[email protected] Sales: +91 96014 44111 Service: +91 96013 33888
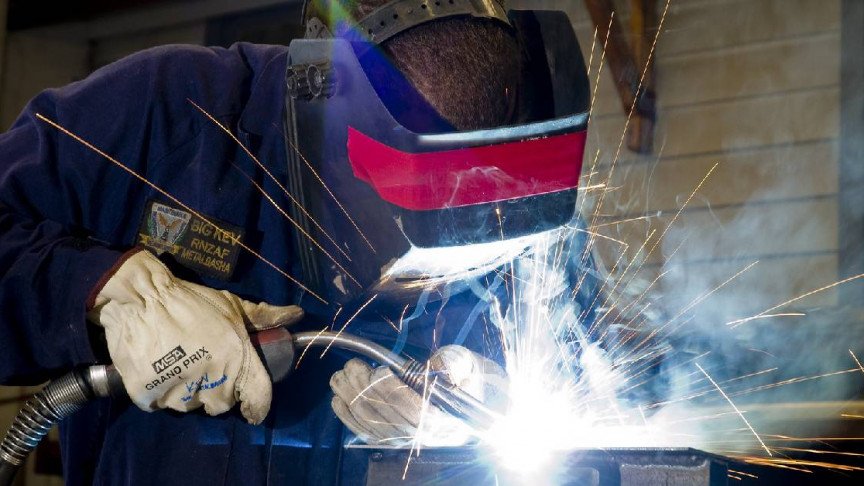
APS industrial tube to tube welding system power source in a heavy engineering facility
ASME & EN ISO Compliant · Made in India for Global Exporters

Tube to Tube Welding System: Industrial Sourcing & Engineering Masterclass

Next-Gen Orbital TIG & Automated Inverter Systems for Zero-Defect Boiler, Heat Exchanger & Process Piping Fabrication.

99.8%
Radiographic NDT Pass Rate
22,600+
Power Sources Field-Deployed
21+
Years R&D & In-House Design
56+
Automated System Configurations
Information Gain & User Intent Mining

Why Modern Procurement Engineers Are Transitioning to Automated Tube to Tube Welding Systems

In high-stakes industrial environments—such as nuclear power plants, supercritical boilers, pharmaceutical ultra-high purity (UHP) fluid lines, and offshore heat exchangers—the humble pipe joint represents either an operational triumph or a catastrophic single-point failure.

Global procurement teams and welding engineering directors frequently face a crucial dilemma: How can we achieve 100% Non-Destructive Testing (NDT) compliance while suppressing operational costs and coping with an acute shortage of certified Class-A manual TIG welders?

Manual GTAW (TIG) root pass welding on thin-wall stainless steel or heavy-wall chrome-moly tubing introduces severe vulnerabilities: tungsten inclusion, root concavity, oxidation (sugar coat), uncontrolled heat-affected zones (HAZ), and inconsistent interpass temperature control. An automated Tube to Tube Welding System eliminates human variable errors by locking arc voltage, pulsing frequency, orbital rotation speed, and inert gas purging within strict digital boundaries.

At Advanced Power Sources Limited (APS Welding), our senior engineering team designs and manufactures complete tube-to-tube and tube-to-tubesheet automated welding systems from the ground up at our ISO 9001:2015 certified plant in Valsad, Gujarat, India. By pairing high-frequency IGBT inverter power sources with microprocessor-driven orbital heads and cold-wire feeders, we provide international buyers with unmatched information transparency, zero-defect repeatabilities, and total operational reliability.

  • Full compliance with ASME Section IX & EN ISO 15614-1 code requirements
  • Elimination of root concavity and inner-diameter oxidation
  • Micro-pulse current shaping for minimal thermal distortion
  • Real-time telemetry logging via proprietary WeldVisor IoT software
  • Up to 4x higher daily joint deposition speed compared to manual GTAW
  • Integrated cold wire feeder options for heavy wall thicknesses
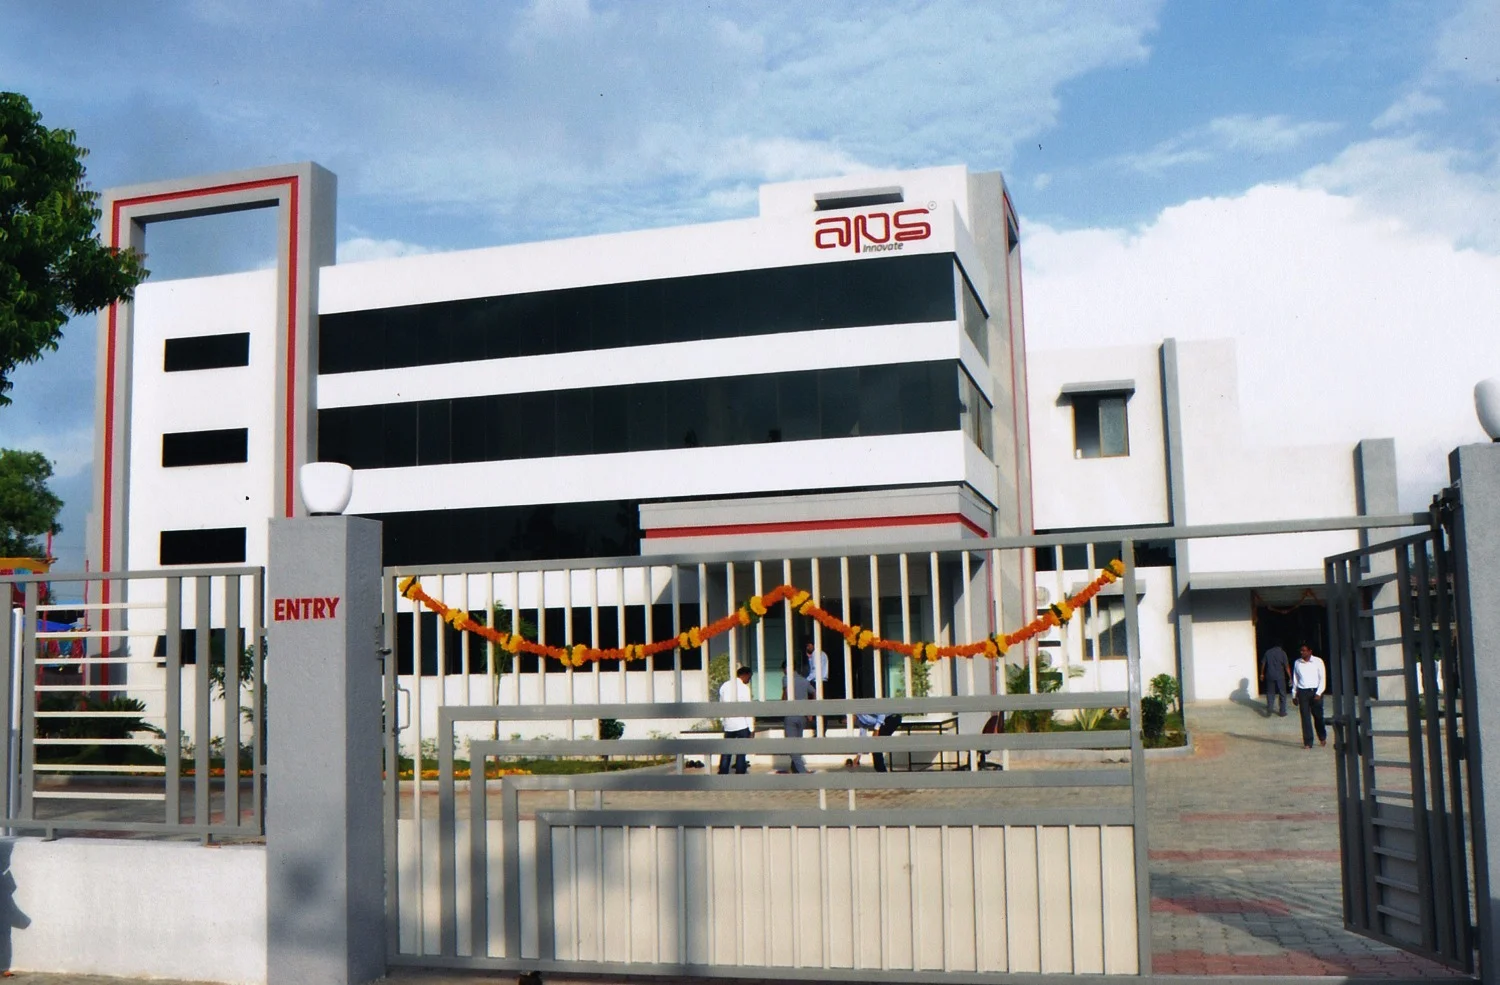
Advanced Power Sources factory facility producing automated tube to tube welding systems
ISO 9001:2015In-House R&D & Assembly
Product Architecture & Recommendations

APS Flagship Tube to Tube Welding System Configurations

Select from our specialized orbital TIG power sources, closed-chamber heads, open-frame rotating heads, and integrated tube-to-tubesheet positioner systems engineered for global duty.

★ Closed Orbital Head
APS Micro-Tube 75

High-Purity Thin-Wall System

Engineered for autogenous (fillerless) orbital TIG welding of stainless steel (304L, 316L) and titanium tubes in cleanroom and biopharma applications.

  • Tube OD Range6.0 mm to 76.2 mm (1/4" to 3")
  • Wall Thickness0.5 mm to 3.0 mm
  • Purge SystemClosed Gas Chamber (<10 ppm O2)
  • Arc ControlDigital Micro-Pulse GTAW
★ Open Frame & Wire Feed
APS Heavy-Pipe 168

Heavy-Wall Tube & Pipe System

Heavy-duty open orbital head equipped with integrated cold wire feeder and Arc Voltage Control (AVC) for multi-pass boiler and process line joints.

  • Tube/Pipe OD25 mm to 168 mm (1" to 6.5")
  • Wall Thickness3.0 mm to 18.0 mm (Multi-pass)
  • Wire FeedingCold Wire Synchronized Pulse
  • TrackingAutomatic Voltage Control (AVC)
★ Inverter Power Source
Apollo Pulse 300 Orbital

Master Orbital Control Power Source

300A 100% duty cycle IGBT inverter power supply featuring multi-axis microprocessor control, job storage memory, and IoT logging.

  • Current Range5A to 300A DC Pulse
  • Duty Cycle100% @ 40°C (IEC 60974-1)
  • Program Memory100 Multi-Sector Jobs
  • IoT TelemetryWeldVisor Cloud Connectivity
★ Tube-to-Tubesheet
APS TubeSheet Station

Exchanger Header Welding Unit

Automated pneumatic clamping head for flush, recessed, or protruding tube-to-tubesheet joint configurations in boiler and condenser fabrication.

  • Tube OD Capacity10 mm to 80 mm ID/OD
  • Pneumatic ClampInternal/External Centering
  • Torch Rotation360° Continuous Motorized
  • ProcessTIG Pulsed / AVC Optional
Engineering Selection Matrix

Tube to Tube Welding System Selection Criteria by Material & Joint Geometry

Use this expert comparison table to specify the correct power source, head type, shielding gas, and wire feed setup based on your exact shop or site requirements.

Application / Metallurgy Tube OD & Wall Range Recommended Head & Process Shielding & Purge Strategy NDT Target Standard APS System Configuration
UHP Stainless Steel (316L VIM/VAR)
Semiconductor & Pharma
OD 6.35 mm – 38.1 mm
Wall 0.89 mm – 1.65 mm
Closed Chamber Orbital Head
Autogenous GTAW (No Filler)
99.999% High-Purity Argon
<5 ppm O2 Backing Purge
AWS D18.1 / ASME BPE
100% Visual & Borescope
APS Micro-Tube 75 + Apollo 300
Supercritical Boiler Tubes
T91, T92, SA213 Carbon Steel
OD 38 mm – 76 mm
Wall 4.0 mm – 10.0 mm
Open Frame Orbital Head
Pulse TIG with Cold Wire Feed
Argon / 2% H2 or Ar/He Mix
Internal Purge Dam System
ASME Section I & VIII Div 1
100% Radiography (RT)
APS Heavy-Pipe 168 + Cold Wire Unit
Shell & Tube Heat Exchangers
Duplex 2205, Inconel 625
OD 15.8 mm – 50.8 mm
Wall 1.5 mm – 3.5 mm
Tube-to-Tubesheet Head
Pulsed GTAW with AVC
98% Ar + 2% N2 for Duplex
Standard Purge Cone
ASME VIII / TEMA Class R
Dye Penetrant & Hydrotest
APS TubeSheet Station + Inverter
Cross-Country Process Lines
Stainless & Titanium Grade 2
OD 50 mm – 219 mm
Wall 2.0 mm – 12.5 mm
Heavy Open Orbital System
Multi-Pass TIG / Arc Oscillation
Pure Argon Shielding
Trailing Shield Cup for Ti
EN ISO 15614-1 / API 1104
Ultrasonic (UT) & RT
APS Open-Frame Heavy Series
Custom Turnkey Engineering Custom OD Specs Available Modular Integration Option Application-Tailored Setup ASME / EN / AWS Code Ready Talk to an APS Application Engineer →

*Note: All APS Tube to Tube Welding Systems are engineered in-house. Custom orbital clamp inserts, arc oscillation units, and high-temperature torch assemblies can be built to project specification.

Procurement & Technical FAQ

Frequently Asked Questions on Tube to Tube Welding Systems

Direct answers to the top engineering, compliance, and purchasing questions asked by global procurement specialists.

What is a Tube to Tube Welding System and why is it superior to manual welding?

A Tube to Tube Welding System is an automated or semi-automated orbital TIG (GTAW) or MIG setup engineered to join metal tubes and pipes with continuous 360-degree mechanical precision. Unlike manual welding, which suffers from operator fatigue, inconsistent heat input, and high reject rates, an automated system delivers repeatable 100% root penetration, smooth internal bead profiles, zero root concavity, and 99.8%+ NDT radiography pass rates under ASME Section IX and EN ISO 15614-1 standards.

Which industries require automated Tube to Tube Welding Systems?

Tube to tube welding systems are essential across high-reliability industries including boiler tube fabrication, shell and tube heat exchangers, pharmaceutical ultra-high purity (UHP) piping, food and dairy tubing, oil & gas subsea risers, nuclear power plant cooling loops, chemical processing, and semiconductor high-purity gas distribution networks.

Can an APS Tube to Tube Welding System weld dissimilar metals or high-alloy materials?

Yes. APS tube to tube welding systems feature programmable micro-pulse digital power sources that accurately regulate heat input. This allows flawless welding of austenitic stainless steels (304L, 316L, 904L), duplex and super duplex stainless steels, titanium Grade 2, Inconel 625/825, Hastelloy, and chrome-moly alloy steels (T91/T92) with minimal heat-affected zone (HAZ) degradation.

What is the difference between closed-chamber and open-frame orbital tube welding heads?

Closed-chamber welding heads completely enclose the tube joint within a flooded inert gas purging chamber. This prevents surface oxidation and enables ultra-clean autogenous (fillerless) TIG welds on thin-wall tubes (OD 6 mm to 76.2 mm). Open-frame heads accommodate larger tube/pipe diameters (up to 219 mm or higher) and heavy wall thicknesses, allowing cold wire feeding, torch oscillation, and Automatic Voltage Control (AVC) for multi-pass joints.

How does APS ensure weld quality traceability for ASME and nuclear code audits?

APS Tube to Tube Welding Systems integrate seamlessly with our proprietary WeldVisor IoT platform and Weld-O-Meter tracking hardware. They record real-time welding current, arc voltage, orbital rotation speed, wire feed rate, and back-purge oxygen levels per sector, outputting encrypted digital weld logs for 100% QA/QC code compliance.

What input power supply is required for international site deployment?

APS welding power sources are built with wide input voltage tolerance (380V to 440V, 3-phase, 50/60 Hz or 220V single-phase depending on unit configuration). Built-in voltage stabilization shields sensitive inverter control electronics against generator voltage spikes and harsh site power fluctuations.

What after-sales support, spare parts, and training does APS offer global buyers?

APS provides end-to-end support including pre-sale application engineering, digital weld procedure specification (WPS) support, live online or factory operator training, rapid-dispatch spare parts packages, and dedicated after-sales engineer assistance from our plant in Valsad, Gujarat, India.

Enterprise Credentials & E-E-A-T

Why Global Fabricators Partner with Advanced Power Sources Limited

When buying specialized Tube to Tube Welding Systems, dealing directly with the original equipment manufacturer ensures technical integrity, long-term spare parts availability, and maximum Return on Investment (ROI).

Founded over two decades ago in Gujarat, India, APS Welding (Advanced Power Sources Limited) operates a fully integrated ISO 9001:2015 certified design, assembly, and testing facility. We don't just assemble purchased components; our electronics engineers design the proprietary IGBT inverter driver cards, digital control firmware, and mechanical orbital head assemblies in-house.

  • 20+ Years of dedicated power source and automation R&D
  • Over 22,600 machines active in heavy fabrication facilities globally
  • 100% load-bank performance and insulation testing before dispatch
  • In-house CNC machining for precision orbital head components
  • Direct factory support without middleman markups
  • Integrated automation ecosystem (Positioners, Rotators, Columns & Booms)
Contact Us
APS engineering team testing in-house designed IGBT inverter control electronics for tube welding machines
22,600+Field-Installed Machines
Technical Knowledge Hub

Related Technical Resources & Equipment Guides

Inverter TIG Welding Machine technology guide

IGBT Inverter TIG Welders

Deep dive into high-frequency arc initiation, pulse shaping, and thermal management in DC GTAW power sources.

Read Tech Guide →
Cold Wire Feeder for TIG Welding System

Cold Wire Feeders for TIG

Discover how synchronized cold wire feeding doubles deposition rates in heavy-wall tube and pipe joints.

Explore Cold Wire Systems →
Industrial Welding Positioners and Automation Systems

Industrial Welding Positioners

Explore 50 kg to 10-ton turntables and tilting positioners for seamless vessel head and flange manipulation.

View Positioner Range →

Request an Engineered Proposal for Your Tube Welding Line

Submit your tube outer diameter, wall thickness, material grade, and production targets. Our application team will respond within 24 hours.

Contact Us