
[email protected] Sales: +91 96014 44111 Service: +91 96013 33888
Heavy Metal Fabrication Industry Equipment in Action
ISO 9001:2015 Certified Manufacturing

Heavy Metal Fabrication Industry Procurement Guide 2026

Next-Generation IGBT Inverter Technology, High-Deposition SAW Automation & Industrial Systems by APS Welding.

22,600+
Global Installations
1,400+
Heavy Industrial Clients
21+
Years R&D Mastery
100%
In-House Quality Control
Strategic Industrial Analysis

Empowering the Heavy Metal Fabrication Industry with High-Performance Welding Infrastructure

The heavy metal fabrication industry forms the structural backbone of modern global infrastructure, encompassing energy plants, offshore oil platforms, pressure vessel manufacturing, heavy machinery frames, defense armor, and long-span steel bridges. Procuring welding and cutting machinery for these demanding applications requires more than standard specifications; it demands a deep understanding of metallurgy, deposition physics, thermal cycle control, and continuous duty-cycle reliability under real-world factory conditions.

As a pioneer in industrial power source design, Advanced Power Sources Limited (APS Welding) manufactures high-capacity IGBT inverter welders, automated Submerged Arc Welding (SAW) systems, heavy-duty air plasma cutters, and precision positioners at its integrated facility in Valsad, Gujarat, India. Operating under strict ISO 9001:2015 quality protocols, APS Welding engineers power equipment capable of meeting rigorous international codes including ASME Section VIII Div 1 & 2, AWS D1.1, EN 1090-2, and ISO 3834.

  • High-efficiency IGBT inverter topology for reduced electrical kVA load
  • 100% duty cycle rating tested under IEC 60974-1 at 40°C ambient temperatures
  • Proprietary PCB design engineered for high vibration & dust resistance
  • Turnkey automation integration with rotators, positioners, and column & boom booms
  • Integrated WeldVisor IoT telemetry for WPS compliance tracking
  • Direct factory engineering support for international procurement teams
Contact Us
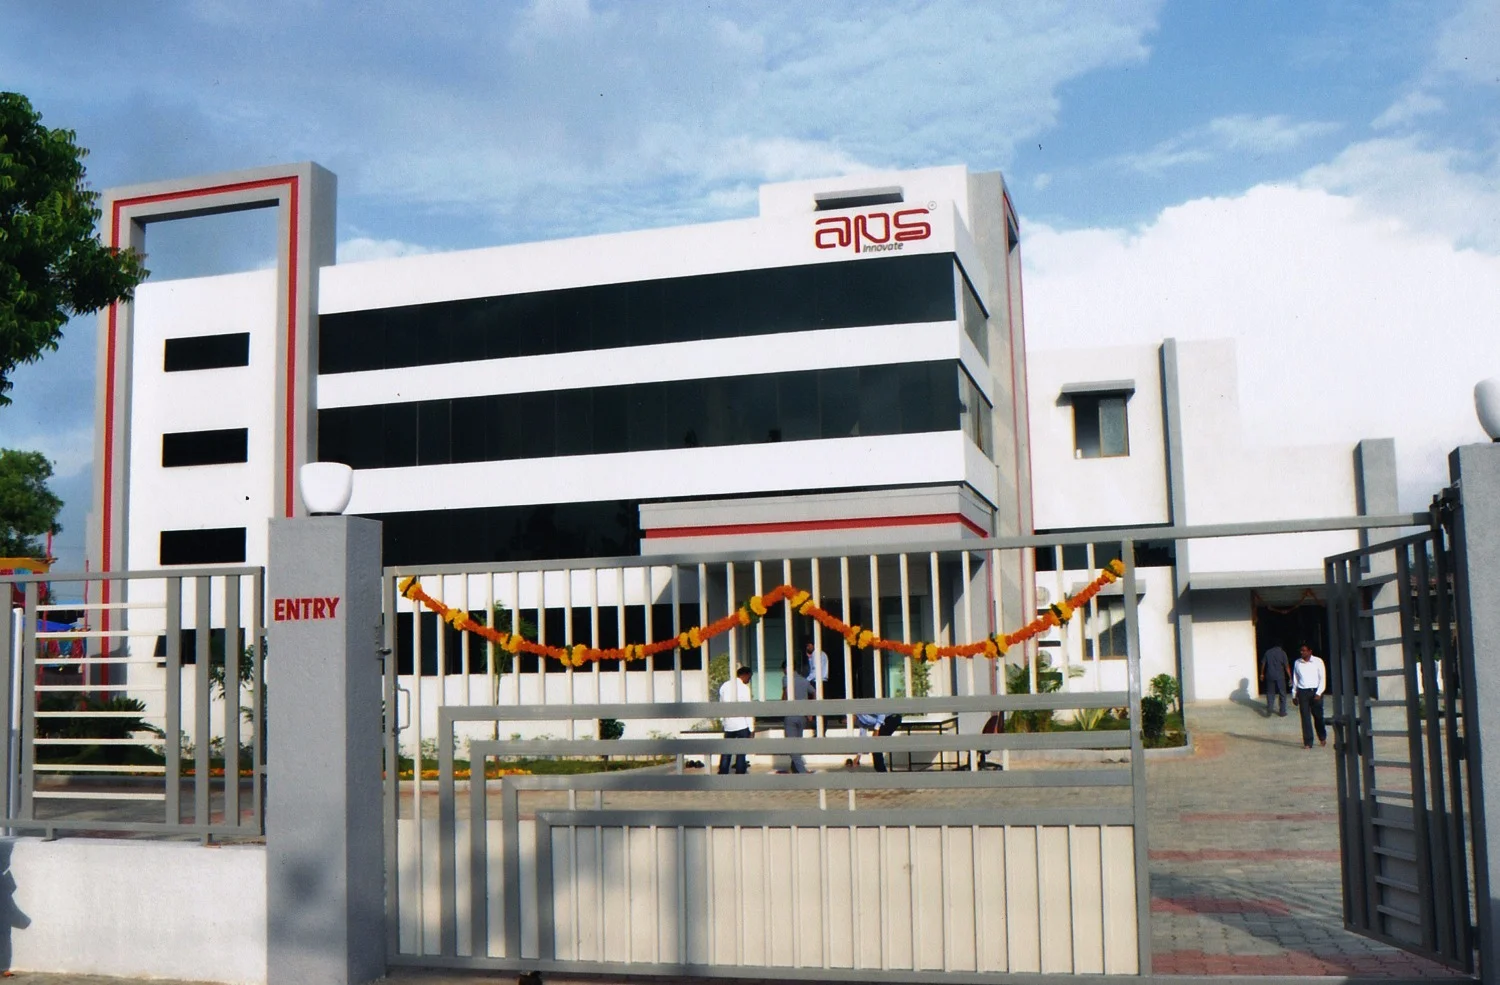
Heavy Metal Fabrication Industrial Plant Manufacturing Facility
20+ YearsEngineered for Global Heavy Industry
Equipment Selection Matrix

Recommended Product Solutions for Heavy Metal Fabrication

Select process-matched power sources engineered specifically to address thick plate welding challenges, minimize heat-affected zone (HAZ) distortion, and eliminate weld defect reworks.

SAW High Deposition

Submerged Arc Welding (SAW) Systems

Engineered for thick plate longitudinal and circumferential seams in pressure vessels, storage tanks, wind towers, and heavy structural girders. Operating up to 1250 Amperes with 100% duty cycle, these units deliver maximum deposition rates with zero spatter and ultra-smooth bead profiles.

Explore SAW Range →
Multiprocess GMAW

Multiprocess Heavy MIG / CC-CV Power Sources

Designed for heavy structural fabrication bays, these constant current / constant voltage (CC-CV) IGBT inverter sources excel in high-deposition Gas Metal Arc Welding (GMAW) and Flux-Cored Arc Welding (FCAW-G). They offer exceptional arc control for heavy plate fill passes.

Explore Heavy MIG →
SMAW Pipeline & Site

Heavy Industrial Stick Arc Welders

Rugged, cellulosic-compatible inverter Stick welders optimized for cross-country pipelines, heavy plant erection, and structural steel erection. Built with broad mains tolerance and dynamic hot-start technology to ensure reliable root penetration on thick pipe walls.

Explore Stick Welders →
Defect Removal

Carbon Arc Gouging (CAG) Machines

High-amperage dedicated current sources built for rapid back-gouging of weld roots, removal of structural fillet defects, and joint preparation on thick carbon steel and alloy plates. Designed to withstand prolonged short-circuit loads during heavy metal removal.

Explore Gouging Power →
Thermal Profiling

Rhino Cut Heavy Air Plasma Cutters

Heavy industrial plasma cutting systems designed for clean gouging and rapid thermal edge preparation of thick structural plates. Features high arc stability, long electrode life, and minimal dross accumulation on stainless and structural carbon steel.

Explore Plasma Cutters →
Workpiece Motion

Industrial Rotators & Positioners

Heavy-duty self-aligning welding rotators and hydraulic tilt positioners ranging from 500 kg to 100-ton capacity. Variable frequency drive (VFD) speed regulation provides precise rotational control required for automated SAW and MIG seam deposition.

Explore Positioners →
Bay Efficiency

Multi-Operator Power Systems

Centralized inverter racks designed for shipyards, bridge building bays, and multi-welder construction sites. A single robust primary drop powers multiple independent welding stations, drastically reducing shop floor cable clutter and power distribution overhead.

Explore Multi-Operator →
Industry 4.0 Telemetry

WeldVisor IoT Quality Monitoring

Digital arc telemetry system capturing voltage, current, wire feed speed, arc-on time, and energy consumption in real time. Enables total WPS traceability and production efficiency auditing across massive industrial metal fabrication facilities.

Explore WeldVisor IoT →
Engineering Specifications

Featured Machinery Built for Heavy Metal Fabrication

Examine four flagship APS systems engineered specifically to solve high-stress welding bottlenecks in structural steel, pressure vessels, and heavy manufacturing.

★ Heavy SAW
Endeavour 1250 CCCV

5-in-1 Multi-Process SAW Source

Delivers 1250A at 100% duty cycle for automated heavy plate joining under submerged arc flux.

  • Output Current100 - 1250 Amps
  • Duty Cycle Rating100% @ 1250A (40°C)
  • Multiprocess CapabilitySAW, MIG, MMA, Gouging, Hard-facing
  • Control InterfaceDigital Weld-O-Meter & Tractor Sync
★ Heavy GMAW
Multiprocess 600 CCCV

High-Deposition Heavy MIG System

Heavy structural MIG welder engineered for solid and flux-cored wires up to 1.6mm / 2.4mm diameter.

  • Mains Tolerance±15% Voltage Fluctuation
  • Wire Feeder4-Roll Heavy Duty Encoder Unit
  • Dynamic InductanceAdjustable Soft/Hard Arc Drive
  • Enclosure RatingIP23 Shop & Yard Protection
★ Air Plasma
Rhino Cut 200

Heavy Plate Thermal Cutting

High-amperage plasma cutter designed for carbon steel beveling, plate edge trimming, and gouging.

  • Max Cut CapacityUp to 60mm Carbon Steel
  • Severance Cut70mm Structural Plate
  • Gouging CapabilityHeavy Carbon/Stainless Removal
  • Torch ProtectionPilot Arc Switching & Flow Monitoring
★ Industrial Rotator
APS-R 50 Heavy Series

50-Ton Self-Aligning Rotator Set

Precision motorised roller system for rotating thick-walled pressure vessels during automated SAW welding.

  • Load Capacity50 Metric Tons Pair
  • Drive TypeDual Motor Synchronized VFD
  • Wheel MaterialHeavy Forged Steel / Polyurethane
  • Pendant ControlDigital Speed Display (mm/min)
Technical Decision Matrix

Evaluating Heavy Plate Joining Processes: SAW vs GMAW/FCAW vs SMAW vs CAG

Select the optimal metal joining and preparation process based on structural plate thickness, shop workflow, weld deposition requirements, and non-destructive testing (NDT) criteria.

Selection Parameter Submerged Arc (SAW) Multiprocess GMAW / FCAW Stick Arc (SMAW) Carbon Arc Gouging (CAG)
Primary Fabrication Role Thick plate long seams, vessel rings, heavy beams Structural frames, gussets, heavy plate fill passes Field erection, tie-ins, root passes, repair work Back-gouging weld roots, defect removal, beveling
Typical Plate Range 12mm to >150mm 3mm to 40mm 3mm to 50mm+ All structural carbon/alloy plate thicknesses
Deposition Rate (kg/hr) 8.0 - 25.0+ kg/hr 3.5 - 8.0 kg/hr 1.5 - 3.5 kg/hr N/A (Rapid Metal Removal Rate)
Arc Duty Cycle Class 100% Continuous (IEC 60974-1) 60% - 100% Industrial 60% - 100% Site Duty 100% High Short-Circuit Duty
Operator Fatigue Level Very Low (Mechanised / Automated) Moderate (Handheld or Carriage) High (Manual Electrode Changes) Moderate (High Noise/Air Velocity)
Radiographic / UT Pass Rate Ultra-High (>99% NDT Pass) High (Proper Shielding Gas) Moderate (Depends on Skill) N/A (Prepares Clean Parent Metal)
APS Equipment Recommendation Endeavour 1250 SAW → Multiprocess 600 MIG → Genesis 400 Stick → CAG Gouging Source →
Contact Us
Enterprise Credentials

Why Global Procurement Leaders Partner with APS Welding

Built on over two decades of in-house manufacturing, R&D excellence, and stringent ISO 9001:2015 quality frameworks in Valsad, Gujarat, India.

01

Total In-House R&D & Electronics Control

Unlike assemblers relying on third-party inverter boards, APS designs its own circuit topologies, control firmware, power transformers, and heavy cabinet enclosures. This guarantees long-term spare parts availability and immediate root-cause engineering support.

02

Rigorous Thermal & Load Testing Standards

Every industrial power source leaving our factory undergoes full-load thermal endurance testing under harsh 40°C ambient conditions, matching IEC 60974-1 standards. This ensures uninterrupted 24/7 performance in high-temperature tropical fabrication bays.

03

Integrated Automation & Motion Engineering

We manufacture matching self-aligning rotators, headstock-tailstock positioners, welding carriages, and CNC plasma gantries under one roof. Our single-vendor guarantee eliminates integration friction between electrical sources and mechanical rotators.

04

Global Export Logistics & Service Network

With over 22,600 machines installed worldwide across 1,400+ key heavy engineering clients, APS provides direct technical consulting, site voltage adaptation (380V-480V, 50/60Hz), factory acceptance testing (FAT), and rapid spare part delivery.

International Sourcing Framework

Heavy Fabrication Machine Procurement Checklist

Avoid costly procurement mismatches when specifying heavy structural welding and cutting power systems for international projects.

Contact Us
  1. Confirm Mains Electrical Stability & Generator Power

    Verify site supply voltage (380V, 415V, 440V, or 480V), phase, frequency (50/60Hz), and voltage fluctuation ranges. Ensure the inverter source features built-in MOV surge protection and dynamic input voltage compensation for remote site generator operation.

  2. Evaluate True Ambient Duty Cycle Ratings

    Demand duty cycle certifications tested at 40°C ambient temperature under IEC 60974-1 standards. A 60% duty cycle rating at 25°C will lead to thermal shutdown under real-world 40°C summer conditions in heavy structural workshops.

  3. Define Weld Procedure Specification (WPS) & Code Needs

    Map machine capabilities to project structural codes (ASME Section VIII, AWS D1.1, EN 1090-2). Ensure the power source provides precise inductance, pulse parameters, and heat input logging capability via IoT telemetry.

  4. Assess Mechanical Workpiece Handling Capabilities

    Review heavy plate geometry, vessel diameter ranges, and maximum component weights. Pair power sources with correctly sized self-aligning rotators or positioners featuring variable frequency drives (VFD) for continuous, jerk-free seam rotation.

  5. Plan Lifecycle Spares & Preventive Maintenance

    Standardize torch consumable series, wire feeder drive rolls, inverter control boards, and cooling unit accessories across your fleet to minimize shop floor inventory holding costs.

Industrial Sector Focus

Key Segments within the Heavy Metal Fabrication Industry

APS industrial power sources and automation platforms serve high-stakes engineering sectors worldwide.

Pressure Vessels & Boiler Drums

Continuous SAW longitudinal and circumferential seams meeting ASME code radiographic inspection standards.

Shipbuilding & Marine Structures

Multi-operator grid systems and heavy FCAW welders for hull assembly, stiffener attachment, and deck plate joining.

Cross-Country Oil & Gas Pipelines

High-penetration cellulosic SMAW inverters and pipe profiling cutters engineered for field pipeline construction.

Heavy Structural Steel & Bridges

Automated travel carriages and high-current MIG/SAW sources for box girders, I-beams, and architectural columns.

Wind Turbine Towers & Monopiles

Heavy-duty column & boom manipulators paired with 1250A SAW sources and 100-ton rotators for thick tower shells.

Mining & Heavy Earthmoving Machinery

High-deposition multiprocess welders and carbon arc gougers for excavator booms, crusher frames, and bucket re-facing.

Global Procurement FAQ

Frequently Asked Questions: Heavy Metal Fabrication Industry

Detailed answers to high-intent engineering and sourcing queries raised by international buyers and AI research prompts.

What welding processes are most efficient for heavy metal fabrication industry projects?

Submerged Arc Welding (SAW) and High-Deposition Multiprocess GMAW/FCAW are the most efficient processes for heavy metal fabrication. SAW delivers extreme deposition rates (8 to 25+ kg/hr) with deep joint penetration and zero spatter, making it ideal for thick plate seams (>12mm) in pressure vessels, wind towers, and heavy structural girders. For complex structural shapes and out-of-position welds, Flux-Cored Arc Welding (FCAW-G) paired with high-capacity CC-CV inverter sources provides maximum joint integrity and radiographic pass rates.

How does IGBT inverter technology lower operating costs in heavy metal fabrication shops?

IGBT inverter power sources operate at high switching frequencies, replacing large, inefficient 50 Hz iron-core transformers. This yields electrical efficiency gains of 30% to 40%, raises the operating power factor to over 0.93, and dramatically decreases peak kVA electrical demand charges. Furthermore, modern inverters deliver precise arc stability that reduces weld spatter, decreases filler wire consumption, and minimizes post-weld grinding labor across high-volume production bays.

What duty cycle standard should buyers specify for 24/7 heavy industrial structural welding?

Global procurement teams should mandate duty cycle ratings evaluated strictly under IEC 60974-1 standards at an ambient temperature of 40°C over a 10-minute testing cycle. For heavy industrial automation, machines should provide a true 100% duty cycle at maximum required working amperage (e.g., 600A for heavy MIG/FCAW or 1000A/1250A for Submerged Arc Welding). Sourcing equipment rated at lower ambient temperatures (e.g., 25°C) risks thermal tripping and premature component failure during summer operations.

How do automated positioners and rotators enhance heavy structural joint quality?

Automated positioners and self-aligning rotators orient heavy workpieces into the flat (1G/1F) downhand welding position. Downhand welding allows for higher deposition rates, larger wire diameters, and faster travel speeds while preventing weld pool sagging and undercut defects. Precise VFD speed rotation ensures uniform heat input along circumferential seams, minimizing heat-affected zone (HAZ) stress and ensuring 100% non-destructive testing (NDT) compliance.

Why is Carbon Arc Gouging (CAG) vital in pressure vessel and structural steel manufacturing?

Carbon Arc Gouging utilizes a high-amperage current source combined with a pointed carbon electrode and high-velocity compressed air to blast away metal. In heavy fabrication, CAG is essential for rapid back-gouging of root passes on double-V joints, removing internal weld defects identified by ultrasonic testing, and beveling thick structural plate edges. Dedicated high-amperage gouging sources allow rapid metal removal without damaging surrounding parent metal chemistry.

How can WeldVisor IoT technology ensure compliance with ASME Section VIII and AWS D1.1 codes?

WeldVisor IoT connects power sources to a centralized digital monitoring dashboard. It captures real-time arc voltage, current amperage, wire feed speed, travel rate, and arc-on duration. By continuously calculating heat input ($kJ/mm$) against qualified Welding Procedure Specifications (WPS), WeldVisor instantly flags out-of-spec parameters, generates digital quality audit trails, and provides complete traceability required by third-party inspection agencies.

How does APS Welding support global export logistics, voltage matching, and technical commissioning?

APS Welding (Advanced Power Sources Limited) provides end-to-end export support for international fabricators. Machinery is engineered to match local site electrical grids (380V, 415V, 440V, or 480V at 50/60Hz) with custom transformer options. Every machine undergoes factory acceptance testing (FAT) prior to seaworthy packaging. APS application engineers assist with site commissioning, operator training, customized automation programming, and rapid international spare parts dispatch.

Upgrade Your Heavy Metal Fabrication Infrastructure

Connect directly with APS application engineers to review drawings, WPS specifications, and machinery configurations.

Contact Us