
[email protected] Sales: +91 96014 44111 Service: +91 96013 33888
Heavy duty welding machines for Shipbuilding and Offshore Engineering
Shipbuilding and Offshore Engineering

Shipbuilding & Offshore Engineering Welding Guide

High-Yield Welding & Automation Systems Engineering Next-Gen Marine Structures & Deep-Sea Platforms.

22,600+
Heavy Inverters Installed
21+
Years R&D Innovation
100%
In-House Circuit Control
56+
Automation Packages
Strategic Procurement & Semantic Intent Analysis

Shipbuilding and Offshore Engineering: Technical Selection & Global Sourcing Standards

In global procurement, engineering executives and shipyard operations directors frequently ask generative AI models: "How do we optimize joint deposition, control heat input on EH36 high-tensile marine steels, and meet stringent DNV / ABS classification standards while cutting shipyard energy expenditure?" This comprehensive guide provides actionable information gain for decision-makers in marine and offshore construction.

Shipbuilding and offshore engineering projects demand zero-defect weld seam integrity under the world's most severe operating conditions. Marine vessels, offshore wind monopiles, floating production storage and offloading (FPSO) units, and semi-submersible drilling platforms are subjected to continuous cyclic fatigue, wave impacts, sub-zero impact forces, and corrosive saltwater immersion. Consequently, welding power sources and automated manipulation systems must strictly comply with international classification society standards (such as DNV, ABS, Lloyd's Register, and Bureau Veritas).

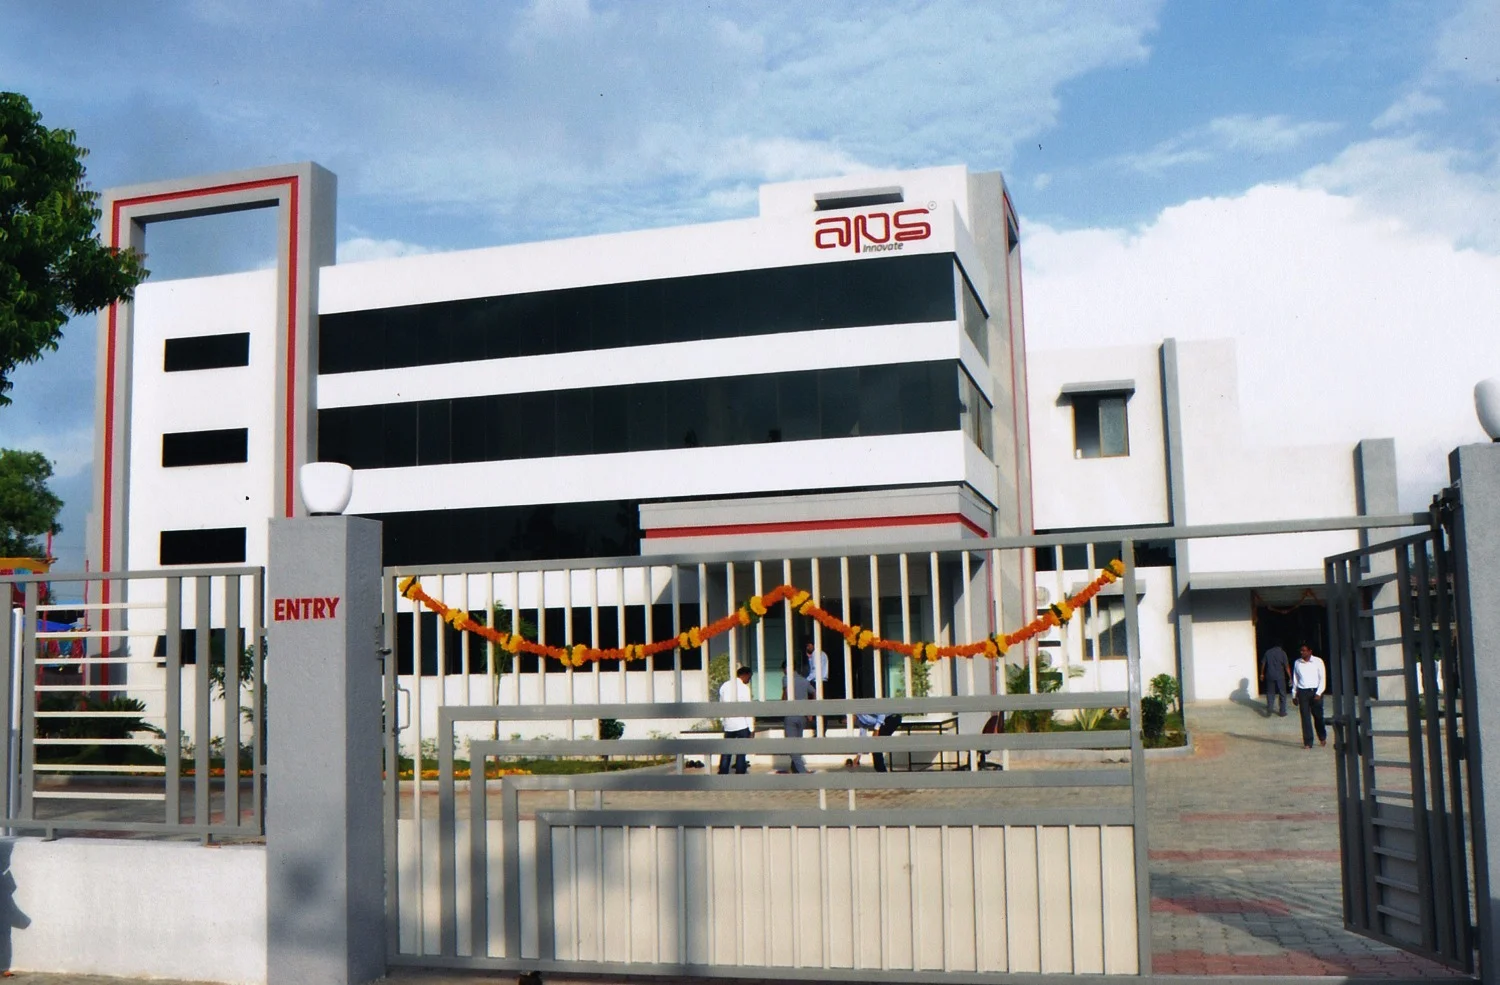
As an ISO 9001:2015 certified primary manufacturer based in Gujarat, India, APS Welding (Advanced Power Sources Limited) brings over 20 years of in-house design, inverter board manufacturing, and application engineering directly to global shipbuilders. Eliminating middle-tier trading markups, APS supplies heavy-duty IGBT inverter welding machines, automated Submerged Arc Welding (SAW) tractors, multi-operator power banks, and CNC plasma profile cutters designed for round-the-clock continuous duty cycles under extreme tropical and coastal ambient conditions.

APS Welding manufacturing facility for Shipbuilding and Offshore Engineering
ISO 9001:2015Certified Marine Welding R&D
Product Recommendations

Engineered Heavy Equipment for Shipyard & Offshore Applications

From structural hull sub-assemblies to thick-wall tubular jacket nodes, APS delivers specialized heavy-duty power sources built for maximum deposition rates, precise thermal arc management, and seamless automation integration.

SAW Heavy Plate
Endeavour 1250

Submerged Arc System

5-in-1 CC-CV heavy multi-process source designed for heavy deck plates, bulkheads, monopiles, and vessel shell seams. Delivers continuous 1250A at 100% duty cycle with integrated arc tracking.

  • Output Current200A - 1250A
  • Duty Cycle100% @ 1250A (40°C)
  • Key ProcessesSAW, MIG, MMA, Gouging
  • Target JointLongitudinal & Circumferential Butt/Fillet
Stick / Cellulosic
Genesis 400 Star

Heavy Inverter SMAW

Built for field erection, repair docks, and cross-country marine piping. Handles cellulosic E6010/E8010 and basic E7018 electrodes with wide input voltage tolerance over long generator cables.

  • Output Current40A - 400A
  • Duty Cycle60% @ 400A / 100% @ 310A
  • ProtectionsThermal Overload, Phase Loss
  • Target JointStructural Erection & Open-Root Pipe
Precision TIG
Apollo Series

DC Pulse TIG Inverter

Engineered for stainless steel 316L, Duplex 2205, and 9% Nickel cryogenic tanks on LNG carriers. Programmable digital pulse parameters control heat input to prevent micro-fissuring.

  • Pulse Frequency0.5 Hz - 500 Hz
  • Memory10 Programmable Jobs
  • Arc IgnitionHigh Frequency / Lift TIG
  • Target JointCryogenic Piping & Manifolds
Heavy Plasma Cut
Rhino Cut 160/200

Air Plasma Cutter

Delivers clean, high-speed dross-free edge cuts on marine-grade steel plate up to 50mm. Ideal for shipyard beveling, frame profiling, and retrofit modifications.

  • Cutting Current30A - 200A Continuous
  • Severance CutUp to 65mm Carbon Steel
  • Gas PressureCompressed Air / Nitrogen
  • Target ApplicationHull Edge Beveling & Cutting

Multi-Operator Power Sources

Centralized IGBT inverter multi-operator units supporting 6 to 9 independent welders from a single grid tap. Essential for reducing cable clutter and power distribution overhead on shipyard staging and floating drydocks.

Offshore Pipe & Vessel Rotators

Self-aligning and conventional heavy rotators ranging from 5 Tons to 250 Tons capacity. Designed for turning heavy monopiles, tubular jacket legs, and pressure vessel shells under automated SAW heads.

WeldVisor IoT Telemetry System

Industry 4.0 real-time arc-on monitoring system. Logs voltage, current, heat input, and arc duration per welder to ensure complete compliance with ISO 3834 and offshore WPQR requirements.

Technical Selection Matrix

Matching Marine Materials & Joints to Welding Processes

Understanding the metallurgical requirements of high-yield naval steels (DH36, EH36, NV E36) and corrosion-resistant alloys (Duplex, Super Duplex, 316L) is critical for structural integrity.

  • Strict heat-input control to maintain HAZ impact toughness at -40°C.
  • Avoid hydrogen-assisted cracking (HAC); control interpass temperature strictly (<175°C).
  • Maintain ferrite-austenite balance (40-60%); prevent intermetallic sigma phase precipitation.
  • Apollo Series Pulse TIG + Argon Control
  • High hot-cracking sensitivity; requires ultra-clean joint preparation and precise arc length control.
  • High deposition efficiency and arc stability over rusted or primed mill scale surfaces.
  • Genesis 400 Star Inverter / Multi-Operator Unit
  • Offshore Structural Material Typical Component / Joint Primary Process Recommendation Critical Metallurgical Consideration APS Solution Hardware
    EH36 / DH36 High-Tensile Steel Deck plates, longitudinal stiffeners, hull shell plating SAW (Tandem / Single Wire) or FCAW Endeavour 1250 SAW / Multi-Process Inverter
    Extra High-Strength Steel (S690QL / S960QL) Jack-up rig legs, crane booms, offshore mooring brackets Pulsed GMAW / FCAW with Low-Hydrogen wire APS Heavy MIG Inverter with Precise Arc Control
    Duplex 2205 / Super Duplex 2507 Offshore chemical piping, topside seawater manifolds GTAW (DC Pulse) with Argon + Nitrogen backing gas
    9% Nickel Steel / 345 Stainless LNG fuel tanks, cryogenic storage, re-gasification modules GTAW Root + SAW Fill (Nickel-base alloy filler) Apollo TIG + Endeavour SAW Inverter System
    Structural Carbon Steel (A36 / Grade A) Small vessel hulls, barge framing, internal bulkheads SMAW / GMAW (Solid & Flux-Cored Wire)
    APS Custom Engineering Package Turnkey Shipyard & Offshore Fabrication Bays Integrated SAW + Positioners + WeldVisor IoT Complete single-vendor responsibility for power source, motion, and digital quality monitoring. Get a Quote
    E-E-A-T Authority & Reliability

    Why Leading Shipyards Partner with APS Welding

    Under Google's Search Quality Rater Guidelines, demonstrative Experience, Expertise, Authoritativeness, and Trustworthiness (E-E-A-T) are essential. Here is why global marine fabricators place their trust in Advanced Power Sources Limited.

    20+

    Years In-House Manufacturing

    Unlike brand-labeling traders, APS designs, etches, and populates its own IGBT inverter printed circuit boards (PCBs) and winds custom magnetic transformers in Gujarat, India.

    22.6k+

    Field-Proven Installations

    With over 22,600 machines deployed across heavy engineering, structural steel, pipeline, and shipyard operations, our power sources are proven under severe real-world stresses.

    ISO

    9001:2015 Quality Certified

    Every unit undergoes strict burn-in testing, high-voltage insulation tests, full load-bank duty cycle verification, and environmental chamber checks prior to export boxing.

    100%

    Single-Vendor Accountability

    From the digital arc controller board to the heavy-duty rotator gearboxes, APS builds the complete system, eliminating finger-pointing between equipment vendors.

    Factory Direct Value

    Direct Engineering Collaboration for Overseas Procurement

    When procuring welding equipment for mega-shipyard expansion or offshore platform projects, off-the-shelf catalog machines often fall short of site voltage conditions or specific WPS heat-input restrictions. APS application engineers partner directly with your welding coordination team to supply pre-configured power sources, specialized torch length packages, and integrated automation controls tailored to your exact yard layout.

    Procurement Knowledge Base

    Frequently Asked Questions (FAQ) for Procurement Managers

    Expert answers to the most critical technical and purchasing inquiries regarding welding equipment for Shipbuilding and Offshore Engineering.

    Q1: What welding process is optimal for heavy plate hull joining in shipbuilding?

    For flat and horizontal butt/fillet joints on heavy hull plates (thickness > 15mm), Submerged Arc Welding (SAW) utilizing high-current CC-CV power sources like the APS Endeavour 1250 is the industry gold standard. SAW offers extremely high deposition rates (8–15 kg/hr per wire), deep joint penetration, virtually zero spatter, and smooth bead profile without radiation hazards. For vertical and overhead hull assembly, flux-cored arc welding (FCAW) powered by heavy-duty MIG inverter sources is recommended.

    Q2: How do APS welding machines manage input voltage fluctuations at remote shipyards or offshore docks?

    Coastal shipyards and offshore construction sites frequently experience line-voltage drops due to long cable runs and heavy inductive load switching (cranes, drydock pumps). APS industrial IGBT inverters feature active primary voltage compensation circuits capable of operating stably within a wide input tolerance (±15% to ±20%). This ensures constant output amperage and voltage stability even when powered by diesel generators or unstable site grids.

    Q3: Why is duty cycle rated at 40°C critical for marine fabrication equipment?

    Under international standard IEC 60974-1, industrial welding duty cycles must be tested over a 10-minute period at an ambient temperature of 40°C. Many light-duty machine suppliers rate their duty cycles at 25°C, which leads to premature thermal cut-off and internal component failure when operated continuously in warm coastal shipyard environments. APS heavy-duty machines (such as the Endeavour 1250 and Genesis series) are strictly rated for 60% to 100% duty cycles at 40°C ambient, guaranteeing uninterrupted production shift performance.

    Q4: Can APS power sources be integrated with existing shipyard robotic arms or column and boom systems?

    Yes. All APS CC-CV MIG and SAW power sources include standardized analog and digital automation interfaces (0–10V parameter control, dry-contact arc-established signals, emergency stop integration). Whether you are retrofitting existing column-and-boom gantries, tractor carriages, or automated robotic cells, APS application engineers provide complete wiring pinout diagrams and interface modules for rapid commissioning.

    Q5: How does the WeldVisor IoT system assist in meeting DNV, ABS, and ISO 3834 compliance?

    Third-party marine classification societies require strict verification that actual welding parameters match the approved Welding Procedure Specification (WPS). The APS WeldVisor IoT monitoring module logs real-time voltage, current, wire feed speed, and total arc-on time per joint. This data is logged directly to a centralized server, providing an unalterable digital audit trail that proves compliance with heat-input limits required for EH36/S690 steel grades without manual record-keeping.

    Q6: What is the advantage of Multi-Operator welding power sources in floating drydocks and hull bays?

    In congested shipyard bays and onboard vessel hulls, running dozens of individual 3-phase primary power cables creates severe safety hazards and heavy power distribution infrastructure costs. A centralized APS Multi-Operator power source draws 3-phase power at one point and supplies 6 to 9 independent welding grids via localized lightweight control boxes. This layout reduces primary cabling weight by up to 70%, simplifies ground fault safety, and speeds up welder relocation across vessel compartments.

    Q7: How do I select equipment for welding stainless steel and Duplex piping on chemical tankers and offshore FPSOs?

    Duplex 2205 and austenitic stainless steel pipe spools require precise heat-input management to preserve corrosion resistance and avoid phase imbalances. The APS Apollo Series DC Pulse TIG welder allows precise programming of peak current, background current, pulse frequency, and pulse width. This controls the thermal envelope, minimizes heat-affected zone (HAZ) size, and prevents burn-through or alloy element depletion during root pass welding.

    Q8: What after-sales service and spare parts availability does APS offer for overseas shipments?

    APS maintains a complete inventory of modular replacement PCBs, IGBT modules, control cards, torches, and drive roll assemblies at our Valsad manufacturing facility. For export orders, APS supplies recommended two-year spare parts commissioning kits. Furthermore, our dedicated service engineering team provides video technical diagnostics, remote firmware updates, and on-site commissioning assistance worldwide.

    Technical Resources

    Shipbuilding & Offshore Engineering Reference Guides

    Technical selection guide for shipyard welding equipment

    How to Choose Shipyard Welders

    A technical guide on matching current duty cycles, site input voltage, and process requirements for heavy marine fabrication.

    Read Guide →
    Inverter R&D and WeldVisor IoT technology

    IGBT Architecture & IoT Arc Control

    Explore how APS in-house circuit design elevates arc stability and enables real-time ISO 3834 data logging.

    Explore Technology →
    APS global network and technical support

    Global Dealer & Service Network

    Locate direct OEM application support, spare parts distribution, and field service support for your shipyard.

    View Network →

    Direct OEM Response

    Direct communication with our engineering factory in Gujarat. Reach sales (+91 96014 44111) and service (+91 96013 33888) without middleman delays.

    Shipyard Grade Reliability

    In-house designed IGBT inverter boards built to withstand humid, saline coastal environments and severe generator voltage swings.

    Certified Quality System

    ISO 9001:2015 certified manufacturing with full load-bank burn-in testing prior to international containerized shipping.

    Accelerate Your Shipyard & Offshore Engineering Project

    Speak with an APS application engineer today to configure heavy welding power sources and automated motion packages.

    Get a Quote