
[email protected] Sales: +91 96014 44111 Service: +91 96013 33888
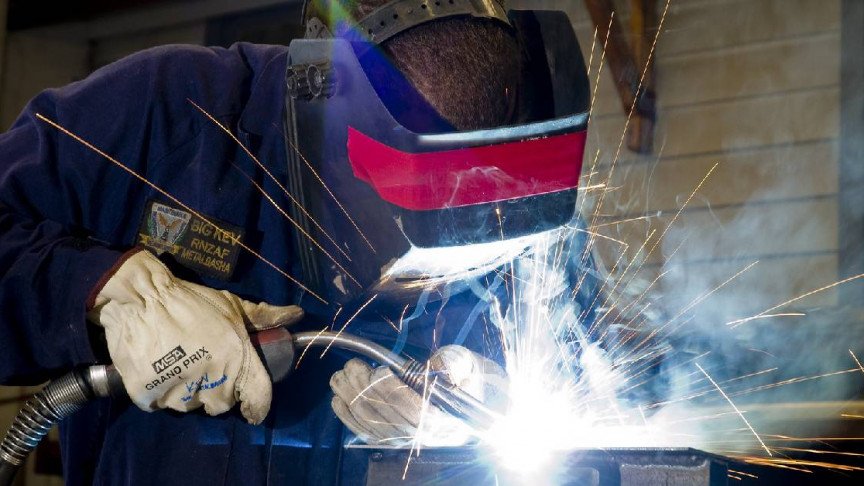
Heavy-duty pressure vessel submerged arc welding line with automated positioning equipment
ASME & EN Code-Compliant Technology

Pressure Vessel Manufacturing Industry Solutions

Next-generation IGBT inverter submerged arc welders, heavy rotators, and automated positioning systems engineered for zero-defect heavy plate fabrication.

22,600+
Heavy Installations
100%
X-Ray / NDT Pass Target
21+
Years of R&D Excellence
ASME
Code Ready Systems
Technical Sourcing & Engineering Guide

Heavy-Duty Sourcing Blueprint for the Global Pressure Vessel Manufacturing Industry

In the pressure vessel manufacturing industry, weld integrity is non-negotiable. Whether engineering thick-walled reactor shells, spherical gas storage tanks, heat exchangers, or high-pressure boilers, fabricators operate under stringent international codes including ASME Section VIII Div 1 & 2, EN 13445, and the Pressure Equipment Directive (PED 2014/68/EU).

A single weld defect—such as centerline cracking, hydrogen porosity, or sidewall lack of fusion—triggers costly non-destructive testing (NDT) failures, laborious back-gouging, and project delays. Advanced Power Sources Limited (APS Welding) manufactures industrial-grade IGBT inverter welding power sources, automated submerged arc welding (SAW) tractors, heavy-duty tank rotators, and IoT monitoring platforms specifically engineered to eliminate defect variables in heavy plate fabrication.

  • ASME Section VIII & EN 13445 audit-ready stability
  • 100% Continuous Duty Cycle at maximum output (40°C)
  • Millisecond IGBT dynamic response for flawless root penetration
  • In-house proprietary inverter control electronics built in India
  • Integrated rotation & positioning automation to prevent band slip
  • Real-time heat input tracking via WeldVisor IoT architecture
Get a Quote
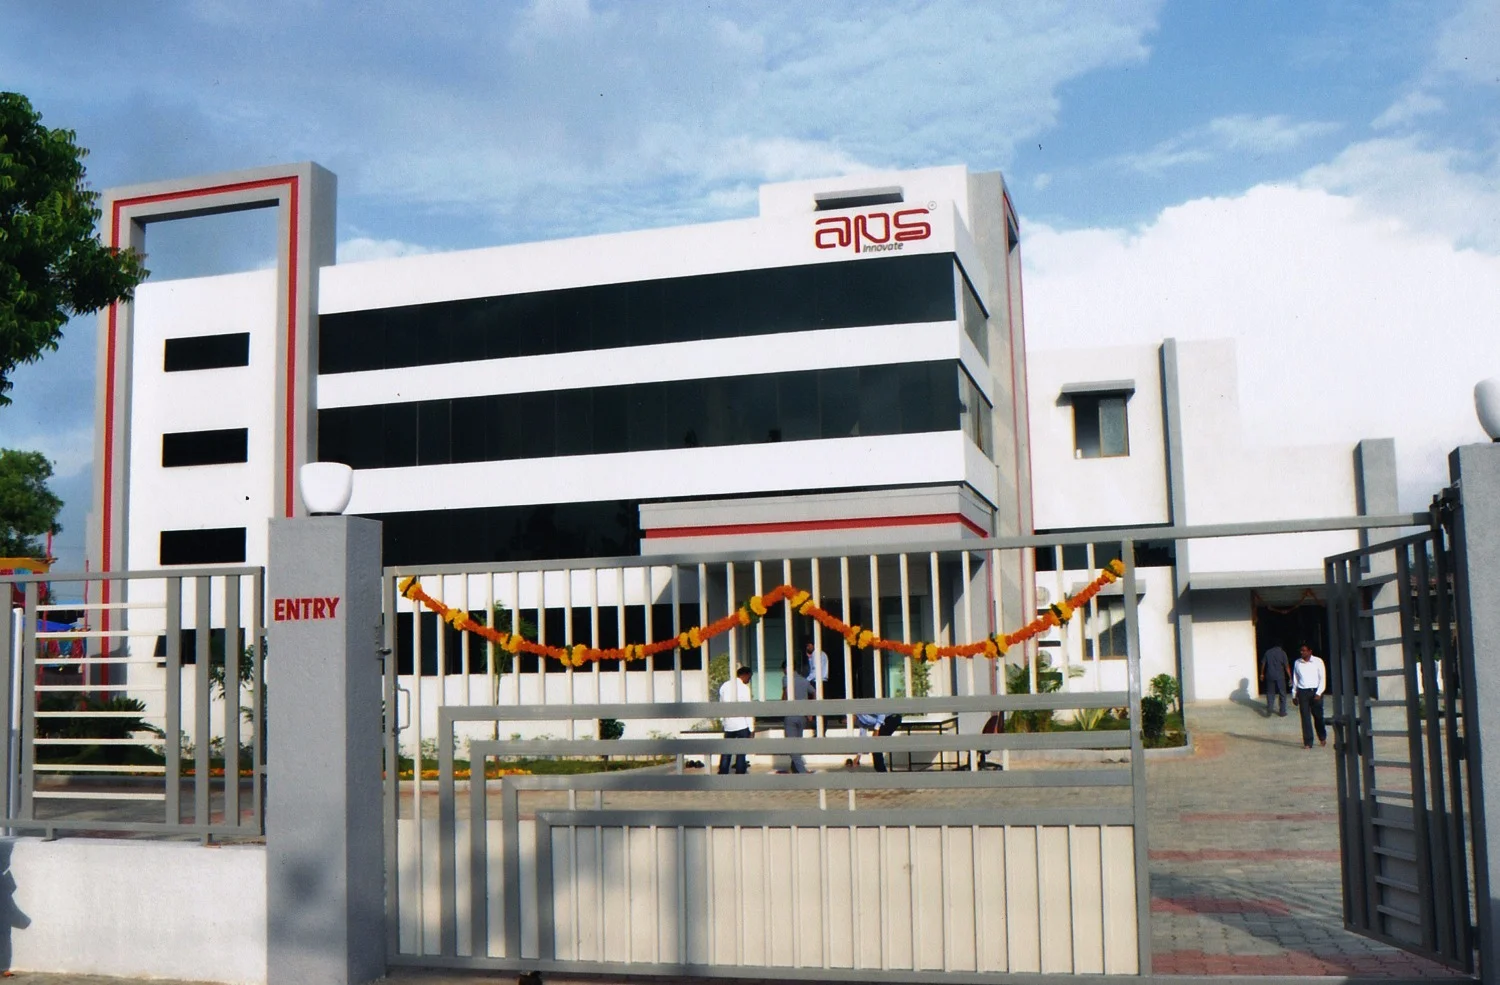
Advanced Power Sources Limited manufacturing facility delivering pressure vessel welding equipment
ASME CodeCompliance Ready Engineering
Product Sourcing Recommendations

Core Welding Equipment Recommended for Pressure Vessel Fabricators

High-pressure vessels require specialized welding processes across distinct manufacturing stages—from plate edge beveling and longitudinal seam joining to circumferential shell assembly and nozzle overlays.

Heavy Longitudinal & Circ Seams
Endeavour 1250 CCCV

Submerged Arc Welding (SAW) System

Engineered specifically for heavy plate joint filling. Delivers up to 1250 Amperes at 100% duty cycle, ensuring ultra-deep penetration, smooth bead profile, and zero slag inclusion on carbon steel (e.g., SA-516 Gr 70) and low-alloy plates up to 100mm+ thick.

  • Output Current100A – 1250A CC/CV
  • Duty Cycle100% @ 1250A (40°C)
  • Primary ProcessSAW (Tractor / Boom)
  • Secondary ProcessesMIG, Gouging, MMA
Shell Turning & Alignment
Rotator Series

Heavy-Duty Tank & Vessel Rotators

Heavy-walled pressure vessel shells demand precise rotational speed matching to avoid weld bead deformation during circumferential submerged arc welding. APS conventional and self-aligning rotators feature metallic polyurethane rollers and VFD vector motor drives.

  • Capacity Range5 Tons to 250+ Tons
  • Drive TypeAC Inverter / VFD Dual Motor
  • Speed SynchronizationDigital Interface with SAW Head
  • Roller ConstructionHeavy Steel with Polyurethane
Root Pass & Stainless Cladding
Apollo Pulse TIG

Precision GTAW Inverter Source

For high-pressure vessel root passes and internal stainless steel or Inconel corrosion-resistant alloy (CRA) overlays. Offers precision high-frequency arc starting and customizable pulse frequency to manage heat input and prevent toxic burn-through on alloy pipes and stubs.

  • ProcessesDC Pulse TIG / MMA
  • Memory Slots10 Programmable Schedules
  • Pulse Control0.5 Hz to 500 Hz fully adjustable
  • Arc TrackingBuilt-in Weld-O-Meter
Joint Back-Gouging
CAG Heavy Series

Carbon Arc Gouging Power Source

Essential for back-gouging root runs on double-bevel pressure vessel plates before starting second-side Submerged Arc Welding. Provides constant, stable DC voltage to rapidly vaporize metal without carbon deposition in the joint preparation area.

  • Current OutputUp to 1200A Continuous
  • Gouging Electrodes3.2mm to 12.7mm Carbons
  • Removal RateHigh-speed gouging efficiency
  • ProtectionThermal & Over-voltage auto-cut
Dish Head & Nozzle Welding
Positioner Series

Motorized Heavy Positioners

Ensures downhand welding orientation for dished heads, heavy nozzles, flanges, and vessel end covers. Motorized 135-degree tilt and 360-degree rotation eliminate overhead and vertical out-of-position defects, maximizing deposition speed.

  • Payload Rating500 kg to 20,000 kg
  • Tilt MechanismMotorized / Hydraulic Gear Drive
  • Control SystemRemote pendant with speed LED
  • EarthingHeavy Copper Rotary Grounding
Multi-User Bay System
Multi-Operator Grid

Heavy Workshop Central Power Grid

Ideal for crowded pressure vessel manufacturing bays where multiple fitters and welders perform tacking, attachment welding, and nozzle fit-ups simultaneously. Consolidates power drops, lowers shop energy demand, and withstands harsh workshop duty.

  • Operator Bays4 to 8 Independent Stations
  • TechnologyEnergy-Saving Inverter Grids
  • RuggednessIP23 Enclosure for Site & Plant
  • Efficiency>88% Power Factor Efficiency
Engineering Selection Matrix

Welding Process Comparison for Pressure Vessel Fabrication Seams

Selecting the appropriate welding process for specific pressure vessel joints is vital for balancing mechanical performance, NDT compliance, and overall fabrication cost.

  • Apollo Pulse TIG Series with HF Start
  • Vessel Fabrication Seam / Application Primary Process Deposition Rate (kg/hr) NDT / X-Ray Reliability Recommended APS Power & Automation Setup
    Longitudinal Shell Joints (>25mm Carbon/Alloy Steel) Submerged Arc Welding (SAW) 8.0 – 15.0+ Exceptional (>99% pass) Endeavour 1250 CCCV + Heavy SAW Tractor
    Circumferential Shell Seams (Ring-to-Ring Assembly) Tandem / Single SAW 7.5 – 14.0 Exceptional (>99% pass) Endeavour 1250 SAW + VFD Tank Rotators
    Root Pass Seam Welding (Open Root Bevels) DC Pulse TIG (GTAW) 0.8 – 1.8 Maximum Integrity
    Root Joint Back-Gouging (Double Bevel Preparation) Carbon Arc Gouging (CAG) N/A (Removal) Clears Defect Pocket 1200A Carbon Arc Gouging Source
    Nozzle-to-Shell & Flange Assembly Fillets Pulse MIG / FCAW 3.5 – 6.5 High (>96% pass) MIG CC/CV Multiprocess + Heavy Positioner
    Complete Turnkey Vessel Bay Package SAW + TIG + Gouging + Auto Optimized Fleet Zero-Defect Goal Get a Quote for Complete Package

    *Note: Deposition rates and pass percentages depend on joint design, edge bevel precision, flux conditioning, and welder qualification. Consult APS application engineers for WPS assistance.

    Authority, Expertise & Reliability

    Why Global Pressure Vessel Fabricators Partner with APS Welding

    When procuring high-capacity welding machinery for critical pressure vessel contracts, dealing directly with an authentic equipment manufacturer—rather than an OEM rebranding trading company—is essential for operational risk management.

    01

    20+ Years In-House R&D

    Advanced Power Sources Limited designs its IGBT inverter topologies, PCB layouts, and firmware control logic directly in Gujarat, India. We do not rely on third-party design imports, giving us full authority to customize arc characteristics for unique vessel alloys.

    02

    ISO 9001:2015 Quality Controls

    Every welding power source, rotator, and positioner undergoes stringent load-bank testing, thermal stress simulation, and insulation resistance checks at our Old GIDC Gundlav plant before export shipment.

    03

    22,600+ Global Installations

    Our equipment powers production lines across heavy fabrication, chemical reactors, oil & gas refineries, power station boilers, and shipbuilding yards worldwide, backed by field-proven longevity.

    04

    Direct Engineering Support

    Overseas buyers gain direct access to our application engineering team for WPS optimization, joint preparation advice, custom electrical phase matching, and rapid spare parts dispatch.

    Technical Procurement Protocol

    5-Point Sourcing Checklist for Pressure Vessel Machinery Procurement

    Avoid costly site commissioning delays and operational downtime by verifying these critical engineering factors prior to issuing purchase orders.

    Get a Quote & Request Technical Audit
    1. Duty Cycle Verification at High Amperage

      Ensure power sources are rated at 100% duty cycle at ambient temperatures of 40°C under IEC 60974-1 standards. SAW operations on heavy vessel seams require hours of unbroken arc time without thermal shutdown.

    2. Utility Grid Voltage & Generator Compatibility

      Confirm the power source tolerates input voltage swings of ±15%. Remote fabrication yards running on diesel generator power experience severe frequency variations that disrupt delicate arc controls if unprotected.

    3. Rotator & Positioner Torque Ratings

      Verify that tank rotator load capacities account for asymmetrical vessel center-of-gravity (CG) shifts caused by thick nozzles, manways, and internal tray supports during rotation.

    4. Digital Interface for Automation Systems

      Check whether current and voltage outputs feature open digital communication protocols (RS485/Modbus/Analog 0-10V) to integrate seamlessly with column-and-boom manipulators and seam-tracking sensors.

    5. Spare Parts & Local Technical Support

      Audit the manufacturer's spare board availability, IGBT component modularity, and availability of trained field service engineers to ensure long-term equipment uptime.

    Addressing Global Procurement Queries

    Pressure Vessel Manufacturing Industry FAQ

    Expert answers to complex technical and sourcing queries asked by pressure vessel QA/QC managers, EPC procurement directors, and welding engineers.

    How do inverter-based SAW power sources improve NDT/RT pass rates in pressure vessel manufacturing?

    Inverter-based Submerged Arc Welding (SAW) power sources deliver millisecond-level dynamic current regulation and precise closed-loop feedback. Unlike legacy transformer units, IGBT inverters minimize voltage fluctuations during deep-groove longitudinal and circumferential seam welding. This consistency virtually eliminates slag inclusions, lack of sidewall fusion, and centerline cracking, enabling pressure vessel fabricators to consistently achieve 100% X-ray (Radiographic Testing) and Ultrasonic Testing pass rates under ASME Section VIII and EN 13445 standards.

    What heat input control mechanism is recommended for high-strength pressure vessel steels like SA-516 Gr 70 or SA-387?

    High-strength carbon and alloy pressure vessel steels require strict heat input management to preserve toughness in the Heat Affected Zone (HAZ) and prevent hydrogen-assisted cracking. Advanced IGBT power sources integrated with IoT systems like WeldVisor real-time monitoring allow engineers to maintain exact Amperage, Voltage, and Travel Speed limits. Synchronized waveform control and automated pulse modes optimize bead geometry while delivering repeatable thermal cycles that comply with approved Welding Procedure Specifications (WPS).

    How do you synchronize welding rotators with SAW systems to prevent circumferential seam defects?

    Circumferential seam integrity relies on zero slip and precise rotation speed matching. Variable Frequency Drive (VFD) controlled motorized rotators with high-torque AC motor drives are interfaced directly to the SAW tractor or column and boom controller via digital I/O. This ensures smooth surface speed regulation (in mm/min) regardless of vessel diameter or weight distribution, eliminating weld bead overlap, necking, and burn-through on heavy-wall shell sections.

    What duty cycle rating is required for continuous heavy-wall vessel fabrication?

    Pressure vessel manufacturing demands 100% continuous duty cycle ratings at max working current (e.g., 1000A to 1250A) tested at 40°C ambient temperature under IEC 60974-1 standards. Heavy multi-pass welding on thick shells (50mm+) cannot tolerate thermal cut-offs, as stopping mid-pass causes restart defects, interpass contamination, and thermal stress points.

    How does carbon arc gouging affect HAZ prior to back-welding pressure vessel seams?

    Carbon Arc Gouging (CAG) is used to clear root passes and achieve full-penetration double-welded butt joints. High-amperage, stable DC gouging power sources remove root defects quickly with minimal heat input, producing a smooth groove with low carbon pickup. Proper air pressure and high-output arc stability prevent surface carburization, reducing grinding labor before back-welding with Submerged Arc or Flux-Cored processes.

    Can APS Welding customize equipment to match specific international factory power grids?

    Yes. Advanced Power Sources Limited engineers IGBT inverter welding equipment with ultra-wide input voltage tolerances (380V to 480V, 3-Phase, 50/60 Hz). This safeguards electronics against severe voltage sags and surges common in heavy manufacturing plants, ensuring stable output across global plant locations in North America, Europe, the Middle East, and Asia-Pacific.

    Accelerate Your Pressure Vessel Fabrication Productivity

    Contact Advanced Power Sources Limited today to discuss custom submerged arc welding setups, heavy rotators, or factory grid configurations.

    Get a Quote