
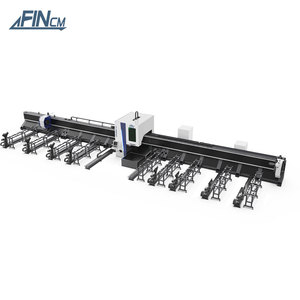
High-duty cycle IGBT inverter power sources, laser tube cutters, orbital MIG/TIG systems, and heavy structural welding positioners engineered for European industrial standards.
A comprehensive analysis of why Austrian structural steel fabricators, automotive suppliers, and machinery plants are upgrading from traditional transformers to digital multiprocess CC-CV inverter systems.
Austrian structural fabricators operating under EN 1090-2 (Execution Classes EXC1 to EXC4) require precise energy-input control to maintain joint ductility and notch toughness. Modern synergic multiprocess GMAW MIG power sources deliver digital arc regulation, ensuring heat input remains strictly within validated Welding Procedure Specifications (WPS).
With Austria leading stringent European industrial energy benchmarks, industrial plants in Upper Austria and Styria are replacing energy-intensive transformer welders. IGBT inverter technology yields up to 35% energy savings, higher power factor correction (PFC > 0.95), and negligible idling losses.
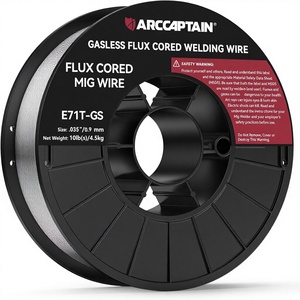
Industrial manufacturing facilities require versatility. A single Constant Current / Constant Voltage (CC-CV) power source allows seamless switching between GMAW (MIG/MAG short arc, spray arc, pulsed arc), FCAW (flux-cored), SMAW (stick electrode), and gouging, maximizing asset utilization per floor square meter.
From heavy machinery fabrication in Linz to high-precision alpine infrastructure in Tyrol, see how advanced GMAW power sources solve specific regional engineering challenges.
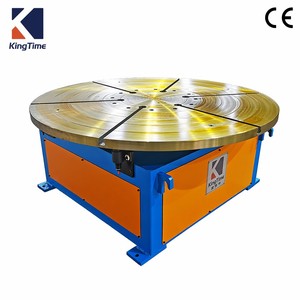
In the industrial heartland of Linz, metalworking enterprises routinely process thick-section carbon steels (S355J2+N, S690QL) and stainless vessel shells. Here, high-current CC-CV GMAW welders connected to motorized welding rotators and gantry lines perform continuous multi-pass welds with low spatter and high deposition rates. Integrating digital wire feed systems guarantees uniform filler wire delivery over long boom arms.
Styria's automotive engineering cluster demands high-frequency pulse GMAW capability for thin-gauge aluminum alloy (5000 and 6000 series) and high-strength galvanised steel. Synergic microprocessors rapidly adjust voltage and wire speed to eliminate burn-through while achieving flawless bead aesthetics and minimal thermal distortion.
Steel structures destined for alpine cableways, avalanche barriers, and bridges endure extreme cyclic stress and low ambient temperatures down to -30°C. Weld integrity under ÖNORM EN ISO 5817 Level B standards is mandatory. Multiprocess inverters featuring electronic hot-start and adjustable arc force prevent cold-lapping and lack-of-fusion defects on critical structural nodes.
Stainless steel fabrication for Austria's renowned beverage, brewing, and pharmaceutical sectors demands corrosion-resistant joint chemistry. Utilizing pulsed GMAW with high-purity argon shielding gas mixtures minimizes chromium depletion in the heat-affected zone (HAZ), reducing post-weld pickling and passivation labor.
Architectural specifications designed for 400V 3-phase European industrial grid compliance (EN 60974-1 / CE certified).
| Performance Specification | Synergic GMAW 350A Class | Heavy-Duty GMAW/CC-CV 500A | Ultra-Industrial GMAW/SAW 1250A |
|---|---|---|---|
| Primary Input Voltage | 400V ±15%, 3-Phase, 50/60 Hz | 400V ±15%, 3-Phase, 50/60 Hz | 400V ±15%, 3-Phase, 50/60 Hz |
| Duty Cycle Rating (40°C Ambient) | 60% @ 350A / 100% @ 270A | 100% @ 500A (Continuous Heavy Duty) | 100% @ 1250A (Automation Line Ready) |
| Supported Processes | GMAW (MIG/MAG), FCAW, SMAW, GTAW | GMAW, FCAW, SMAW, Carbon Arc Gouging | GMAW Heavy Deposition, SAW, Gouging |
| Inverter Circuitry Architecture | Dual-Module IGBT 60 kHz High-Freq | Heavy-Duty Dual IGBT Module Array | Multi-Inverter Parallel Module Topology |
| Wire Feed Speed Range | 1.5 – 22 m/min (4-Roll Encoder Feed) | 1.5 – 24 m/min (Digital Closed-Loop) | Submerged Arc Tractor Feed / Boom Feed |
| Supported Wire Diameters | 0.8 / 1.0 / 1.2 / 1.6 mm | 1.0 / 1.2 / 1.6 / 2.4 mm (Solid & Flux) | 2.0 / 3.2 / 4.0 / 5.0 mm Solid Wire |
| Protection Class & Insulation | IP23S / Class H Insulation | IP23S / Class H Insulation | IP23S Heavy Duty Enclosure |
| Recommended Local Applications | Automotive sub-assemblies, sheet metal | Structural steel EN 1090 EXC3, vessels | Shipbuilding, wind towers, gantry SAW |
Why next-generation digital waveform regulation provides unparalleled weld pool stability and mechanical strength.
Traditional MIG welders suffer from explosive droplet transfer during dip-transfer MIG welding, resulting in heavy spatter and poor weld appearance. High-speed DSP control monitors arc voltage and current waveform every microsecond, automatically tailoring current ramp-down before droplet separation to eliminate spatter formation completely.
Operative efficiency is vastly improved via pre-loaded digital synergic curves. Operators select base material type, wire diameter, and shielding gas blend; the power source instantly calculates optimal wire feed rate, peak pulse current, background current, and pulse frequency. This reduces machine setup time by up to 70%.
Our heavy-duty power sources incorporate isolated wind-tunnel cooling ducting. Critical electronic printed circuit boards (PCBs) are isolated from incoming dusty cooling airflow, shielding IGBT modules and microprocessors against metallic dust, humidity, and atmospheric pollutants common in industrial heavy-engineering environments.
Why dealing directly with an ISO 9001:2015 certified original equipment manufacturer provides superior value, engineering support, and long-term security for Austrian industrial buyers.
Unlike brand-label traders who assemble components from unverified sub-suppliers, our factory engineers and manufactures every core subsystem in-house: from high-frequency inverter transformers and surface-mount PCB control boards to sheet metal enclosures and wire feeder units. This ensures total design coherence and direct engineering responsibility for performance reliability.
Every single power source undergoes rigorous full-load burn-in testing, insulation resistance checking, and artificial heat-chamber duty cycle validation prior to container loading. Testing protocols strictly mirror IEC 60974-1 standards at 40°C ambient temperatures, guaranteeing that rated duty cycles match real-world factory continuous production conditions.
We supply tailored equipment configurations matching Austrian grid requirements (400V 3-Phase 50Hz with wide input voltage tolerance ±15% to withstand generator supply spikes on alpine job sites). Custom digital interface protocols (CANopen, Modbus, Profinet) enable effortless integration with robotic welding cells and central SCADA systems.
By eliminating multiple intermediary distributor layers, factory-direct clients receive complete modular replacement board kits, torch consumables, wire feeder drive rolls, and direct application support from our senior power electronics engineers, minimizing long-term total cost of ownership (TCO).
Technical and procurement answers for industrial managers, welding coordinators, and import specialists in Austria.
Yes. All our industrial multiprocess inverter power sources are engineered and manufactured in strict compliance with EN 60974-1 (Safety Requirements for Arc Welding Equipment), EN 60974-10 (Electromagnetic Compatibility - EMC), and carry the CE mark. They fully meet Austrian industrial grid standards (400V, 3-Phase, 50 Hz) and insulation class requirements.
EN 1090-2 requires structural steel fabricators to control welding energy input (kJ/mm) within specified limits to ensure microstructural integrity. Our digital synergic power sources allow precise setting and locking of voltage, wire feed speed, and pulse parameters. Furthermore, real-time digital volt/amp meters provide verified readout values for welding procedure qualification records (WPQR).
A Constant Current / Constant Voltage (CC-CV) machine combines multiple power characteristics into one chassis. In a busy workshop in Linz or Graz, a single operator can execute heavy MIG/MAG wire welding on carbon steel plates, switch to DC TIG for root pass joint preparation, perform SMAW stick welding on site out-of-position joints, or run high-current carbon arc gouging to remove root defects without acquiring four separate power sources.
Duty cycle is tested rigorously according to International standard IEC 60974-1 over a 10-minute test cycle inside a climate-controlled room set to 40°C ambient temperature. A machine rated at 100% duty cycle at 500A can operate continuously for 10 minutes out of 10 minutes without thermal shutdown. This guarantees zero downtime even during hot Austrian summer workshop operations.
Absolutely. Our power sources come standard with automation interfaces, supporting remote start/stop, voltage reference input, wire feeder speed synchronization, arc feedback signals, and digital fieldbus connectivity. They seamlessly pair with our industrial welding positioners, rotators, welding carriages, and gantry platforms.
We supply comprehensive spare parts kits (including control boards, drive rollers, IGBT modules, solenoid valves, and torch consumables) alongside machinery shipments. Our senior engineering team provides direct video support, application guidance, parameter optimization, and circuit schematics to keep your production line running without interruption.
Click the "Inquire Now" button below or on any product card. Provide your target welding process, material thickness range, input supply specifications, and required monthly production output. Our technical sales engineers will prepare a detailed engineering specification proposal and direct factory price quote within 24 hours.
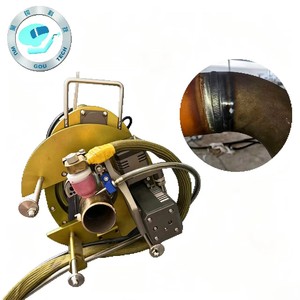
Consult with our senior application engineers to select the exact multiprocess GMAW MIG inverter, orbital pipe cutter, or heavy welding automation positioner for your Austrian production facility.