
Explore our high-performance welding oscillators, column and boom stations, fiber laser cutters, and heavy-duty automatic welding systems deployed across global industrial fabrication hubs.
In high-integrity metal joinery, achieving optimal sidewall fusion, controlled heat input, and defect-free multi-pass bead geometry requires precise mechanical torch weaving. As a premier China welding oscillator manufacturer supplying engineering clients across Abu Dhabi, Dubai, Sharjah, and Ras Al Khaimah, we deliver advanced digital torch weavers engineered to meet strict ASME Section VIII, API 1104, and AWS D1.1 specifications.
A welding oscillator (torch weaver) is a precision motorized slide assembly that moves a TIG (GTAW), MIG/MAG (GMAW), FCAW, or SAW torch back and forth across a joint seam in controlled patterns—linear, trapezoidal, pendulum, or spiral. By accurately regulating parameters such as weaving width (amplitude), oscillation speed, left/right dwell times, and center pause, our oscillators eliminate common manual welding defects including lack of sidewall fusion, undercut, excessive heat-affected zone (HAZ) grain growth, and slag inclusions.
Independently adjustable left and right dwell times (0.0 to 9.9 seconds) ensure complete molten pool soaking at the groove faces, eliminating cold laps in heavy plate joints.
Micro-stepping motor drive coupled with precision ball screw slides delivers linear weaving repeatability of ±0.1 mm, preventing arc deflection and bead irregularity.
Controlled weaving distributes arc energy over a broader width, reducing overall thermal distortion on duplex stainless steel and high-strength alloy structures.
The United Arab Emirates represents one of the world's most demanding fabrication environments. From offshore oil rigs in Abu Dhabi to iconic skyscraper steel frames in Dubai, our welding oscillators are engineered to deliver 24/7 reliability under extreme ambient temperatures exceeding 50°C.
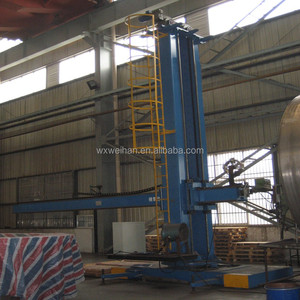
In Abu Dhabi's industrial zones (ICAD Musaffah and Ruwais Industrial Complex), fabricators producing heavy-wall pressure vessels, desalter columns, and heat exchangers utilize our linear welding oscillators integrated with Column and Boom systems. Oscillating circumferential and longitudinal seams under Submerged Arc Welding (SAW) or Heavy FCAW guarantees 100% radiographic quality compliant with ASME VIII Div 1 & Div 2 standards.
At Jebel Ali Free Zone (JAFZA) and Dubai Maritime City, shipyards handle continuous repair and newbuild construction of offshore jack-up rigs, barges, and supply vessels. Our lightweight portable motorized weavers are mounted onto magnetized tractors for vertical (3G) and overhead (4G) shell plate butt welding, dramatically reducing operator fatigue while increasing metal deposition rates by over 180% compared to stick manual welding.
Structural steel fabricators across Hamriyah Free Zone (Sharjah) and Al Ghail Industrial Zone (Ras Al Khaimah) produce heavy box columns, bridge girders, and stadium trusses. Our 2-axis CNC oscillators allow automated multi-layer fillet weaving, achieving smooth bead profiles with zero undercut on thick structural plates.
Overland crude and gas transmission pipelines require high-precision root and capping passes. Combining our digital pulse TIG oscillators with orbital pipe welding carriages ensures consistent root penetration and weld metal purity when joining high-yield API 5L X65 to X80 line pipes under high-humidity coastal conditions.
Quantifying the ROI of automated torch weaving in UAE industrial workshops:
| Performance Metrics | Manual Hand Torch Weaving | Basic Analog Weaver | APS Digital 2-Axis CNC Oscillator |
|---|---|---|---|
| Positioning Accuracy | Operator dependent (±2.0 mm) | Potentiometer controlled (±0.5 mm) | Digital Stepper / Ball Screw (±0.1 mm) |
| Dwell Time Control | Irregular / Subjective | Basic uniform pause | Independent Left / Center / Right (0-9.9s) |
| Deposition Rate Efficiency | Baseline (100%) | 140% - 160% increase | 220% - 300% increase |
| Defect Rate (UT / RT Failure) | 8% - 15% in heavy wall joints | 3% - 5% | < 0.5% (ASME Class Zero Defect) |
| Ambient Temp Resistance | Limited by welder endurance | Up to 40°C limit | Heavy-Duty Industrial Duty (Up to 55°C) |
| Automation Integration | None | Standalone only | Full PLC / Column & Boom / Robot Interface |
As the UAE accelerates its national industrial strategy—"Operation 300bn"—and expands the In-Country Value (ICV) Program across ADNOC and government procurement sectors, engineering firms are forced to modernize production lines. Key market shifts include:
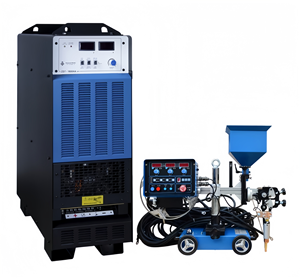
Our oscillators are natively engineered to integrate with our proprietary IGBT inverter power sources (MIG CC-CV, TIG Pulse, and Submerged Arc), providing synchronized arc start/stop and auto-stop upon cycle completion.
Modules can be expanded from single linear oscillation to 2-axis radial/cross-seam tracking, enabling multi-pass filling of non-uniform pipe joints without manual torch adjustment.
With established supply lines to Dubai (JAFZA) and Abu Dhabi (Musaffah), we deliver replacement motor packs, control cards, and slide brackets with minimal lead times.
Direct sourcing from a certified Chinese manufacturer like our facility bridges the gap between premium European-grade mechanical accuracy (±0.1mm linear precision) and cost optimization. With over 20 years of dedicated R&D, ISO 9001:2015 certification, and 22,600+ global installations, our systems provide rugged construction tailored for Middle Eastern industrial duty without excessive intermediary markups.
X-ray and UT failures in heavy-wall pressure vessels typically result from lack of sidewall fusion or slag entrapment between weld passes. By programming precise left and right dwell times (e.g., holding the arc at the joint sidewall for 0.8 seconds while moving swiftly across the center), the oscillator ensures complete metal fusion into the base metal groove face while giving slag time to float to the surface.
Yes. All electronic controllers, stepper motors, and slide mechanisms supplied to the United Arab Emirates are built with ambient temperature tolerances rated up to 55°C. Internal PCB assemblies receive conformal anti-dust coatings, and drive housings meet IP54 ingress protection against sand and fine particulates common in desert industrial areas.
Our oscillators feature universal torch mounting clamps suitable for Gas Metal Arc Welding (MIG/MAG), Flux-Cored Arc Welding (FCAW), Gas Tungsten Arc Welding (TIG/GTAW with or without cold wire feeding), and Submerged Arc Welding (SAW) torches. They can be mounted onto carriages, column and booms, or fixed automation gantries.
Standard model oscillators are maintained in stock for rapid dispatch. Air freight shipments to Dubai International (DXB) or Abu Dhabi (AUH) typically arrive within 5 to 7 working days. Bulk equipment orders or integrated Column & Boom systems shipped via sea freight to Jebel Ali Port or Khalifa Port take approximately 18 to 22 days from dispatch.
Absolute reliability is core to our brand value. We provide comprehensive operational manuals, wiring schematics, and remote video commissioning assistance with experienced application engineers. All wearing parts—including drive belts, ball screws, motor controllers, and torch clamps—are backed by long-term spare parts availability.
Simply click the "Inquire Now" button on this page to open our instant engineering inquiry window. Share your required welding process (TIG/MIG/SAW), material thickness, current payload requirements, and site input voltage, and our application specialists will respond with a tailored technical proposal within 24 hours.
Connect directly with our senior engineering team to select the ideal linear, pendulum, or multi-axis welding oscillator for your project.