
Proven power sources, heavy-duty positioners, and automated arc systems for critical industrial applications across Doha, Ras Laffan, and Mesaieed.
An authoritative technical guide on optimizing circumferential and longitudinal joint fabrication in heavy-wall pressure vessels, LNG cryogenic spools, and utility pipelines across the State of Qatar.
As Qatar accelerates its energy sector modernization—underpinned by the multi-billion dollar North Field East (NFE) and North Field South (NFS) LNG expansion projects—the structural requirements placed upon fabricators in the Doha Industrial Area, Ras Laffan Industrial City, and Mesaieed Industrial Zone have undergone a radical transformation. Modern engineering standards set by QatarEnergy, Ashghal (Public Works Authority), and Kahramaa demand zero-defect metallurgical integrity, absolute geometric concentricity, and 100% Non-Destructive Testing (NDT) compliance under Radiographic (RT) and Ultrasonic (UT) examination.
Manual and semi-automatic pipe welding techniques, while historically viable, present severe bottlenecks in duty cycle, heat input management, and linear deposition rates. Human welder fatigue, ambient working temperatures exceeding 45°C during Gulf summers, and the strict interpass thermal controls required for duplex, super duplex, and P91 alloy steel piping mandate the integration of automated mechanical motion systems. The heavy-duty Column and Boom Pipe Welding Manipulator has emerged as the cornerstone technology for EPC contractors, spool fabricators, and vessel manufacturers operating within Qatar.
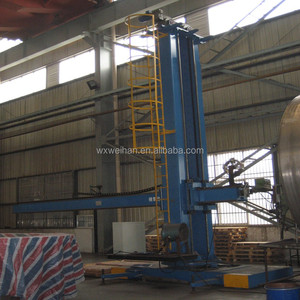
By synchronizing precise linear boom movement with motorized anti-drift rotators and advanced inverter-based power sources (SAW, GMAW, GTAW, and FCAW), column and boom manipulators convert complex manual weld joints into repeatable, highly efficient automated processes. This whitepaper analyzes the mechanical architecture, local thermal adaptations, procurement specifications, and localized application scenarios essential for engineering teams seeking to deploy manipulator technology in the Doha market.
A industrial pipe welding manipulator is not merely a boom mounting structure; it is a high-precision, low-deflection kinematic system engineered to deliver smooth, vibration-free torch delivery across extended operational radii. When depositing heavy Submerged Arc Welding (SAW) passes or multi-run FCAW fill layers, even sub-millimeter boom tip deflection can introduce tracking errors, leading to side-wall lack of fusion, slag inclusion, or irregular bead profile.
Engineered using stress-relieved heavy structural box sections with dual linear guideways. Boom deflection is held under 1.5 mm at full horizontal reach (up to 6 meters), eliminating torch chatter and joint deviation during deep-groove SAW cycles.
Inverter-driven AC gear motors coupled with precision anti-backlash rack-and-pinion drives deliver stepless speed control (100 to 2000 mm/min). Digital encoder feedback ensures instantaneous velocity stabilization under variable load mass.
Features heavy-duty mechanical anti-fall safety pawls and redundant counterweight cable systems. In the event of primary chain tension loss, instantaneous mechanical locking prevents boom free-fall, protecting shop floor technicians and high-value workpieces.
Industrial manufacturing across Qatar spans several high-consequence sectors. Each application presents specific metallurgical, dimensional, and environmental challenges that require custom manipulator configurations.
Operational Context: Fabrication of 9% Nickel steel cryogenic pipe spools, heavy-wall stainless steel (316L/304L), and thick carbon steel pressure vessel shells for LNG train expansions.
Manipulator Solution: 4x4 Heavy-Duty Column and Boom Manipulators equipped with TIG (GTAW) cold wire feed for root passes and Submerged Arc Welding (SAW) tandem heads for high-deposition shell filling. Fully integrated with self-aligning rotators featuring polyurethane-lined rollers to prevent surface iron contamination on stainless and nickel alloys.
Operational Context: Large-diameter chilled water headers (DN1200 to DN2400) for Marafeq Qatar and Ashghal stormwater/sewerage trunk mains require thousands of linear meters of external circumferential butt welds.
Manipulator Solution: High-speed travel carriage manipulators operating on fixed floor rails. Using Flux-Cored Arc Welding (FCAW) with dual-shield wire, these units achieve multi-pass circumferential welds in a fraction of manual layout time while meeting stringent QCS 2018 structural standards.
Operational Context: Heavy structural piling, jacket legs, and conductor pipes with wall thicknesses ranging from 25mm to 80mm subjected to harsh marine corrosion and high fatigue loads.
Manipulator Solution: 6x6 Heavy-Duty Column and Boom systems outfitted with Narrow Gap SAW technology. Narrow gap bevel preparation reduces weld metal volume by up to 50%, significantly shortening thermal cycles and reducing heat-affected zone (HAZ) embrittlement.
Operational Context: High-pressure steam lines and seawater intake manifolds fabricated from Super Duplex Stainless Steel (UNS S32750) and Chrome-Moly alloys (P11, P22, P91).
Manipulator Solution: Precision Pulsed GTAW/GMAW automated manipulators featuring closed-loop Arc Voltage Control (AVC) to ensure exact interpass temperature regulation and controlled heat input, preserving ferrite-austenite phase balance.
Selecting the appropriate column and boom configuration requires matching mechanical payload, stroke envelope, and process integration to production demands. The matrix below outlines standard industry classes available for Doha fabricators:
| Manipulator Series | Effective Reach (H x V) | Max Boom Load | Primary Process | Target Application |
|---|---|---|---|---|
| Light-Duty (L-CBM) | 1.5m x 1.5m to 2.5m x 2.5m | 50 kg - 80 kg | Precision TIG / MIG | Small pipe spools (DN50 - DN300), thin-wall tanks, hardware fittings |
| Medium-Duty (M-CBM) | 3.0m x 3.0m to 4.0m x 4.0m | 150 kg - 250 kg | MIG / Single-Wire SAW | District cooling mains, medium pressure vessels, structural columns |
| Heavy-Duty (H-CBM) | 5.0m x 5.0m to 6.0m x 6.0m | 350 kg - 500 kg | Tandem SAW / Heavy FCAW | LNG storage vessels, heavy wall piping, oil refinery headers |
| Extra Heavy Telescopic | 6.0m x 6.0m up to 9.0m x 9.0m | 800 kg+ | Multi-Wire SAW / Narrow Gap | Shipyard piling, offshore jacket legs, large boiler drums |
The industrial sector in Qatar is undergoing rapid technology adoption driven by economic diversification mandates under Qatar National Vision 2030 and regional labor dynamics:
The Gulf Cooperation Council (GCC) region faces increasing competition for certified high-alloy 6G welders. Automated column and boom manipulators allow a single operator to supervise dual automated cells, multiplying volumetric weld output by 300% to 500% while reducing dependence on scarce manual labor.
Modern Doha workshops are increasingly adopting real-time weld monitoring platforms, such as the WeldVisor IoT Monitoring System. By transmitting arc-on time, voltage, current, wire feed speed, and total heat input directly to cloud dashboards, QA/QC managers achieve full traceability for every linear meter of weld joint, simplifying ASME and QatarEnergy audit compliance.
Equipment deployed in Qatar must withstand summer ambient temperatures exceeding 45°C–50°C in unconditioned workshop bays, alongside ambient airborne particulate dust. Modern manipulators incorporate IP55-rated sealed electrical cabinets, heavy-duty cooling fans, climate-controlled inverter enclosures, and double-sealed linear bearings to prevent premature component failure.
When investing in capital automation equipment for export to Qatar, buyers require direct OEM accountability rather than third-party trading intermediaries. Advanced Power Sources Limited (APS Welding) brings over two decades of dedicated R&D and manufacturing excellence to international project execution.
Every IGBT inverter board, control cabinet, heavy structural column, and positioner is designed, machined, assembled, and load-tested in-house at our ISO 9001:2015 certified facility in Gujarat, India, ensuring direct engineering oversight.
With over 22,600+ welding power sources and automation systems installed globally, our equipment operates reliably across heavy engineering, shipbuilding, power plants, and oil & gas projects worldwide.
We deliver unified system packages—combining Column & Boom manipulators, self-aligning rotators, SAW/MIG power sources, flux handling, and WeldVisor IoT telemetry from a single OEM point of contact.
Our engineering team provides comprehensive pre-sale application reviews, helping Doha fabricators calculate deposition rate gains, cycle time reductions, and return on investment (ROI) prior to equipment selection. Furthermore, spare parts availability and direct factory technical support ensure uninterrupted operational uptime throughout project lifecycles.
Essential technical and logistical answers for purchasing managers, QA/QC heads, and workshop directors serving the Doha industrial market.
Our pipe welding manipulators and paired inverter power sources are engineered specifically for continuous industrial duty in high-ambient environments up to 50°C. Heavy-duty power electronics feature high-efficiency heat sinks, forced air cooling tunnels, over-temperature protection sensors, and IP55-rated dust-resistant control enclosures. This design prevents thermal trips and component degradation during long summer shifts in Doha workshop facilities.
Yes. Our manipulators, paired with APS SAW or GTAW/GMAW power sources, deliver precise speed control, repeatable heat input management, and smooth motion required to satisfy 100% Radiographic Testing (RT) and Ultrasonic Testing (UT) under ASME Section VIII, ASME B31.3, API 650, and Qatar Construction Specifications (QCS). Integrated digital speed displays and optional WeldVisor IoT logging allow QA teams to verify parameters against approved Welding Procedure Specifications (WPS).
Equipment supplied to Qatar is configured for standard local industrial supply: 415V, 3-Phase, 50Hz AC power (tolerating ±10% voltage fluctuation). Control transformer circuits operate at safe low-voltage levels (24V/110V AC/DC) for operator safety. Generator-friendly inverter power source options are also available for remote field fabrication sites.
Absolutely. Our manipulators feature universal boom-end mounting plates and modular cable management tracks. You can install a heavy Submerged Arc Welding (SAW) head alongside a Gas Metal Arc / Flux-Cored (GMAW/FCAW) torch package. Quick-change bracketry and dual-process control pendants allow operators to switch between root-pass MIG/FCAW and fill-and-cap SAW in minutes.
We ship directly from our main manufacturing hub in Gujarat, India—benefiting from direct, frequent maritime shipping routes to Hamad Port (Doha). Standard manufacturing and assembly lead time ranges from 3 to 5 weeks depending on custom boom lengths and automation accessories, followed by a short 5-to-7 day sea transit time, ensuring rapid project mobilization.
APS Welding provides complete remote and on-site commissioning support. Every system includes detailed installation manuals, electrical schematics, and video commissioning guides. Our factory-trained application engineers are available for on-site setup, operator training, and maintenance servicing across Doha, Ras Laffan, and Mesaieed industrial areas.
Speak with an APS application engineer to review your drawing specifications, calculate deposition gains, and receive a customized Column & Boom manipulator quotation tailored to your project requirements.
Inquire Now