
Heavy-duty, automation-ready machinery configured for high-reliability manufacturing in New Zealand
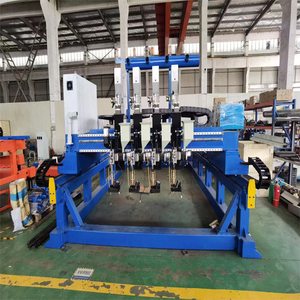
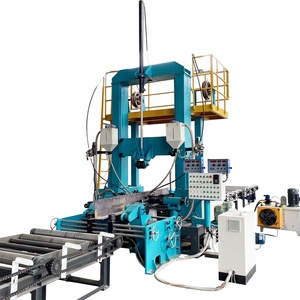
Longitudinal seam welding is the bedrock of cylindrical, conical, and flat-sheet metal fabrication. Designed to complete continuous, high-integrity butt joint welds along straight linear axes, modern automated longitudinal seam welders serve as essential equipment for fabricators transitioning from manual processes to repeatable, high-output production lines. For engineering houses, tank builders, and structural tube fabricators in New Zealand, obtaining zero-defect, 100% full-penetration welds with minimal heat distortion is paramount.
As a specialized OEM/ODM manufacturer, our automated longitudinal seam welding machinery integrates state-of-the-art kinematic motion controls, precision pneumatic finger clamping systems, and specialized copper backing bars with internal gas purging capabilities. Whether utilizing TIG (GTAW), Plasma Arc Welding (PAW), Submerged Arc Welding (SAW), or MIG/MAG (GMAW), our machinery provides absolute control over heat input, travel speed, and weld pool solidification dynamics.
A high-performance linear seam welder relies on mechanical stiffness and thermal dissipation. Our machine design incorporates several distinct engineering features:
New Zealand's industrial landscape demands extreme versatility. From the agricultural heartlands of Waikato and Canterbury to maritime centers in Auckland and infrastructure projects across Wellington and Christchurch, automated longitudinal seam welding plays a critical role in local supply chains.
Fabrication of thin-wall stainless steel (304L, 316L) pipes, heat exchangers, and storage tanks. Meets AS/NZS 1554.6 Class 1A sanitary welding criteria, yielding ultra-flat, cleanable interior seams resistant to bacterial growth.
Longitudinal joinery of thick-walled structural steel tubes (CHS and RHS profiles) subjected to high dynamic seismic loading. Configured with Submerged Arc Welding (SAW) heads for deep penetration under AS/NZS 1554.1 SP (Special Purpose) standards.
Joining marine-grade aluminum alloy sheets (5083, 6061) and structural longitudinal stiffness panels for commercial ferries, workboats, and pleasure yachts manufactured in Northland and Auckland shipyards.
Automated linear seam welding for high-pressure, corrosion-resistant alloy piping (Duplex, Super Duplex, Inconel-clad carbon steel) deployed in geothermal power extraction facilities in the Taupō and Rotorua regions.
High-volume production of galvanized, carbon steel, and aluminum ducting, water filtration vessels, and pressure tanks with automated seam tracking and repeatable cycle times under 60 seconds per meter.
Linear hardfacing overlay setups to protect wear-resistant plates and agricultural machinery ground-engaging tools against severe abrasive soils typical of Taranaki and Southland farming zones.
Selecting the optimal power source and torch setup for a longitudinal seam welder depends on material composition, wall thickness, and throughput requirements. Below is an engineering comparison matrix designed to guide procurement teams:
| Welding Process | Ideal Thickness Range | Key Advantage | Deposition Rate | NZ Industry Target |
|---|---|---|---|---|
| TIG (GTAW) Cold/Hot Wire | 0.5 mm – 4.0 mm | X-ray quality beads, zero spatter, pristine internal root profile | Low - Medium | Dairy, Beverage, Sanitary Tubing, Aerospace |
| Plasma Arc Welding (PAW) | 3.0 mm – 10.0 mm | Single-pass keyhole full penetration without beveling | Medium - High | Chemical Vessels, Heavy Stainless Pressure Tanks |
| Submerged Arc Welding (SAW) | 6.0 mm – 50.0+ mm | Extreme deposition rate, deep penetration, high duty-cycle | Very High | Seismic Structural Columns, Wind Towers, Heavy Pipe |
| MIG/MAG (GMAW/FCAW) | 1.5 mm – 12.0 mm | Fast travel speed, cost-effective consumables, high adaptability | High | General Structural Fabrication, Silos, HVAC Ducts |
| Fiber Laser / Hybrid Welding | 0.8 mm – 8.0 mm | Minimal heat distortion, ultra-high travel speed (>2m/min) | High Efficiency | High-Volume OEM Manufacturing, Precision Electronics |
The New Zealand fabrication sector faces a unique set of operating conditions: skilled welder shortages, stringent WorkSafe NZ health and safety mandates, rising labor costs, and increasing demand for verifiable quality tracking. Consequently, kiwi manufacturers are accelerating the adoption of smart linear welding automation.
Modern longitudinal seam welders supplied to the NZ market are increasingly retrofitted with smart IoT monitoring modules, such as WeldVisor. These systems log critical parameters in real time—including arc voltage, welding current, wire feed rate, heat input (kJ/mm), and travel speed. Fabricators supplying structural components under AS/NZS 1554 can instantly output digital weld logs for structural engineers and quality auditors, guaranteeing total traceability without manual paperwork.
Hexavalent chromium fumes generated during stainless steel welding are tightly regulated under New Zealand occupational health laws. Advanced OEM seam welders now incorporate integrated torch-head fume extraction hoods and fully enclosed safety interlock guards, ensuring operators are protected from airborne particulates and hazardous optical radiation emitted during continuous automated welding runs.
As fiber laser technology becomes more accessible, OEM buyers in New Zealand are moving from conventional TIG linear welding to hybrid laser-MIG or pure fiber laser longitudinal seam welders. Laser seam welders reduce total heat input by up to 70%, eliminating the post-weld hydraulic straightening operations typically required on thin gauge stainless steel sheets.
As an ISO 9001:2015 certified manufacturer with over 20 years of dedicated R&D and power source development experience, Advanced Power Sources Limited provides comprehensive OEM and ODM engineering services. We do not merely assemble components; we design the complete electronic, software, mechanical, and kinematic chain in-house.
We build seam welders handling part lengths from 300 mm up to 12,000 mm, accommodating tube diameters from 50 mm up to 3,000 mm+ with adjustable bed elevations.
Choose between Siemens PLC, Mitsubishi PLC, or proprietary digital microcontrollers featuring multi-language touchscreens (English/Māori UI available upon request).
ODM designs with dual-torch configurations (e.g., TIG root pass + MIG fill pass on a single linear carriage) to maximize throughput on thick-walled materials.
Before dispatch to New Zealand ports (Auckland, Tauranga, Lyttelton), every machine undergoes a full 48-hour continuous operational burn-in test. Our testing routine includes:
Clear answers to common technical, logistics, and compliance queries raised by engineering managers and procurement officers in New Zealand.