
Heavy-duty power sources, multi-torch robotic stations, 3D fixturing tables, and automated cladding systems optimized for continuous duty in heavy manufacturing cells.
The heavy engineering, infrastructure modernization, and energy processing sectors across the Central Federal District of Russia—anchored by the Moscow industrial cluster—are undergoing a major technological transformation. As industrial contractors and heavy plate fabrication yards ramp up output for structural bridge spans, pressure vessels, power generation infrastructure, and Arctic-bound modular plants, the demand for high-reliability joining systems has escalated. Processing structural steel plates exceeding 20mm to 100mm in thickness requires strict heat control, minimal angular distortion, high deposition rates, and arc stability tailored to sub-zero service environments.
Advanced Power Sources Limited (APS Welding) stands as a premier global manufacturer and exporter of heavy-duty IGBT inverter welding power sources, submerged arc welding (SAW) systems, multi-process CC-CV generators, and automated positioning systems. With over 22,600 heavy-duty installations operating globally, our engineering team manufactures complete welding power trains—from customized inverter driver boards to automated column & boom manipulator systems. This technical synthesis addresses the critical operational requirements of Moscow-based fabricators seeking high Information Gain, verified GOST/NAKS compatibility, and continuous 100% duty cycle throughput.
Technical Gain Insight: Heavy structural fabrication in regional Moscow conditions demands power sources capable of handling ±15% primary line voltage fluctuations while preserving arc stiffness down to sub-zero ambient temperatures (-40°C). Conventional transformer-rectifiers suffer severe thermal decay, whereas fast-switching IGBT inverter topologies maintain stable droplet transfer and precise heat input control.
Heavy plate joining requires specialized equipment configurations depending on the ultimate service environment of the weldment. Below are four key industrial sectors in Moscow and surrounding fabrication hubs (such as Podolsk, Kolomna, and Elektrostal) utilizing automated and inverter-driven joining systems:
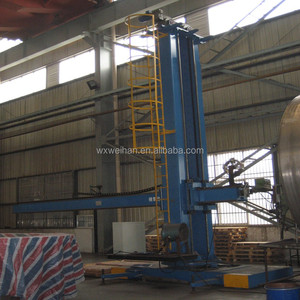
Moscow’s rapid transport expansion—including major highway bypasses, rail overpasses, and high-rise commercial steel frames—utilizes thick low-alloy structural steels such as 09G2S and 15HSND. Fabricating box girders and I-beams requires continuous longitudinal fillet and butt welding. Deploying Automatic Column & Boom systems paired with Heavy-Duty Submerged Arc Welding (SAW) power sources delivers deep penetration, smooth bead profiles, and zero-spatter welds that meet rigorous ultrasonic testing (UT) and radiographic inspection (RT) criteria.
Process equipment manufacturing for Moscow chemical, petrochemical, and power generation facilities demands zero-defect longitudinal and circumferential shell seams. Utilizing multi-process CC-CV inverter power units (like the APS Endeavour series) integrated with self-aligning welding rotators ensures consistent root pass execution via TIG/MIG followed by rapid fill passes via tandem SAW. Precision control of heat input mitigates grain growth in the Heat-Affected Zone (HAZ), preserving low-temperature Charpy V-notch impact toughness.
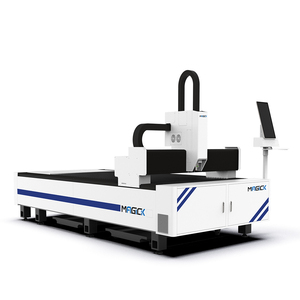
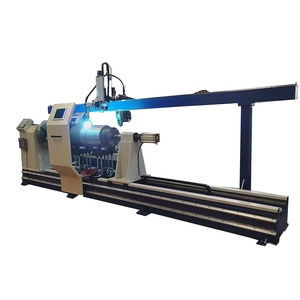
Fabrication yards building specialized piping spools for district heating networks and oil & gas transport require high-speed profile cutting and specialized cladding. Using CNC Pipe Profile Cutting Machines alongside CNC Control Pipe Cylinder TIG Overlay Hardfacing Machines allows Moscow fabricators to apply corrosion-resistant alloy (CRA) overlays (such as Inconel or stainless steel) onto heavy carbon steel cylinders with minimal dilution rates.
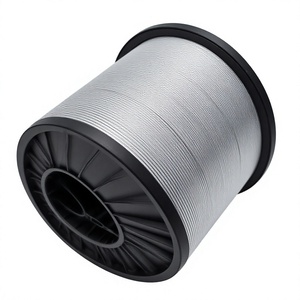
Heavy machinery maintenance yards require rapid metal removal and hardfacing capabilities. Inverter-based Carbon Arc Gouging (CAG) power units remove cracked or fatigued weld metal efficiently prior to re-welding. Paired with high-deposition Flux-Cored Arc Welding (FCAW) using E71T-1C wire, maintenance shops achieve rapid turnover with superior structural integrity.
Procurement teams in the Moscow region are rapidly upgrading traditional manufacturing infrastructure to meet stringent modern standards. Three key technical trends dominate current purchasing decisions:
Selecting the optimal joining process for heavy steel plate (20mm+) depends on deposition speed, joint geometry, site vs. shop conditions, and labor efficiency:
| Welding Process | Typical Plate Range | Deposition Rate (kg/hr) | Sub-Zero Toughness (-40°C) | Automation Readiness | Recommended APS Equipment |
|---|---|---|---|---|---|
| Submerged Arc (SAW) | 15mm - 120mm+ | 8.0 - 18.0+ | Excellent | Fully Automated (Column & Boom / Tractor) | Endeavour 1250 CCCV / SAW Series |
| Flux-Cored MIG (FCAW) | 6mm - 40mm | 3.5 - 7.5 | High (E71T-1C) | Semi-Auto / Robotic Station | APS Multiprocess GMAW / E71T-1C Wire |
| DC Pulse TIG (GTAW) | 1.5mm - 12mm (Root Pass) | 0.8 - 2.0 | Superior | Manual / Cold Wire CNC Overlay | Apollo DC Pulse TIG / CNC Cladding System |
| Inverter Stick (SMAW) | 3mm - 50mm (Site Repair) | 1.5 - 4.5 | Good (E7018/E6010) | Manual Portable | Genesis 400 Star / Stick Inverters |
Advanced Power Sources Limited (APS Welding) is an ISO 9001:2015 certified manufacturer headquartered in Valsad, Gujarat, India. Unlike trading intermediaries, APS designs, builds, and tests all inverter power boards, transformers, sheet metal enclosures, and control firmware in-house across our 20,000+ sq. m manufacturing facilities.
Our dedicated electronics R&D division designs proprietary IGBT driver cards engineered with dust-proof, moisture-resistant encapsulation to survive dusty fabrication bays and high ambient humidity or freezing outdoor operations.
Every industrial welding machine produced undergoes full-load heat run testing in a 40°C thermal chamber at 100% duty cycle rating prior to international seaworthy packing and dispatch.
APS provides integrated solutions: pairing power sources directly with heavy-duty positioners (up to 10,000 kg capacity), rotators, travel carriages, and CNC plasma gantry cutters under one unified warranty.
Answers to common technical, logistics, standards, and operational questions from Russian engineering procurement specialists.
APS industrial power sources are manufactured under ISO 9001:2015 quality management guidelines and comply with international IEC 60974-1 safety and performance standards. For Eurasian Customs Union (EAC) market entry, full technical passports, electrical safety documentation, and declaration certificates are provided to facilitate smooth NAKS procedure qualification and jobsite commissioning across Moscow industrial zones.
Yes. Heavy-duty APS stick (SMAW), TIG, and SAW machines can be specified with winterized thermal packages, low-temperature silicon cabling, and insulated printed circuit board (PCB) coatings. This prevents condensation-induced short circuits during rapid temperature transitions between indoor heated bays and sub-zero outdoor staging areas.
APS industrial units are standardly configured for 380V / 400V / 415V, 3-Phase, 50Hz electrical supply. The integrated IGBT inverter control module tolerates line voltage variations of up to ±15%, making them resilient against voltage dips common in heavy industrial parks operating large overhead cranes or induction heaters.
For 09G2S low-alloy steel plate fabrication, APS recommends using our Flux Cored Carbon Steel Wire E71T-1C (1.2mm or 1.6mm) paired with an APS Multiprocess CC-CV power source using CO2 or Ar/CO2 shielding gas. For plates thicker than 25mm, automated SAW using high-manganese wire and basic flux is recommended to ensure Charpy V-Notch impact toughness down to -40°C.
Standard heavy machinery and power source orders ship via multimodal sea-rail or direct container freight routes connecting major Indian ports (Mundra/NHAVA SHEVA) directly to Russian logistics hubs (St. Petersburg or Novorossiysk) with rail transfer to Moscow container terminals (e.g., Vorsino/Vostochny). Typical transit times range from 25 to 35 days, with full export seaworthy timber crates and anti-corrosion VCI wrapping included.
APS maintains comprehensive spare parts kits—including main IGBT modules, control cards, cooling fan assemblies, wire feed rollers, and torch consumables—packaged with every export consignment. Technical support is available via direct video engineering sessions, online schematics, and remote diagnostic guidance via our digital technical support line.
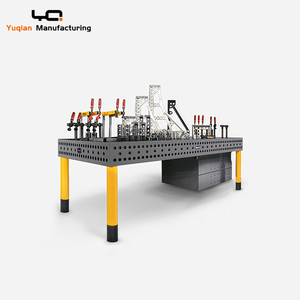
Absolutely. APS specializes in retrofitting and expanding shop capabilities. By combining existing shell fabrication rollers with an APS Column and Boom manipulator system, motorized 3D welding tables, and an Endeavour 1250 SAW power source, fabricators can convert manual stick/MIG processes into an automated high-deposition welding cell with minimal downtime.
Consult with our application engineering team today to receive a complete technical package, process ROI comparison, and detailed export quotation tailored for your Moscow jobsite requirements.
Send an Inquiry