Slovakia has established itself as one of Central Europe's most concentrated industrial and manufacturing powerhouse hubs. Driven by world-class automotive production centers in Bratislava, Trnava, Nitra, and Žilina, along with expanding biopharmaceutical complexes in Hlohovec and heavy chemical/refinery operations in Slovnaft Bratislava, the requirement for flawless joinery in high-purity and high-pressure fluid lines is paramount. Manual TIG (GTAW) welding often struggles to guarantee 100% X-ray quality consistency across thousands of repetitive structural joints, cleanroom tubing, and thick-walled pressure vessels under demanding EN ISO standards.
As a global OEM manufacturer of advanced IGBT inverter power sources and automated orbital welding systems, our enterprise delivers fully integrated, custom-engineered orbital welding heads, closed-loop micro-arc controllers, and intelligent wire feed units. This guide provides an in-depth analysis of high-gain information, application scenarios across Slovak industrial clusters, local technical trends, and procurement strategies engineered to optimize compliance with European Pressure Equipment Directive (PED 2014/68/EU), ASME Section IX, and EN ISO 15614-1 certifications.
Explore our specialized heavy industrial machinery, plasma cutting systems, automated surfacing, and consumable welding wires supplied for OEM integrations serving Slovak industrial contractors.
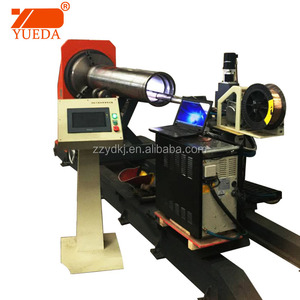
Orbital TIG (GTAW) welding represents the gold standard in joining circular profile tubes and pipes, where the arc rotates mechanically through 360 degrees around a static workpiece. In high-purity applications, such as pharmaceutical water-for-injection (WFI) lines or semiconductor gas delivery systems, any minor variation in root penetration or oxide discoloration can create micro-crevices susceptible to bacterial colonization or corrosion. Our custom OEM orbital welding architectures address these challenges through precise hardware-software integration:
Core OEM Advantage: Proprietary closed-loop micro-arc pulse synchronization maintains arc voltage stability within ±0.1V, preventing tungsten contamination and ensuring uniform heat input across 1G, 2G, 5G, and 6G position configurations.
For thin-walled stainless steel (SS316L, Hastelloy, Titanium) tubing ranging from 3.17 mm (1/8 inch) to 168.3 mm (6 inches) outer diameter, enclosed rotor heads flood the entire weld zone with inert gas (typically 99.999% pure Argon or Argon/Hydrogen mixtures). This completely prevents oxidation and eliminates the need for post-weld chemical pickling. Conversely, open-frame orbital heads equipped with Automatic Arc Voltage Control (AVC) and motorized wire feed units are engineered for thick-walled carbon steel and duplex pipe spools used in energy and oil & gas sectors across Central Europe.
Every orbital power supply engineered at our manufacturing site features high-frequency IGBT inverter control modules designed to withstand power grid fluctuations (400V ±15%, 50/60 Hz). Integrated with our proprietary WeldVisor IoT platform, every weld parameter—current pulsing, rotation speed, wire feed rate, and backing gas pressure—is recorded in real-time. This provides complete digital traceability compliant with EN ISO 3834-2 quality requirements.
| Technical Specification | Closed-Head Orbital TIG (Tube) | Open-Head Orbital TIG (Heavy Pipe) | Custom Tube-to-Tubesheet Head |
|---|---|---|---|
| Outer Diameter Range | 3.17 mm – 168.3 mm (0.125" – 6.625") | 25.4 mm – 1016 mm (1.0" – 40.0") | 10 mm – 80 mm ID (Heat Exchangers) |
| Wall Thickness Capability | 0.5 mm – 3.5 mm (Single Pass) | 3.0 mm – 50.0 mm (Multi-pass filler) | 1.0 mm – 4.0 mm (Flush/Recessed) |
| Cooling Mechanism | Liquid Cooled / High-Duty Cycle | Heavy Dual-Circuit Liquid Cooled | Integrated Liquid Cooling Jacket |
| Typical Materials | 316L, 304L, Titanium, Inconel | Carbon Steel, P91, Duplex SS | Stainless Steel, Copper-Nickel, Titanium |
| Slovakia Target Sector | Pharma, Biotech, EV Battery Lines | Slovnaft Refinery, Power Plants | Chemical & Nuclear Exchangers |
Understanding the unique regional industrial distribution of Slovakia is essential for deploying custom orbital welding systems. Our OEM engineering services adapt clamp collets, torch angles, and firmware interfaces to match regional factory specifications.
Slovakia leads global automotive production per capita, housing mega-assembly plants for Volkswagen, Stellantis, Kia, Jaguar Land Rover, and upcoming Volvo EV facilities. Orbital welding systems are deployed extensively for:
Slovakia’s expanding pharmaceutical sector requires strict adherence to EHEDG hygienic guidelines and ASME BPE standards. Custom orbital systems provide zero-dead-leg welds on process piping, purified water loops, and clean steam distributions, ensuring micro-roughness values Ra < 0.38 µm.
In thermal and nuclear power plants such as Mochovce NPP, as well as refining facilities along the Danube, heavy-duty open-head orbital welding systems perform multi-pass root and cap passes on high-alloy steam pipes under strict non-destructive testing (NDT) criteria including X-ray radiography and ultrasonic inspection.
Slovak fabricators face an aging demographic of certified manual TIG welders. Transitioning to automated OEM orbital systems enables one operator to manage multiple welding heads, increasing output by 300% while eliminating human error.
Tier-1 automotive suppliers in Slovakia require full digital batch traceability. Modern orbital controllers output digital weld logs via OPC-UA protocols directly to factory MES (Manufacturing Execution Systems).
Slovakia’s strategic placement along Central European gas transit routes requires upgrading high-pressure hydrogen-blend pipelines. Orbital TIG welding ensures embrittlement-resistant, zero-leakage pipeline joints.
Modern job sites demand lightweight, portable orbital power sources that can easily operate inside tight pipe racks and modular skid construction yards throughout Eastern and Western Slovakia.
As an ISO 9001:2015 certified manufacturer with over 20 years of in-house design and production heritage, our factory operates a dedicated 22,000+ sqm engineering center. Unlike traders or local brokers, we build the core electronics, high-frequency arc ignition boards, closed-chamber mechanical housings, and software algorithms completely in-house.
We own the complete intellectual property of our IGBT power inverter circuitry and digital controllers, enabling rapid OEM hardware/software customization for Slovak clients.
From specialized collets for non-standard metric/imperial tube dimensions to localized Slovakian/English touchscreen HMI interfaces, we adapt systems to your exact workflow.
With over 22,600 machines deployed worldwide across 50+ countries, we support buyers in Slovakia with comprehensive application guidance, site commission assistance, and fast spare-part dispatches.
Technical and commercial answers tailored for engineering managers, procurement officers, and plant operators in Slovakia.
Yes. All power sources and orbital heads supplied to the Slovakian market carry full CE certification and comply with EMC Directive 2014/30/EU and Low Voltage Directive 2014/35/EU. Weld procedures generated by our equipment routinely meet EN ISO 15614-1 and EN ISO 5817 Level B acceptance criteria required under the Pressure Equipment Directive (PED 2014/68/EU).
Our industrial power sources feature wide input voltage tolerance (3-phase 400V ±15%, 50 Hz). Internal voltage stabilization circuits protect sensitive microprocessor controls against voltage sags and spikes commonly encountered when operating on diesel generators or heavy industrial grids in remote installation sites.
To prevent internal root oxidation in stainless steel and titanium tubes, our closed-loop orbital controllers integrate digital gas flow meters and allow direct connection to residual oxygen analyzers. The controller blocks arc ignition until purge oxygen levels drop below a pre-programmed threshold (typically < 10 PPM to < 50 PPM depending on WPS requirements).
We supply custom-machined aluminum/titanium collet sets for non-standard tube geometries, micro-welding heads for compact spatial clearances (< 40 mm radial clearance), and specialized software programming for automated multi-pass schedules. OEM branding and localized interface languages can also be provided.
Standard orbital power supplies and standard closed-head systems are maintained in stock with export dispatch times within 10–15 business days. Custom OEM heads and collet assemblies require 3 to 4 weeks for precision CNC manufacturing and full load testing. Critical consumables (tungsten electrodes, collets, gas lenses, liquid-cooling jackets) are dispatched via air express to reach Slovak locations within 3–5 business days.