
Precision-engineered automated surfacing systems designed to maximize asset lifecycle, minimize component wear, and deliver exceptional metallurgical bonding in extreme operating environments.
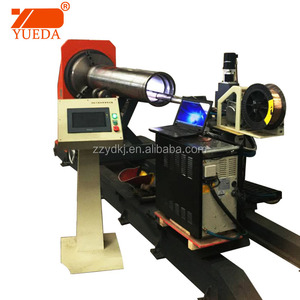
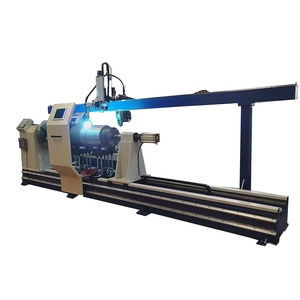
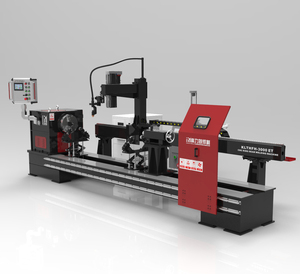
Kuwait's industrial economy—propelled by major oil exploration projects across the Sabriya, Greater Burgan, and Ratqa fields, alongside massive refinery expansions at Mina Al-Ahmadi, Mina Abdullah, and Al-Zour—operates under some of the most unforgiving mechanical and environmental stresses globally. Mechanical equipment, drill strings, slurry pumps, valve seats, catalyst piping, and heat exchangers are continuously exposed to severe abrasive quartz sand, corrosive hydrogen sulfide ($H_2S$), high thermal loads, and extreme operational pressures.
Unplanned downtime in Kuwaiti petrochemical and refining processing units carries exorbitant financial costs. To counteract rapid metal degradation, leading engineering, procurement, and construction (EPC) contractors and maintenance operators across Kuwait are shifting from traditional component replacement to advanced automated hardfacing and cladding overlay technology. By applying high-performance alloys—such as Stellite, Inconel 625, Monel 400, Hastelloy, and Chromium Carbide / Tungsten Carbide composites—onto low-alloy carbon steel substrate materials, operators achieve superior surface properties while maintaining core structural ductility.
As China’s premier manufacturer and exporter of heavy-duty industrial hardfacing systems, our company bridges cutting-edge inverter power topology, micro-gap CNC motion controls, and intelligent arc waveform management to deliver automated overlay equipment tailored specifically for Kuwait’s rigorous industrial standards (including KOC and KNPC technical compliance protocols).
Built from the circuit board up to withstand continuous 100% duty-cycle operation in ambient desert temperatures up to 55°C.
Proprietary inverter power modules deliver instant dynamic response, ultra-stable arc ignition, minimal spatter generation, and high electrical efficiency even during severe input grid fluctuations.
Closed-loop Automatic Voltage Control maintains precise arc gap dimensions across irregular workpiece contours, preventing burn-through and maintaining precise dilution ratios below 5%.
Integrated real-time parameter tracking logs voltage, current, travel speed, heat input, and arc-on time, providing full digital traceability required for oilfield certification audits.
Modular architectural design supports Plasma Transferred Arc (PTA), Submerged Arc Welding (SAW), Open-Arc FCAW, Cold-Wire TIG, and Precision Fiber Laser cladding on a single CNC platform.
Heavy-duty copper heat-exchangers and high-flow liquid cooling systems ensure uninterrupted 24/7 continuous production cycles in harsh Middle Eastern climates.
Pre-programmed parameter libraries for ASME IX, API 6A, and NACE MR0175 compliant procedure qualification records (PQR), ensuring rapid client sign-off.
In hardfacing and corrosion-resistant cladding applications, dilution control is the single most critical quality indicator. Dilution refers to the percentage of base metal melted and mixed into the weld deposit overlay layer. High dilution dilutes the chemical composition of high-alloy filler metals, reducing hardness, corrosion resistance, and thermal fatigue endurance.
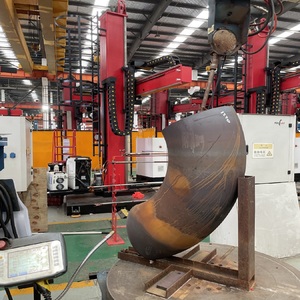
For instance, when depositing Inconel 625 (UNS N06625) onto low-alloy steel valve bodies or pipe spools for Kuwait's offshore sour gas projects, international specifications mandate an iron content below 5% in the first layer. Achieving this via manual SMAW or GMAW requires multiple weld passes, drastically increasing labor, filler wire consumption, and gas usage. Our automated Vertical Pipe Cladding and CNC TIG Overlay Systems employ synchronized hot-wire TIG pulse control, keeping iron dilution under 4% in a single layer at significantly higher deposition rates.
Selecting the optimal hardfacing technology based on component geometry, deposition rate, dilution limits, and metallurgical targets.
| Surfacing Technology | Deposition Rate (kg/h) | Typical Dilution (%) | Min Overlay Thickness | Primary Application in Kuwait | Key Advantage |
|---|---|---|---|---|---|
| Gantry Open-Arc FCAW | 8.0 – 18.0 | 15% – 25% | 3.0 mm | Wear Plates, Chutes, Cement Hammers | Ultra-high productivity for large flat areas |
| Submerged Arc (SAW) Overlay | 6.0 – 14.0 | 15% – 20% | 3.2 mm | Heavy Cylinders, Pressure Vessel Shells | Deep penetration, smooth aesthetic finish |
| Vertical / Horizontal TIG Cladding | 2.0 – 5.5 | < 5% | 1.6 mm | Valves, Flanges, Small Bore Pipe Inners | Zero defect rate, low dilution in 1 pass |
| Plasma Transferred Arc (PTA) | 3.0 – 9.0 | 5% – 10% | 1.0 mm | Pump Rotors, Valve Seats, Drill Stabilizers | Utilizes economical alloy powders |
| Fiber Laser Cladding | 1.0 – 4.0 | < 3% | 0.5 mm | Precision Tooling, Hydraulic Rod Repair | Minimal thermal distortion, exact precision |
Our automated hardfacing machines are deployed across Kuwait's primary industrial zones, including the Shuaiba Industrial Area, Sabriya Oilfield Services Center, and Al-Ahmadi Fabrication Yards. Below are specific localized operational scenarios where our equipment delivers measurable ROI:
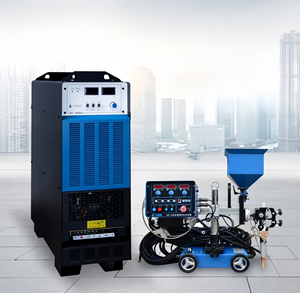
Drill stabilizers, reamers, and jar bodies suffer massive outer diameter wear when cutting through abrasive sandstone and carbonate strata. Utilizing our PTA Inverter Hardfacing Machine equipped with automated powder feeders, oilfield repair shops re-apply spherical tungsten carbide matrix overlays in spiral patterns, extending tool operational life by 300% to 500% compared to manual stick hardfacing.
Gate valves, globe valves, and pipe flanges operating in sour crude service require non-corrosive sealing surfaces. Our Vertical Automatic Pipe & Valve Cladding Machine automatically overlays Inconel 625 onto internal ring grooves, blind flanges, and valve seats with continuous step-over indexing, achieving zero-defect ultrasonic testing (UT) and radiographic testing (RT) results.
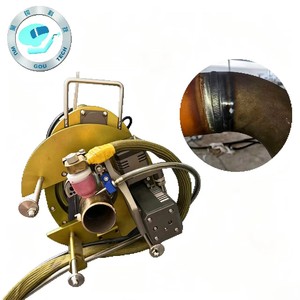
Corrosive chemical slurries quickly erode unlined small-bore elbow fittings and pipe spools. The Yueda Small Inner Pipe Automatic Surfacing Machine utilizes a slimline specialized torch arm designed to enter internal diameters as small as 50mm, laying down smooth continuous corrosion-resistant alloy beads up to 3 meters deep inside the pipe bore.
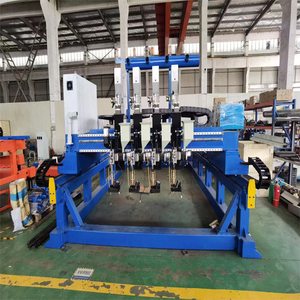
Cement raw meal chutes, clinker crushers, and coal pulverizer liners require continuous replacement. Our Gantry Type Quadruple Torch Wear Plate Machine deposits chromium carbide flux-cored wires onto raw steel plates simultaneously across four head assemblies, generating bimetallic wear plates at industrial scale with uniform crack-relief patterning.
Choosing an overseas OEM partner for heavy industrial equipment requires complete confidence in engineering design, manufacturing quality, component sourcing, and long-term technical support. Our state-of-the-art 22,000 m² manufacturing facility in China maintains total end-to-end control over the production process:
To ensure seamless integration and avoid operational mismatches when importing hardfacing machinery into Kuwait, procurement managers should evaluate the following key parameters:
Detailed technical responses addressing common procurement, operational, and metallurgical questions from Middle Eastern engineering teams.
Contact our application engineering team today for technical consultation, customized equipment proposals, and competitive factory-direct export pricing.