
Precision machinery, fiber laser profiling systems, automated TIG/MIG power sources, and specialized consumables essential for high-integrity pressure vessel fabrication in Central Asia.
Uzbekistan is undergoing a massive industrial transformation under the "Uzbekistan 2030" national strategy. As the country expands its processing capacity across gas chemistry, petroleum refining, mineral metallurgy, and thermal energy generation, the demand for high-integrity pressure vessels engineered to European Union (CE PED 2014/68/EU) and ASME Section VIII standards has reached an all-time high. Heavy industrial assets operating under high temperatures and cyclic pressure demands require strict metallurgy selection, precise automated welding processes, non-destructive testing (NDT), and comprehensive quality audit trails.
In accordance with the regulatory standards prescribed by the State Committee of the Republic of Uzbekistan for Industrial Safety (Sanoat Xavfsizligi), pressure equipment imported or installed within the republic must comply with unified safety codes while aligning with European CE directives or EAC TR CU 032/2013 standards. Our manufacturing facilities integrate advanced IGBT inverter welding systems, automated submerged arc welding (SAW) columns, and fiber laser cutting machines to deliver certified pressure vessels engineered for extreme operational environments.
Key Information Gain: Pressure vessels destined for Uzbekistan's gas-chemical hubs (e.g., Navoi, Bukhara, Kashkadarya) must account for high sour gas concentrations (H₂S and CO₂). Special metallurgy such as SA-516 Grade 70N (normalized), Austenitic Stainless Steels (304L/316L), and Nickel Alloys are deployed alongside mandatory 100% Radiographic Testing (RT) and post-weld heat treatment (PWHT).
| Design Standard | Pressure Range | Temperature Range | Metallurgy Options | Inspection Standards |
|---|---|---|---|---|
| CE PED 2014/68/EU (Module B+D) | Vacuum to 160 bar (16 MPa) | -40°C to +450°C | P265GH, P355GH, 1.4404 (316L), Duplex 2205 | EN 13445, 100% RT & UT, Hydrotest at 1.43x |
| ASME Sec VIII Div 1 & Div 2 | Up to 350 bar (35 MPa) | -50°C to +650°C | SA-516 Gr 70/60, SA-240 304L/316L, Hastelloy C276 | ASME Sec V NDT, Hydrotest at 1.3x - 1.5x |
| EAC TR CU 032/2013 / UzStandard | PN16 to PN250 | -50°C to +500°C | 09G2S, 12X18H10T, SA-516 Gr 70 N | GOST 5520, GOST 34347-2017, Hydrostatic Test |
Custom engineering solutions designed to meet the rigorous climate conditions, heavy thermal swings, and high-capacity demands of Uzbekistan's major industrial hubs.
Deployment of high-pressure gas separation vessels, amine absorption towers, and knock-out drums in Mubarak and Shurtan gas-chemical complexes. Designed with H₂S stress-corrosion cracking resistance and severe service wall thicknesses up to 80mm.
Autoclaves, ammonia synthesis storage tanks, and liquid nitric acid buffer vessels for Navoiyazot and Maxam-Chirchiq. Stainless steel cladding (SS316L) and orbital TIG tube-to-tubesheet joint integrity ensure leak-free continuous operation.
Heavy slurry expansion vessels, acid leaching tanks, and high-pressure steam digestors operating at Almalyk (AGMK) and Navoi (NGMK) gold and copper processing facilities. Built to withstand extreme abrasive and corrosive slurry flows.
Steam drums, deaerators, and high-pressure feedwater heaters for modernized thermal power plants (TPS) across Tashkent, Syrdarya, and Navoi regions. Certified for high-cycling thermal pressure stresses under European EN standards.
The industrial sector of Uzbekistan is experiencing exponential growth, driven by foreign direct investment (FDI), privatization programs, and massive infrastructure upgrades. Engineering procurement teams in Tashkent, Samarkand, and Fergana are transitioning away from obsolete legacy equipment toward automated, energy-efficient manufacturing machinery. Key trends reshaping procurement include:
Strategic Supply Chain Advantage: Operating direct logistics routes connecting our ISO-certified manufacturing base directly to major Uzbekistan industrial zones ensures shortened freight lead-times, complete documentation compliance, and direct factory-to-site engineering support.
Over 20 years of in-house design, automated machinery manufacturing, and global export expertise for critical industrial applications.
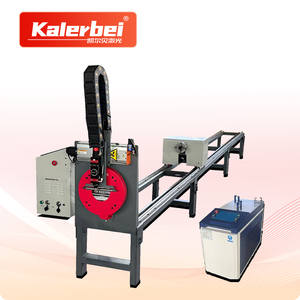
From custom IGBT inverter circuit boards to heavy-duty automated submerged arc welding (SAW) gantries, our internal engineering team handles complete hardware and software integration without reliance on external brokers.
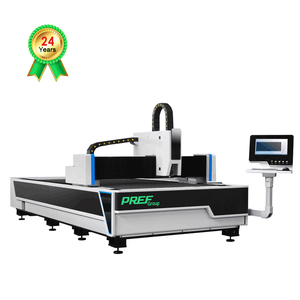
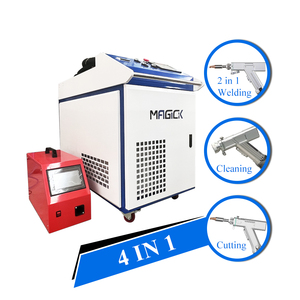
Equipped with high-precision fiber laser tube cutters and 30mm heavy-plate CNC plasma cutting tables, ensuring precise edge preparation, minimal heat-affected zones (HAZ), and perfect beveling for deep-penetration weld seams.
Every vessel and welded assembly undergoes rigorous quality assurance including Ultrasonic Testing (UT), Radiographic Testing (RT), Hydrostatic Pressure Testing up to 1.5x design pressure, and full material traceability (MTC EN 10204 3.1/3.2).
Direct technical and commercial answers regarding certification, environmental adaptation, logistics, and after-sales support.
Yes. Our pressure vessels are manufactured in compliance with CE PED (2014/68/EU) and ASME Section VIII directives. We provide full technical passports, material test certificates (MTC), non-destructive testing (NDT) reports, and structural calculations required for registration with Sanoat Xavfsizligi (State Industrial Safety Committee of Uzbekistan) and UzStandard certification bodies.
Central Asia experiences severe ambient temperature shifts, ranging from sub-zero winter temperatures (-30°C) to intense summer heat (+45°C). Our industrial equipment and power electronics feature heavy-duty industrial cooling systems, tropicalized PCB coating, high-duty-cycle IGBT inverters, and climate-tested seals designed specifically for continuous outdoor operation in desert and steppe environments.
Absolutely. We supply a complete range of certified consumables (such as ER308-GS gasless flux-cored wire, specialized TIG wire feeders, and laser optics) alongside comprehensive wearing parts kits. Fast-track logistics via direct rail and highway transit corridors ensure spare parts reach Tashkent, Navoi, or Bukhara within minimal downtime windows.
Our power sources, CNC laser cutters, and automatic band saw blade welding machines can be customized to match local Uzbekistan industrial power grids, including standard 380V / 400V / 415V three-phase supply at 50Hz, with wide input voltage tolerance (+/- 15%) to accommodate remote site generator supply fluctuations.
Standard catalog equipment and welding machines are available for immediate export dispatch within 10 to 15 days. Custom engineered pressure vessels, columns, or automated SAW gantries typically require 6 to 12 weeks depending on vessel shell thickness, metallurgy procurement (e.g., Clad SA-516 / SS316L), and post-weld heat treatment (PWHT) scope.
Consult directly with our senior application engineers to review your project drawings, material specifications, and regulatory requirements for Uzbekistan and global markets.
Get a Quote