
Germany’s industrial sector, driven by stringent DIN EN ISO 3834-2 standardisation and the relentless push toward Industrie 4.0, requires welding automation systems that deliver absolute repeatability, zero metallurgical defects, and seamless integration with decentralized PLC environments (such as Siemens S7-1500 and Beckhoff TwinCAT). As a specialized manufacturer and global exporter of high-duty industrial power sources and multi-axis automated positioning units, our enterprise engineered solutions specifically bridge the cost-efficiency of advanced IGBT inverter architectures with the rigorous precision demanded by German heavy engineering, automotive OEMs, pressure vessel fabricators, and structural steel works.
In modern industrial fabrication across regions such as Baden-Württemberg, North Rhine-Westphalia (NRW), and Bavaria, welding is no longer treated as an isolated manual task. It is a data-driven, continuous thermal joining process requiring real-time closed-loop parameter control, programmable pulse shaping, and low thermal distortion setups. Whether implementing heavy-section Submerged Arc Welding (SAW) on structural H-beams or deploying high-frequency micro-TIG cold wire feeders for thin-walled stainless steel pipes, our automated systems enable European plants to maximize arc-on time, achieve consistent weld bead geometry, and substantially lower energy consumption per kilogram of deposited metal.
Advanced IGBT module switching rates up to 20 kHz ensure instantaneous dynamic response, minimal arc spatter, and exact heat input management essential for high-yield metallurgy.
Equipped with integrated IoT monitoring modules, transmitting real-time arc-on hours, operational current/voltage, and thermal diagnostic alerts via PROFINET and OPC UA.
Full adherence to European Low Voltage Directive 2014/35/EU, EMC Directive 2014/30/EU, and EN 60974-1 arc welding equipment safety standards.
To achieve sustainable Information Gain in industrial export markets, machinery must be evaluated within the specific operational context of the local supply chain. In Germany, distinct industrial clusters demand tailored automated welding setups:
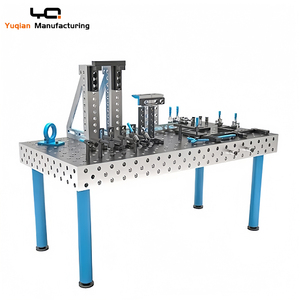
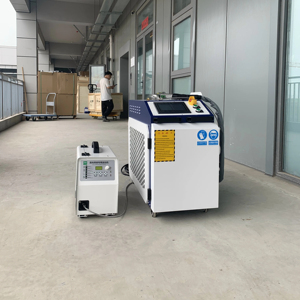
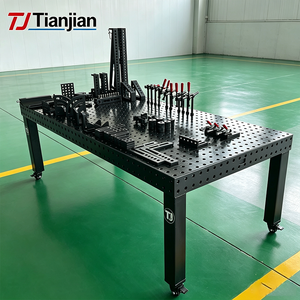
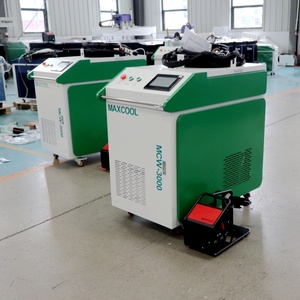
The transition toward electric vehicle (EV) lightweighting requires low-heat joining of dissimilar metals, aluminum structural extrusions, and battery housing enclosures. Our 4-in-1 Handheld & Automated Fiber Laser Welding Machines (1000W to 3000W) integrated with multi-axis positioning tables provide localized precision, narrow heat-affected zones (HAZ), and deep weld penetration without mechanical post-processing. Combined with high-durability D16 and D28 3D modular welding tables, tier-1 suppliers can reconfigure clamping fixtures rapidly for short-run prototype batches or high-volume automated lines.
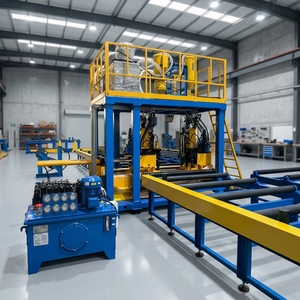
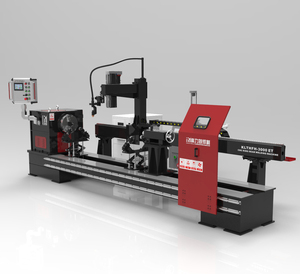
In the heavy industrial belt of the Ruhr Valley and northern wind turbine manufacturing zones, structural integrity cannot be compromised. The Pioneer CNC Horizontal H-Beam Automatic Submerged Arc Welding System (SAW) provides continuous multi-pass longitudinal fillet welds on thick carbon steel plates. Utilizing heavy-duty CC/CV multi-process power sources rated up to 1250A at 100% duty cycle, these systems provide deep penetration and smooth slag removal, passing rigorous ultrasonic (UT) and radiographic (RT) weld testing under AD 2000-Merkblatt standards.
For chemical process plants, valve manufacturing, and forging die maintenance, component surface degradation must be mitigated through high-alloy metal deposition. Our Plasma Transferred Arc (PTA) Inverter Cladding Systems allow precision powder deposition (Stellite, Inconel, Tungsten Carbide) with extremely low dilution rates (<5%). This technology guarantees superior abrasion and corrosion resistance for high-stress industrial components operating under European environmental mandates.
Selecting the optimal automated joining setup requires evaluating metallurgical parameters, duty cycles, electrical efficiency, and workflow layout. Below is an engineering comparison matrix designed for German procurement directors and welding engineers (Schweissaufsicht / EWE):
| System Category | Primary Process | Target Materials | Nominal Power / Current | Typical German Application | Key Compliance / Interface |
|---|---|---|---|---|---|
| Pioneer CNC Horizontal SAW | Submerged Arc (SAW / GMAW) | S235JR to S690QL Heavy Steel | 1000A - 1250A @ 100% Duty | H-Beam, Girders, Wind Towers | DIN EN ISO 15614-1 / CNC G-Code |
| Handheld/Auto Fiber Laser (4-in-1) | Fiber Laser (Wobble head) | Stainless Steel, Aluminum, Galvanized | 1000W - 3000W CW | EV Chassis, Enclosures, Sheet Metal | CE / Class 4 Laser Safety Enclosure |
| PTA Inverter Cladding Machine | Plasma Transferred Arc | Stellite, Inconel, Cobalt Alloys | 300A - 500A Micro-Pulse | Valve Seats, Extruder Screws, Dies | AD 2000 / Precision Powder Feeder |
| Automated TIG Wire Feeder System | GTAW Cold / Hot Wire | High-purity SS 316L, Titanium | 250A - 400A Pulse DC TIG | Pharma Piping, Heat Exchangers | DIN EN 10217-7 / Digital Stepper Encoder |
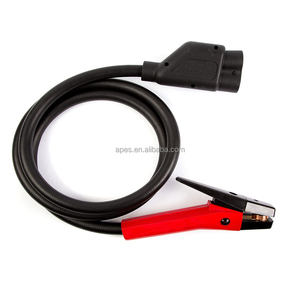
| Carbon Arc Gouging Heavy Unit | Air Carbon Arc (CAG) | Cast Iron, Alloyed Steels | 600A - 1000A Continuous | Ship Repair, Weld Root Defect Removal | EN 60974-1 / High-CFM Compressed Air |
As energy costs remain a critical operational metric across the European Union, German manufacturers are systematically replacing legacy transformer-based welding units with ultra-efficient inverter power sources. Modern IGBT Inverter Topology operates at power factors exceeding 0.93 to 0.95, significantly reducing active power draw and total kVA demand from the grid.
Furthermore, under the framework of European green manufacturing mandates, minimizing material waste during joint preparation is essential. Systems such as our integrated carbon arc gouging torches and PTA cladding setups enable circular-economy re-manufacturing of worn tooling rather than component replacement. On the digital front, our WeldVisor IoT architecture acts as a central telemetry hub. By logging amperage curve micro-variations, shielding gas pressure stability, and arc-on ratios, quality assurance teams can export complete welding logs directly to their Enterprise Resource Planning (ERP) systems, satisfying DIN EN ISO 14731 welding coordination auditing requirements.
Building on over two decades of dedicated power source design and mechanical automation engineering, our manufacturing enterprise delivers direct manufacturer accountability without middleman delays:
Unlike assemblers relying on off-the-shelf third-party boards, our core electronic control boards, pulse-timing firmware, and inverter gate drivers are engineered in-house under strict ISO 9001:2015 controls, allowing tailored custom firmware modifications for complex automated cell integrations.
With tens of thousands of power units operating globally, we maintain standardized export packaging, full CE certification compliance dossiers, comprehensive English and German technical manuals, and rapid spare-parts availability to guarantee minimal site downtime.
Partner with an established manufacturer of industrial automated welding systems, heavy-duty IGBT power sources, and precision 3D positioning equipment. Request detailed engineering specifications, CAD models, or a competitive export quotation today.
Inquire Now