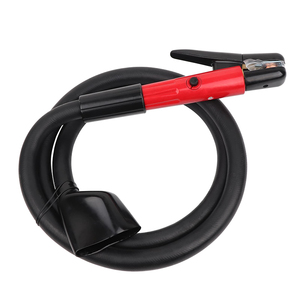
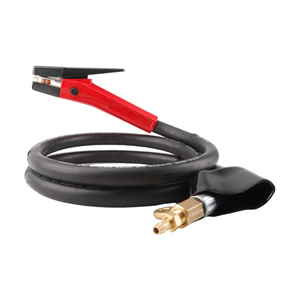
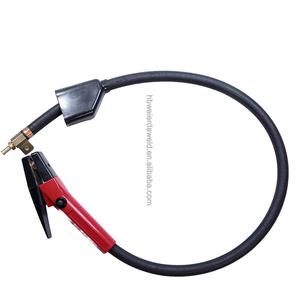
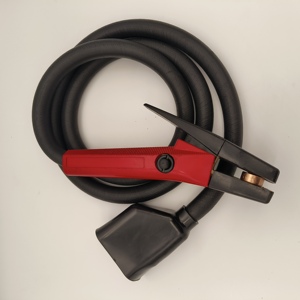
Heavy-Duty Air Carbon Arc Gouging Guns, Replacement Torches, and Thermal Cutting Hardware Engineered for Extreme Amp Duty Cycles in South Korea Industrial Applications.
Analyzing the Process Mechanics, Metallurgical Benefits, and Equipment Requirements for High-Duty Metal Removal in Korean Heavy Industry
Air Carbon Arc Gouging (CAG / Arc Air) represents one of the most vital thermal cutting and metal removal processes across South Korea’s industrial belt. The process functions by striking an intense electric arc between the tip of a copper-coated graphite/carbon electrode and the metal workpiece. As the local base metal melts instantaneously under temperatures exceeding 3,500°C to 5,000°C, high-velocity streams of compressed air (typically 80 to 100 PSI) passing through targeted orifices in the torch head blast the liquid metal away, creating a clean, uniform U-shaped groove.
Compared to mechanical grinding, plasma cutting, or oxy-fuel washing, air carbon arc gouging yields metal removal rates up to five times faster, making it an indispensable tool for heavy metal fabrication, weld defect removal, root pass cleaning, and plate beveling. In South Korea—home to world-leading shipbuilding conglomerates, nuclear pressure vessel fabricators, offshore structure builders, and heavy machinery giants—procuring industrial-grade, heavy-duty air gouging torches like the K3000 (600A-800A), K4000 (1000A), and K5/K5000 (1250A) is a critical operational priority.
As a premier direct manufacturer and OEM supplier, our factory provides precision-engineered carbon arc gouging torches tailored specifically to meet the high thermal loads, strict safety parameters, and ergonomic requirements demanded by Korean engineers and procurement managers.
Deploying Heavy-Duty Gouging Systems to Address Specific Metal Removal Challenges in Ulsan, Geoje, Changwon, Pohang, and Incheon
At mega-yards operated by HD Hyundai Heavy Industries, Samsung Heavy Industries, and Hanwha Ocean, K4000 (1000A) and K5 (1250A) gouging guns are deployed continuously for hull butt-joint back-gouging, deck plate joint preparation, and non-destructive examination (NDE) defect repair on thick EH36 and FH40 marine grade steel plates.
In heavy steel mills and foundry facilities around POSCO sites, heavy-duty 1000A-1250A gouging torches are utilized to wash away cast steel risers, ingot surface flaws, and slag encrustations. The forged monoblock brass bodies withstand continuous radiant heat without structural deformation.
Fabricators of armored defense vehicles, heavy excavators, and industrial presses rely on precision gouging with 3/8" (9.5mm) pointed and flat carbon electrodes to bevel high-tensile alloy steels, ensuring complete joint penetration (CJP) during robotic submerged arc welding (SAW) operations.
Pressure vessel shops building reactors, heat exchangers, and storage spheres use stainless steel carbon gouging techniques. Torches equipped with 360-degree swivel cable connections allow operators to maneuver within narrow vessel interiors without hose twisting or air-flow constriction.
As South Korea expands offshore wind farm initiatives off the coasts of Ulsan and Jeollanam-do, gouging torches are essential for joint preparation on jacket foundations, monopiles, and transition pieces, working in demanding coastal humidity.
Busan port maintenance drydocks use flexible multi-amp torch packages for rapid replacement of worn hull plates, rudder stock repairs, and retrofitting eco-friendly scrubbers on container ships under tight turnaround schedules.
Key Operational, Technological, and Regulatory Factors Driving Equipment Selection in Korean Industrial Supply Chains
South Korea’s manufacturing landscape is undergoing a massive transformation. Driven by demographic shifts, strict safety legislation under KOSHA (Korea Occupational Safety and Health Agency), and high-tech shipbuilding demands (LNG/Ammonia carriers), procurement teams are upgrading to next-generation thermal cutting equipment.
Korean shipbuilders prioritize lightweight yet ultra-durable torch bodies (e.g. glass-filled phenolic insulating handles) that reduce wrist strain during 8-hour shifts while insulating up to 500°C radiant heat.
With rising energy costs in Korean industrial complexes, torches with optimized 4-hole orifice valve seats achieve maximum molten metal expulsion at lower CFM air pressure ratings.
Automatic arc air gouging heads mounted on motorized travel carriages or CNC gantries are replacing manual gouging for long linear seams in pressure vessel and tank manufacturing.
Comprehensive Parameter Comparison for Heavy-Duty Industrial Gouging Guns Supplied to Korea
| Torch Model Class | Amperage Range | Carbon Electrode Capacity | Air Pressure Needed | Air Consumption (CFM) | Cable Cable Assembly | Primary Korea Target Application |
|---|---|---|---|---|---|---|
| K3000 Series | 600A - 800A | Pointed: 5/32" to 3/8" (4-10mm) Flat: 3/8" x 5/32" |
80 PSI (5.6 kg/cm²) | 21 CFM (0.60 m³/min) | 7-Foot (2.1m) Heavy Rubber / 360° Swivel | Structural Steel, Medium Machinery, Light Root Pass Cleaning |
| K4000 / K4 Series | 1000A Continuous | Pointed: 5/32" to 1/2" (4-13mm) Flat: 5/8" x 3/16" |
80 - 100 PSI (5.6-7.0 kg/cm²) | 28 CFM (0.79 m³/min) | 7-Foot (2.1m) High-Flex Monocoil / Copper Cable | Shipbuilding Hull Butt Joints, Heavy Foundry Castings, Boiler Shops |
| K5 / K5000 Extreme | 1250A Heavy Duty | Pointed: 5/16" to 5/8" (8-16mm) Flat: 3/4" x 3/8" |
90 - 100 PSI (6.3-7.0 kg/cm²) | 33 CFM (0.93 m³/min) | Heavy Duty Monocoil Cable with Neoprene Boot Cover | Nuclear Pressure Vessels, Thick Riser Removal, Defense Plate Beveling |
| Automatic Gouging Head | 1200A - 1600A | Jointed Carbons: 5/16" to 3/4" (8-19mm) | 90 - 110 PSI | 35-40 CFM | Direct Machine Control Connector / Remote Control Unit | Automated Seam Gouging on Wind Towers, Tanks, Pipe Spools |
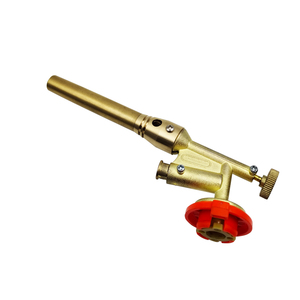
| Blow Torch Metal Series | 1300°C Flame Temp | Butane / Propane Gas Cartridge Fit | Self-Contained Gas Pressure | Variable Flow Valve | Direct Cylinder Lock Base | Auxiliary Preheat, Mold Heating, Field BBQ & Pipe Maintenance |
Why Tier-1 Korean Distributors and EPC Contractors Partner Directly with Our Manufacturing Plant
Unlike cheap die-cast zinc alternatives, our gouging torch heads feature high-grade forged copper/brass alloy monoblocks. This ensures superior electrical conductivity, minimal heat retention, and resistance to high-amperage arc melting.
Every single gouging torch produced in our ISO 9001:2015 certified factory undergoes rigorous 100% compressed air leak testing and high-amperage load verification before export packaging to Busan and Incheon ports.
We support full custom branding for Korean welding equipment suppliers, including laser engraving torch handles, custom color-coded insulation, localized user manuals (Korean/English), and retail box designs.
Addressing Common Inquiries Regarding Technical Standards, Logistics, Customs, and Operational Parameters
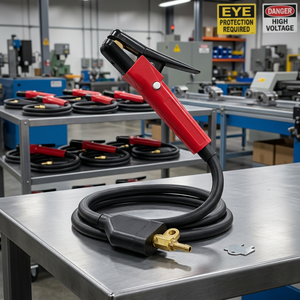
The standard K4000 (1000A rating) torch is designed to accept round carbon electrodes ranging from 5/32 inch (4.0mm) to 1/2 inch (13mm) in diameter. It also accommodates flat carbon gouging electrodes from 3/8 inch (9.5mm) up to 5/8 inch (16mm). The 360-degree rotating head allows operators to adjust carbon position easily for overhead or vertical gouging positions in shipbuilding yards.
For optimum performance and clean metal expulsion, the air compressor supply should maintain a clean air line pressure of 80 to 100 PSI (5.6 to 7.0 kg/cm²). The air delivery rate should be at least 28 CFM (0.79 m³/min) for 1000A K4000 torches, and up to 33 CFM for 1250A K5 torches. Inadequate air pressure results in sluggish metal removal, carbon contamination in the groove, and premature torch head overheating.
DCRP (DC Electrode Positive) connects the gouging torch to the positive terminal of the welding power source and the work clamp to the negative terminal. Under DCRP, approximately 70% of the arc heat is concentrated at the carbon tip, allowing rapid sublimation of the graphite and intense melting of the base metal. DC Straight Polarity (DCEN) is only used for specific carbon gouging applications on copper alloys.
Our manufacturing process complies strictly with international standards ISO 9001:2015 and IEC 60974-7 for arc welding equipment. High-grade insulating materials (glass-reinforced thermoset plastic) are utilized to prevent electrical shock and withstand high radiant heat, matching the safety guidelines set forth by KOSHA (Korea Occupational Safety and Health Agency).
For standard models (K3000, K4000, K5000), we maintain consistent factory inventory, enabling dispatch within 3 to 7 working days. Bulk custom OEM orders typically ship within 15 to 20 days. Shipments are dispatched via ocean freight directly to Busan Port or Incheon Port, or via express air freight (Incheon International Airport / ICN) for urgent shipyard maintenance shutdowns.
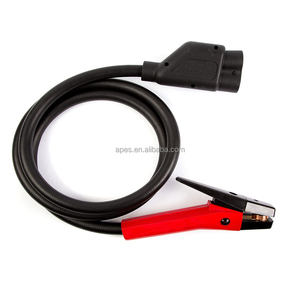
Yes. As a full-service manufacturer, we supply 100% interchangeable replacement spare parts including copper torch heads, upper jaw assemblies, lower insulators, air valves, lever assemblies, head insulators, and heavy-duty 360-degree swivel cable assemblies. Distributors in Korea can order complete replacement kits for easy field maintenance.
While plasma gouging offers lower smoke levels on thin metals, Air Carbon Arc Gouging remains the dominant choice for heavy structural steel and shipbuilding thick plates (>15mm). Carbon gouging requires significantly lower initial equipment investment, utilizes standard CC/CV DC welding power sources already present in Korean shipyards, and achieves much deeper metal removal rates in heavy plate root-gouging applications.
Absolutely. While standard cable assemblies are 7 feet (2.1 meters) long, we regularly produce custom length monocoil power/air cables (e.g., 3m, 5m, or 10m) covered in heavy-duty abrasion-resistant rubber or canvas protective boots to satisfy specific shipyard workflow demands in Ulsan and Geoje.
Request Technical Specifications, Wholesale Pricing, and Factory Direct OEM Catalog for the South Korean Market
Get a Quote