
Explore our ISO 9001:2015 certified engineering equipment, designed for tube-to-tubesheet joint integrity, structural fabrication, and high-precision metal processing.
In high-pressure heat exchangers, surface condensers, feedwater heaters, and chemical reactors, the tube-to-tubesheet connection represents the most critical mechanical boundary. A single microscopic breach under cyclic thermal stress can result in catastrophic cross-contamination of process fluids, costly emergency outages, and severe environmental liabilities.
As premier tube sheet welder suppliers & exporters, Advanced Power Sources Limited (APS Welding) delivers fully automated orbital GTAW (TIG) power sources and precision closed-loop welding heads. Engineered in compliance with ASME Section VIII Division 1 & 2, TEMA (Tubular Exchanger Manufacturers Association), and HEI (Heat Exchange Institute) standards, our machines provide repeatable, hermetically sealed structural and seal welds across diverse alloy matrix configurations.
Technical Precision Note: Automated pulse TIG tube sheet welding eliminates manual operator fatigue, ensuring consistent arc voltage control (AVC), uniform bead geometry, and precise heat input management to minimize heat-affected zone (HAZ) sensitization in austenitic stainless steels and duplex alloys.
Comparative analysis of orbital tube-to-tubesheet joining, heavy seam welding, and mechanized fabrication systems for global EPC contractors.
| Equipment Category | Primary Process | Target Metallurgy / Range | Duty Cycle & Precision | Automation Grade |
|---|---|---|---|---|
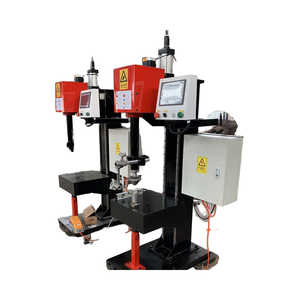
| Orbital Tube Sheet Welder | Pulse GTAW (DC TIG) with AVC | Stainless, Duplex, Titanium, Inconel (OD 12mm - 89mm) | 100% Continuous Duty @ IEC 60974-1 (40°C) | Fully Automated Closed-Loop CNC Control |
| Vertical Circumferential Welder | Multi-Process TIG / MIG Rotary | Carbon Steel, SS Cylinders & Pressure Vessels | 80% - 100% Duty Cycle with Servo Rotation | Programmable PLC Motorized Seam Tracking |
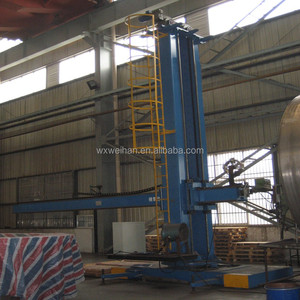
| Column & Boom Manipulator | Heavy SAW / MIG / TIG Integrated | Heavy Plate Shells, Tanks, Wind Towers (>50mm) | Continuous Heavy Duty Industrial Rating | Motorized Gantry / Column Travel Integration |
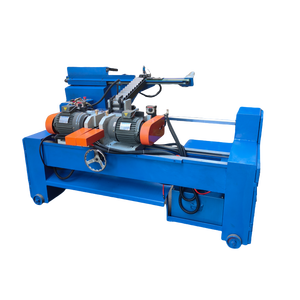
| Pipe Profile & Chamfering | Hydraulic Gear Beveling | Seamless & Welded Pipes (Schedule 40 - 160) | High-Speed Chamfering ±0.05mm Repeatability | Hydraulic Automatic Clamping & Feed |
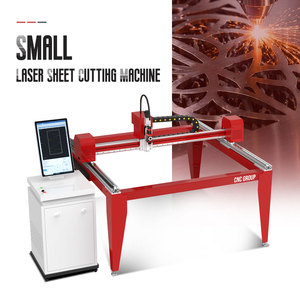
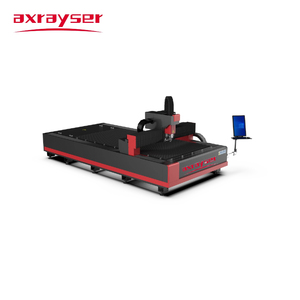
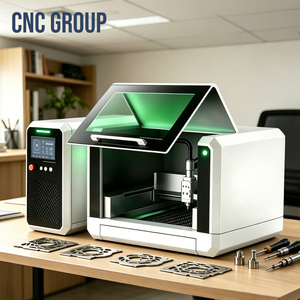
| Precision Fiber Laser Cutting | 1.5kW - 6kW Fiber Laser Beam | Brass, Carbon Steel, Stainless Sheet (0.5mm - 25mm) | Positioning Accuracy: ±0.03mm / m | CNC Automated Nesting & Cutting Worktable |
As global manufacturing shifts toward zero-defect mandates, digital traceability, and decarbonized energy production, procurement strategies for heat exchanger fabrication equipment are evolving rapidly.
Modern EPC buyers increasingly require real-time welding parameter logging—monitoring arc current, arc voltage, wire feed rate, and travel speed per joint. Smart power sources equipped with IoT systems (such as APS WeldVisor) allow quality control managers to verify heat input limits instantly, establishing digital quality passports for nuclear and subsea heat exchangers.
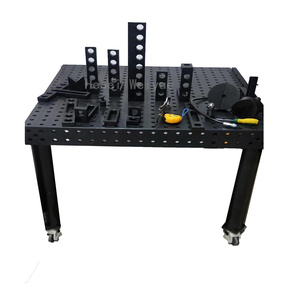
Procurement teams are moving away from standalone power supplies toward integrated robotic and mechanized workcells. Combining high-speed edge chamfering, 3D modular clamping positioners, column and boom manipulators, and automated GTAW/SAW heads under a unified control protocol reduces material handling overhead by up to 45% while eliminating alignment bottlenecks.
Legacy transformer-rectifier power sources are being phased out in favor of advanced IGBT inverter architectures. Switch frequencies exceeding 20 kHz deliver superior arc stability, ultra-fast dynamic response to surface irregularities, reduced electrical power consumption, and compact physical footprints suitable for tight workshop layouts.
Discover the engineering innovations driving next-generation thermal management equipment manufacturing.
In automated tube sheet welding, minor variations in tube protrusion height or sheet flatness can destabilize the tungsten arc gap. Modern orbital weld heads incorporate high-precision stepper motors linked to digital AVC feedback. The system continuously measures arc voltage thousands of times per second, dynamically adjusting torch height to maintain an exact arc distance throughout 360-degree rotation.
The growing adoption of super duplex stainless steel (e.g., UNS S32750), Hastelloy, and Grade 2 Titanium in desalination and petrochemical plants demands exact interpass thermal control. Pulsed TIG welding technology enables precise micro-joule heat input parameterization, preventing phase imbalance (austenite-ferrite ratio deterioration) and eliminating hot-cracking vulnerabilities during circumferential solidification.
Tube sheet welding integrity depends heavily on pre-weld joint fit-up. Utilizing high-power fiber laser sheet cutters and double-head hydraulic chamfering machines ensures zero-gap tube-to-hole clearance (typically within ±0.05mm). This level of mechanical accuracy prevents blow-through during autogenous seal welding and ensures full-penetration structural joints under helium leak testing.
For heavy wall tubes requiring filler wire addition, synchronized wire feeding is vital. Microprocessor-controlled wire feeders pulse the wire in perfect cadence with the peak welding current. The wire enters the leading edge of the molten pool precise millisecond intervals, avoiding tungsten contamination and delivering uniform wire deposition in all orbital positions (flat, vertical, and overhead).
Advanced Power Sources Limited (APS Welding) operates an ISO 9001:2015 certified manufacturing facility located in Old GIDC Gundlav, Valsad, Gujarat. Unlike equipment traders or white-label distributors, we engineer every critical component in-house—from proprietary IGBT inverter power printed circuit boards to precision orbital torch clamping mechanics.
Every machine dispatched from our facility undergoes rigorous multi-stage testing including electrical load bank testing, continuous thermal burn-in, high-voltage insulation tests, and actual arc testing on heavy-wall alloy specimens.
Overseas buyers receive comprehensive factory acceptance test (FAT) reports, operation manuals, electrical schematics, and direct access to senior service technicians.
Answers to essential technical and commercial questions for engineers, QC managers, and global sourcing specialists.
Automated orbital TIG (GTAW) welding provides precise, reproducible control over arc current, pulsed heat input, AVC gap distance, and rotation speed. Manual welding on a typical heat exchanger with thousands of tube joints leads to operator fatigue, inconsistent bead profile, burn-through risks, and high defect rates under hydrostatic or helium leak testing. Orbital systems deliver 100% joint repeatability, significantly reducing rework costs and ensuring compliance with ASME BPVC standards.
Our orbital tube-to-tubesheet heads support outer tube diameters ranging from 12 mm to 89 mm (0.5 inches to 3.5 inches). Compatible metallurgies include carbon steel, austenitic stainless steel (304L, 316L, 321), duplex and super duplex stainless steel (2205, 2507), nickel alloys (Inconel, Monel, Hastelloy), titanium, and copper-nickel alloys. Customized weld heads for non-standard tube geometry or tight pitch configurations are available upon request.
Industrial power sources manufactured by APS Welding are rated in strict accordance with IEC 60974-1 standards. Duty cycle is measured over a 10-minute cycle at a standard ambient temperature of 40°C. For example, a 100% duty cycle rating at specified amperage indicates that the power source can run continuously without thermal cutout under extreme tropical or heavy shop conditions.
Yes. In standard fabrication procedures, tubes are lightly tack-welded or mechanically expanded (roller expanded or hydraulically expanded) into the tubesheet bore prior to seal or structural welding. Our orbital heads feature specialized centering mandrel pneumatic clamps that align perfectly with the tube inside diameter (ID), securing the torch rigidly relative to the joint line.
International buyers should provide local grid parameters, including voltage (e.g., 380V, 415V, 440V, or 480V), phase (3-Phase standard for industrial systems), line frequency (50 Hz or 60 Hz), and site operating conditions (e.g., mains vs. generator supply). APS welding machines feature wide input voltage tolerance bands (±15%) to protect sensitive inverter electronics against voltage spikes and brownouts common at field construction sites.
APS Welding maintains a global support service model. We supply comprehensive recommended spare parts kits (including torch consumables, tungsten electrodes, control boards, drive rolls, and gas nozzles) with initial machine shipments. Our technical team offers online diagnostic assistance, video-guided commissioning support, and can dispatch field service engineers for site installation, FAT procedures, and operator training upon request.
Talk to our senior technical engineers today for customized tube sheet welding proposals, equipment recommendations, or factory visit scheduling.
Contact Us