
Explore our flagship heavy-duty welding platforms, orbital automation rigs, and industrial fabrication machinery available for white-label OEM/ODM distribution.
An authoritative technical analysis for procurement directors, welding engineers, and OEM brand managers evaluating high-frequency inverter technology for industrial manufacturing.
Modern Gas Tungsten Arc Welding (GTAW) demands absolute current stability and microsecond dynamic response. Conventional transformer-based welding sources suffer from thermal hysteresis, excessive power loss, and crude arc start control. Our proprietary IGBT Inverter In-House PCB Topology operates at switching frequencies ranging from 20 kHz up to 100 kHz. By rectifying three-phase AC mains into DC and pulsing it through high-speed Insulated Gate Bipolar Transistors (IGBTs), the primary transformer footprint is reduced by 70% while improving electrical efficiency beyond 88%.
This high-frequency conversion yields an instantaneous arc response. When tungsten touches the workpiece or high-frequency (HF) sparks bridge the gap, the digital control loop adjusts output current within 50 microseconds, virtually eliminating tungsten contamination and molten pool spatter.
Welding non-ferrous metals such as aluminum alloys (5000 and 6000 series) and magnesium requires overcoming tenacious surface oxide layers ($Al_2O_3$). Traditional sinusoidal AC TIG welders lack independent control over cleaning versus penetration. Our advanced ODM/OEM inverter platforms incorporate DSP-driven digital AC synthesis offering three customizable waveforms:
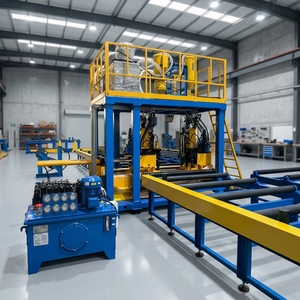
From manual pipe root pass systems to fully integrated orbital automatic TIG units, inspect our standardized platforms ready for white-label manufacturing and hardware adaptation.
| Model Category / Platform | Primary Process | Input Voltage Tolerance | Pulse Frequency Range | Rated Duty Cycle (40°C) | OEM Customization Scope |
|---|---|---|---|---|---|
| Apollo Series TIG 200AC/DC | AC/DC GTAW / MMA | 230V ± 15% 1-Phase | 0.5 Hz – 200 Hz Pulse | 60% @ 200A / 100% @ 155A | Custom Enclosure Color, Brand Interface, Memory Slots |
| Industrial Apollo TIG 315 P AC/DC | AC/DC GTAW / Pulse / Spot | 415V ± 15% 3-Phase | 0.5 Hz – 500 Hz High-Speed | 100% @ 250A / 60% @ 315A | Dual-Voltage Option, Digital CANbus Automation Interface |
| Endeavour Master TIG 400 DC | DC GTAW / Heavy MMA / Gouging | 380V – 480V 3-Phase | 0.1 Hz – 500 Hz DC Pulse | 100% @ 310A / 60% @ 400A | WeldVisor IoT Chipset Integration, Liquid Cooler Interlock |
| Orbital-Ready TIG 500 Automation | Automated GTAW / Cold Wire | 415V Continuous 3-Phase | 0.5 Hz – 1000 Hz Ultra-Pulse | 100% @ 400A Continuous | Robot Communication Protocols (EtherNet/IP, Profinet, Modbus) |
Designed for high-end aerospace, stainless tank, and aluminum structure fabrication. Fully configurable pulse width, pulse peak, balance control (15% - 50%), and background current parameters prevent burn-through on thin-gauge materials while maintaining arc stiffness.
Boost deposition rates by up to 60% over manual TIG rod feeding. Synchronized pulse feeding delivers wire directly into the molten pool in tandem with arc pulsing, eliminating operator fatigue and producing immaculate ripple bead appearances.
Unifying DC GTAW, SMAW (Stick cellulosic E6010 ready), GMAW (MIG), Submerged Arc (SAW), and Carbon Arc Gouging into a single robust power source. Perfect for heavy vessel fabrication and pipeline construction yards.
As global manufacturing shifts toward automation, stringent carbon audits, and IoT traceability, procurement teams must align with OEM suppliers offering forward-compatible power sources.
Procurement departments are moving away from isolated welding machines toward connected ecosystems. Modern QA/QC protocols in nuclear, pharmaceutical, and aerospace sectors require continuous logging of arc voltage, current amperage, heat input (kJ/mm), arc-on duty metrics, and wire consumption rates.
Our proprietary WeldVisor IoT Architecture bridges inverter control boards to cloud dashboards via Wi-Fi/4G. This enables real-time WPS compliance monitoring, predictive maintenance alerts for power module components, and complete serial-number traceability per joint.
Global electrical grid standards (such as EN 61000-3-12) mandate strict control over total harmonic distortion (THD). Conventional inverter power sources without active PFC draw non-linear current spikes, resulting in a low power factor (0.65 – 0.75) and tripper circuit breakers on mobile generator sites.
Future-ready procurement specifies Wide-Range Active PFC (90V – 460V) achieving a Power Factor > 0.99. This drastically reduces utility energy bills, permits operation on long extension cables (up to 100 meters), and enables lower kVA generator sizing for field construction.
With a chronic global shortage of skilled certified manual TIG welders, industrial fabricators are rapidly adopting collaborative robots (Cobots). Robotic TIG demands millisecond digital synchronization for high-frequency arc ignition, crater-fill sequences, and gas pre/post-flow control.
Our OEM ODM platforms feature dedicated digital automation ports supporting RS485, CANopen, and direct analog/digital I/O maps, allowing seamless pairing with Universal Robots, KUKA, FANUC, and ABB arms.
The next evolutionary leap beyond standard Silicon IGBTs is Wide-Bandgap Silicon Carbide (SiC) semiconductor modules. Operating at switching speeds exceeding 200 kHz, SiC-based TIG inverters deliver ultra-compact form factors, virtually zero thermal dissipation losses, and laser-like arc focus on microscopic precision assemblies.
Advanced Power Sources Limited (APS Welding) operates an ISO 9001:2015 certified manufacturing complex in Gujarat, India, delivering direct factory-to-brand partnerships with zero intermediary markup.
Unlike traders who rebrand off-the-shelf white-box units, our in-house engineering team designs the complete PCB schematics, micro-controller firmware, transformer magnetic coils, and heat-sink thermal channels from scratch.
Every manufactured inverter power source undergoes 100% full-load burn-in testing, high-voltage insulation dielectric checks, thermal chamber cycling, and synthetic dust vibration testing to ensure uncompromised site survivability.
We offer comprehensive private-label OEM/ODM agreements including sheet metal chassis color matching, customized LCD/LED user interface graphics, localized multi-language firmware, and custom export packaging designs.
Consult directly with our Chief Power Electronics Engineer to discuss custom firmware, electrical specs, and private-label contract manufacturing.
Addressing key technical evaluation parameters, standard duty cycle metrics, and global logistics queries for B2B buyers.
APS Welding (Advanced Power Sources Limited) is an ISO 9001:2015 certified industrial welding machine manufacturer located in Old GIDC Gundlav, Valsad, Gujarat, India. Operating for over 20 years with more than 22,600 machines installed worldwide, APS designs, manufactures, and services IGBT inverter TIG (GTAW), MIG (GMAW), Stick (SMAW), Submerged Arc (SAW), Plasma Cutters, and automated positioning machinery completely in-house.
Duty cycle ratings must always be evaluated at identical ambient temperatures and standardized testing intervals under IEC 60974-1 standards. Industrial-grade machines are rated based on a 10-minute operational cycle at 40°C ambient temperature. A machine rated 60% at 300A can operate continuously at 300 Amps for 6 minutes out of every 10 minutes without thermal shutdown. Beware of low-cost commercial units rated at only 20°C or 25°C ambient, which will suffer thermal failure under heavy continuous industrial shop duty.
High-Frequency (HF) Arc Start uses a high-voltage, low-current spark circuit to ionize the shielding gas path and ignite the arc without touching the tungsten electrode to the metal workpiece. This eliminates tungsten contamination and electrode tip damage, making it essential for high-spec code welding (such as pressure vessels and aerospace). Lift TIG ignition requires lightly touching the tungsten to the workpiece and lifting it to strike an arc. Lift TIG is used in environments sensitive to electrical interference, such as near CNC controls or medical electronics where HF high-frequency emissions are prohibited.
To provide an accurate engineering proposal and unit price breakdown, please provide: (1) Target site input power details (Voltage, Phase 1-Ph or 3-Ph, Frequency 50/60Hz); (2) Required welding processes (AC/DC TIG, DC Only, Pulse, Cold Wire Feeder integration); (3) Target duty cycle requirements at peak amperage; (4) Expected annual order volumes and private-label customization requirements (custom branding, UI language, enclosure IP rating).
APS Welding supplies complete technical documentation, schematics, PCB diagnostic guides, and spare parts packages for international distributors. We offer direct video-link engineering support, factory technician training at our Gujarat plant, and rapid air-freight dispatch for replacement mainboards and IGBT modules. All machines carry a comprehensive industrial warranty backed by direct factory R&D engineers.
Partner with an established ISO 9001:2015 manufacturer. Request detailed technical spec sheets, factory audit reports, and factory-direct wholesale quotations today.