Explore our heavy-duty submerged arc welding power sources, automated column & boom manipulators, gantry welding systems, and specialized pipe/beam machinery engineered for zero-defect output.
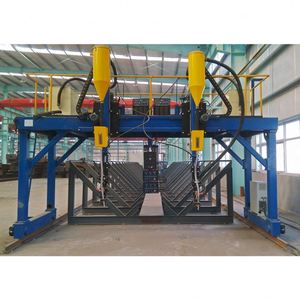
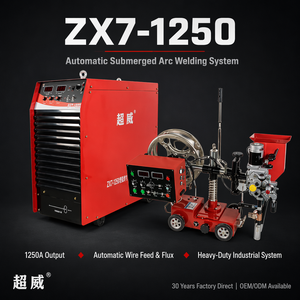
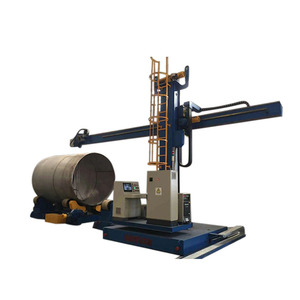
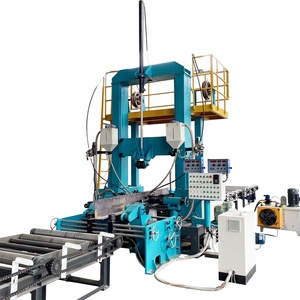
Submerged Arc Welding (SAW) remains the undisputed backbone of heavy steel fabrication worldwide. From pressure vessel fabrication, wind turbine tower production, and offshore jacket construction to structural H-beam welding and cross-country pipeline infrastructure, SAW technology offers unrivaled metal deposition rates, deep joint penetration, and exceptional thermal efficiency. However, modern manufacturing environments demand more than off-the-shelf welding power units; they require tailored, fully integrated OEM automation systems engineered around specific structural geometry, material metallurgy, and continuous duty cycles.
As a leading ISO 9001:2015 certified industrial welding machine manufacturer and exporter, Advanced Power Sources Limited (APS Welding) delivers cutting-edge IGBT inverter technology paired with turnkey mechanical automation. By moving away from legacy transformer-rectifier topologies toward advanced digital multi-process inverter architectures, modern fabricators can achieve energy efficiency gains exceeding 30%, superior arc stability, and precise control over heat input—critical for maintaining grain structure integrity in high-strength low-alloy (HSLA) steels.
Standard off-the-shelf welding equipment often forces fabricators to compromise on floor layout, cycle times, and operational ergonomics. Direct-to-factory custom OEM integration solves these friction points through purpose-built fixtures, customized travel gantries, synchronized column and boom manipulators, and customized digital interfaces. Whether your facility requires single-wire CC/CV sources, double-wire tandem systems, or integrated IoT monitoring (such as WeldVisor telemetry), working directly with an established engineering manufacturer ensures every subsystem is matched to your exact Welding Procedure Specification (WPS).
We do not operate as third-party traders. From printed circuit board (PCB) design to heavy structural gantry machining, every component is manufactured, tested, and serviced directly from our main manufacturing hub in Gujarat, India.
Our proprietary IGBT inverter control electronics are engineered completely in-house. This gives us absolute control over arc dynamics, digital signal processing, pulse waveforms, and rapid diagnostic fault detection.
Every SAW power source and automated tractor undergoes rigorous 100% duty cycle heat-run testing at 40°C ambient temperature per IEC 60974-1 standards prior to international export packing.
Single-vendor accountability. We manufacture the SAW inverter power source, column and boom manipulator, motorized flux recovery/rebuild system, and self-aligning rotators as one unified cell.
The industrial welding landscape is experiencing a paradigm shift driven by automation, decarbonization, smart monitoring, and stringent ultrasonic quality requirements. Understanding these technology vectors enables procurement teams to future-proof their capital equipment investments.
Traditional 50Hz SCR transformer-rectifier power sources are rapidly being phased out globally. Advanced IGBT inverter SAW power sources operate at switching frequencies above 20 kHz, resulting in compact footprints, reduced weight, and a power factor exceeding 0.93. The primary advantage lies in dynamic arc response: inverter technology reacts to arc length fluctuations within microseconds, virtually eliminating burn-through and bead profile irregularities.
To maximize shop floor throughput without expanding building footprint, leading fabricators are adopting Tandem SAW configurations (DC Lead torch for deep penetration + AC Trail torch for smooth surface cap and high deposition). Advanced digital AC waveform control prevents arc blow caused by magnetic interference between adjacent torches, allowing deposition speeds up to 1.8 meters per minute on thick structural plate.
Automation is moving from open-loop tactile tracking to closed-loop optical laser triangulation. Modern OEM SAW gantries feature optical seam trackers that detect joint bevel misalignment, gap variation, and tack weld locations in real-time, automatically adjusting torch height (AVC) and cross-seam position without operator intervention.
Quality traceability is mandatory in ASME Code, API, and EN 1090 certified fabrication. Modern SAW power sources incorporate cloud-connected IoT telemetry modules (e.g., APS WeldVisor). These systems continuously log welding current, arc voltage, travel speed, heat input (kJ/mm), wire consumption, and daily arc-on time, delivering real-time dashboards for quality managers and plant directors.
Choosing the correct mechanical delivery system is vital for operational productivity. Below is an engineering comparison of the primary SAW automation configurations supplied by OEM exporters:
| System Configuration | Target Applications | Deposition Capacity | Typical Amperage | Key OEM Feature |
|---|---|---|---|---|
| Tractor SAW Welder | Flat butt welds, long deck plates, shipbuilding flat seams | 10 – 15 kg/h (Single Wire) | 800A – 1250A | Portable 4-wheel drive, compact trackless travel, lightweight head |
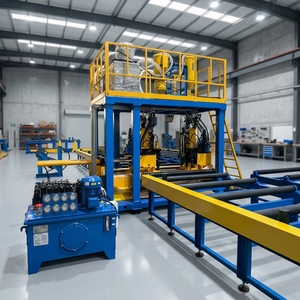
| H-Beam Welding Line (Gantry/Horizontal) | Structural H-Beams, I-Beams, tapered crane girders | 20 – 35 kg/h (Dual Torch / Twin) | 1000A x 2 / 1250A x 2 | Simultaneous fillet welding on both sides, automatic mechanical seam tracking |
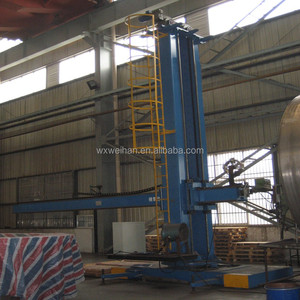
| Column & Boom Manipulator | Pressure vessels, tanks, pipe spools, wind tower shells | 12 – 30 kg/h (Tandem Compatible) | 1000A – 1600A Heavy Duty | VFD motorized boom travel, anti-fall safety devices, integrated flux recovery |
| Double Torch SAW Robotic Cell | Complex heavy structural joints, spherical domes, valve cladding | 15 – 28 kg/h | 800A – 1250A Multi-process | 6-axis robot synchronized with positioner, adaptive laser seam searching |
* All systems can be custom-configured with specific input voltages (380V, 415V, 460V, 575V at 50/60Hz) to match overseas site requirements.
Procurement strategies for heavy industrial equipment have evolved significantly. Global EPC contractors, shipyard procurement leads, and structural steel manufacturing directors evaluate vendors using sophisticated multi-factor metrics rather than upfront sticker price alone.
Smart buyers evaluate SAW equipment based on lifetime electrical efficiency, flux consumption efficiency, duty cycle overhead, and spare part accessibility. High-efficiency IGBT inverter power sources cut annual electrical consumption by tens of thousands of kilowatt-hours compared to legacy transformers, yielding a full ROI within 12 to 18 months of double-shift operation.
Purchasing a power source from one vendor, a manipulator from another, and a flux recovery unit from a third frequently results in control interface conflicts, mismatched duty cycles, and disputed warranty claims. The trend is firmly shifting toward single-source OEM exporters who design, build, and warrant the entire automated welding cell under one roof.
Speed to market is paramount for industrial projects. Global buyers prioritize factories capable of supplying modular, pre-engineered platform sub-assemblies that can be customized and shipped within accelerated 4 to 8-week timelines, backed by comprehensive factory acceptance testing (FAT).
Get expert answers to common technical, operational, and commercial queries regarding custom OEM automatic submerged arc welding systems.