Heavy-Duty Equipment for Structural Steel Mills, Tank Builders & Piping Contractors
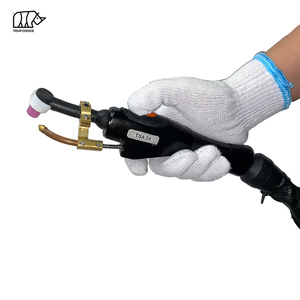
Precision engineering in structural steel fabrication demands specialized power sources, mechanized beveling tooling, and automated arc welding systems. Below is our curated industrial equipment showcase engineered for high deposition rates, robust duty cycles, and strict AWS/EN compliance in structural steel manufacturing.
Strategic Technical Analysis for International EPC Contractors, Industrial Developers & Sourcing Executives
In modern mega-infrastructure, high-rise architectural development, energy sector plants, and logistics parks, structural steel has established itself as the indispensable backbone of commercial engineering. As global procurement teams evaluate wholesale steel structure fabrication factories and machinery suppliers in China, the key criteria have evolved beyond basic cost per metric ton. Sourcing leadership now prioritizes structural integrity, dimensional tolerances under load, metallurgical weld repeatability, automated beam-line throughput, and verified international compliance standards including AWS D1.1 (American Welding Society), EN 1090-2 (Execution Class EXC1 to EXC4), and ISO 3834-2 certification.
To achieve maximum structural performance while keeping total cost of ownership (TCO) low, international buyers must analyze the complete supply chain—from raw material steel grade selection (e.g., ASTM A36, ASTM A572 Grade 50, EN 10025 S355JR/S355J2) to non-destructive testing (NDT) practices (Ultrasonic Testing, Radiographic Testing, Magnetic Particle Inspection). Advanced Chinese structural steel fabrication plants feature fully integrated automated lines incorporating 3D CNC pipe profile cutters, automated horizontal shell seam circumferential welders, portable edge beveling tools, and IoT-enabled arc monitoring systems.
E-E-A-T Benchmark Standards for Industrial Heavy Fabrication
Evaluating a wholesale factory’s expertise requires inspecting their internal quality control architecture. Quality structural steel fabrication relies on consistent metallurgical control, minimal heat-affected zones (HAZ), precise edge joint preparation, and zero-defect penetration on critical full-penetration butt joints.
All structural steel welding procedures must be validated by formal Welding Procedure Specifications (WPS) and Procedure Qualification Records (PQR). Certified welders operate high-duty cycle SMAW, GMAW, and SAW systems calibrated to strict voltage and current tolerances.
Comprehensive quality management governing fusion welding of metallic materials. Ensures traceably calibrated power sources, pre-heating protocols for heavy carbon steel sections, and controlled interpass temperatures to prevent hydrogen cracking.
100% Visual Inspection (VT) coupled with 20%–100% Ultrasonic Testing (UT) or Radiographic Testing (RT) on moment connections, bridge girders, and heavy crane runways, supported by EN 10204 3.1 Material Mill Test Certificates.
| Fabrication Process | Deposition Rate (kg/hr) | Target Structural Application | Automation Potential | Defect Risk & Mitigation |
|---|---|---|---|---|
| Submerged Arc Welding (SAW) | 8.0 – 15.0+ kg/hr | Heavy H-Beams, Box Columns, Vessel Shells | Fully Automated (Tractors/Boom) | Low defect rate; flux protects against atmospheric contamination. |
| GMAW / FCAW (Flux-Cored) | 3.0 – 6.5 kg/hr | Structural Frames, Web-to-Flange Fillets | Semi-Automated / Robotic Cells | Moderate porosity risk; requires gas shielding protection in field setups. |
| SMAW (Shielded Metal Arc) | 1.2 – 2.5 kg/hr | Field Erection, Stiffener Plates, Site Repairs | Manual Operation | Slag inclusion risk; requires skilled welder and thorough interpass cleaning. |
| GTAW / TIG (Pulse Argon Arc) | 0.5 – 1.8 kg/hr | Stainless Steel Structures, Thin Tubes, Root Pass | Cold-Wire Feeder Mechanized | Extremely low defect rate; high visual finish for architectural steel. |
Why Industrial Hardware Selection Dictates Project Schedules and Margins
Achieving structural steel fabrication excellence relies directly on shop-floor equipment capabilities. Modern Chinese wholesale factories utilize advanced machines to automate time-consuming prep work, eliminate manual human error, and accelerate production cycles:
High-frequency IGBT inverter power sources maintain ultra-stable arc characteristics, reduce electrical power consumption by up to 35% compared to legacy transformers, and support 100% duty cycles under 40°C ambient temperatures.
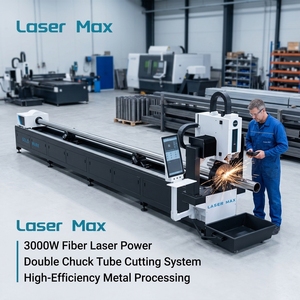
CNC sheet and tube fiber laser cutting machines (3kW to 15kW+) produce clean, burr-free bevel edges on heavy plate, eliminating secondary grinding and speeding up joint alignment for automated welding lines.
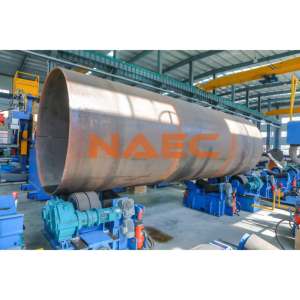
Motorized welding positioners and self-aligning rotators place complex weldments in the flat (downhand) position, boosting deposition rates by 40% while lowering welder fatigue and stress.
Real-time IoT arc-on time tracking and digital parameter logging verify heat input limits, enforce WPS boundaries, and ensure complete quality traceability for cross-border engineering projects.
Key Market Drivers Shaping International Supply Chains for the Next Decade
As environmental regulations, labor shifts, and digital transformation sweep the structural steel industry, global buyers must adjust their procurement strategies. Sourcing directors should track several core structural trends when vetting China wholesale fabrication suppliers:
Global construction is shifting heavily toward Modular Integrated Construction (MiC) and Prefabricated Prefinished Volumetric Construction (PPVC). Wholesale fabricators in China are upgrading facilities from standard beam cutting to fully finished 3D structural steel cassette manufacturing, complete with MEP penetration sleeves, fireproof coatings, and high-strength bolted connections.
To mitigate manual welder shortages, tier-1 Chinese factories are deploying multi-axis robotic welding cells powered by laser seam-tracking vision sensors. These systems continuously adjust torch angle and travel speed in real time, guaranteeing flawless fillet welds on complex structural node joints.
With international carbon border adjustment mechanisms (such as EU CBAM) taking effect, leading structural steel suppliers are transitioning to Electric Arc Furnace (EAF) steel billets powered by renewable energy. Quantifying embodied carbon per metric ton of fabricated steel is fast becoming a standard mandatory line item in major project tenders.
Leading fabrication plants now ingest Tekla/Revit BIM models directly into their CNC beam-processing software. Automated shot-blasting (Sa 2.5 standard) and automated paint-spray lines ensure uniform dry film thickness (DFT) for intumescent and anti-corrosion epoxies before ocean shipment.
Why Partnering with Our Manufacturing Ecosystem Mitigates EPC Project Risks
With over two decades of dedicated manufacturing experience, our enterprise hub bridges the gap between high-capacity steel structure production and advanced power source engineering. Overseas buyers deal directly with our in-house engineering and manufacturing team, eliminating middleman markups while ensuring full technical transparency.
We design, assemble, and test our IGBT inverter power boards, control firmware, and automation software internally. Technical requests or customized arc dynamics are solved directly by our core design engineers.
Every single machine and fabricated assembly undergoes strict stage inspections—from raw plate incoming chemical checks to 100% full-load thermal burn-in testing prior to export packing.
Our heavy-duty power sources, positioners, submerged arc tractors, and plasma cutters operate reliably across demanding shipyards, pipeline trenches, pressure vessel shops, and structural steel mills worldwide.
Essential Verification Steps Before Placing Wholesale Structural Steel Orders
To prevent project delays, unexpected shipping costs, or field fit-up failures, procurement teams should use this audit framework when evaluating Chinese structural steel fabrication suppliers:
Confirm the mill source for structural plate and structural hollow sections (HSS). Ensure heat numbers stamped on physical steel match EN 10204 3.1 Mill Test Certificates for yield strength, tensile strength, and impact toughness (Charpy V-notch testing at -20°C or -40°C).
Verify that factory welders hold current performance qualification records (WPQR) matching AWS D1.1 or ISO 9606-1 in the specific positions (3G, 4G, 6G) and processes required for your structural members.
Require 3D laser tracker verification or mandatory trial shop assembly for complex spatial trusses, bridge spans, and heavy box columns to guarantee zero-misfit field bolting on site.
Check surface profile roughness (typically 40–75 microns following ISO 8503-2) post shot-blasting, and review paint ambient conditions (dew point monitoring) to prevent early coating delamination or marine rust.
Clear Answers to Common Technical and Sourcing Questions
Connect directly with our senior application engineers to review your project drawings, select high-efficiency power sources, or schedule a comprehensive factory audit.
Contact Us