
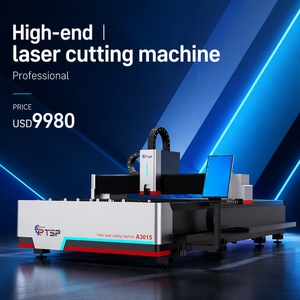
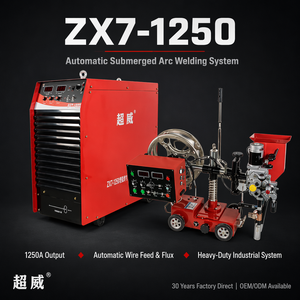
Explore our heavy-duty portable bevelers, CNC laser cutting centers, automated submerged arc welders, and welding automation solutions designed for global fabricators.
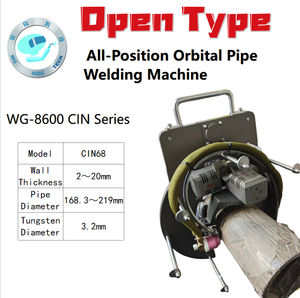
In modern structural steel erection, pressure vessel manufacturing, aerospace ducting, and nuclear pipeline fabrication, achieving a flawless root pass is directly governed by weld joint geometry precision. Historically, fabricators relied heavily on manual angle grinding or oxy-fuel/plasma flame cutting to achieve V, K, X, and J bevel bevel angles. However, as international welding standards such as ASME Section VIII, AWS D1.1, ISO 9692, and EN 1090-2 enforce strict quality verification, thermal beveling methods are increasingly scrutinized due to structural metallurgy degradation.
When carbon steel, duplex stainless steel, nickel alloys, or titanium plates undergo plasma or oxy-acetylene torch beveling, the edge temperature spikes beyond the upper critical transformation point (Ac3). This intense local thermal cycle introduces microstructural anomalies:
China Portable Beveling Machine Manufacturing Advantage: Our industrial cold-milling technology utilizes indexable carbide inserts operating at controlled surface speeds. By mechanically shearing the metal without heat generation, our machines maintain a 0.00 mm Heat-Affected Zone (HAZ), preserving the substrate’s original mechanical grain structure and tensile yield strength.
| Process Parameter | Cold Milling Portable Beveler | Manual Angle Grinding | CNC Plasma Torch Beveling |
|---|---|---|---|
| Heat-Affected Zone (HAZ) | 0.00 mm (Zero Thermal Alteration) | Low-Moderate (Localized Scorching) | High (0.5 mm – 2.5 mm HAZ depth) |
| Angle Precision & Repeatability | ±0.5° Constant Index Angle | Irregular (Operator Dependant ±5°) | ±1.5° Torch Wobble Drift |
| Surface Roughness (Ra) | Ra 1.6 – Ra 3.2 µm (Mirror Finish) | Ra 12.5 – Ra 25 µm (Deep Grooves) | Ra 6.3 – Ra 12.5 µm (Dross Marks) |
| Bevel Speed (Plate/Pipe) | 1.2 – 3.0 meters / minute | 0.2 – 0.4 meters / minute | 0.8 – 1.5 meters / minute |
| Post-Processing Requirement | None (Immediate Fit-Up & Weld) | De-burring & Cleaning Needed | Slag/Dross Removal & HAZ Grinding |
| Operator Health & Safety | Low Noise, Swarf Chips (No Fumes) | Severe Dust, Vibration, Spark Hazard | Toxic Smoke, UV Radiation, High Heat |
Direct from China’s leading wholesale manufacturer: Precision engineered systems tailored for pipe fabrication yards, shipbuilding bays, boiler production, and structural steel plants.
Designed for internal expansion clamping along the pipe inner wall, ideal for boiler tubes, power plant piping spools, and high-pressure steam lines.
Self-propelled milling equipment that crawls along the edge of steel plates, eliminating manual feeding in heavy structural engineering and tank construction.
Ergonomic portable units designed for deburring, inner hole chamfering, radius contour milling (R2, R3, R4), and paint adhesion preparation per ISO 8501-3.
Low-clearance split-frame technology for simultaneous orbital cutting and beveling of inline piping during turnarounds and subsea installations.
As global engineering, procurement, and construction (EPC) contractors replace manual Stick (SMAW) welding with automated narrow-gap Gas Metal Arc Welding (GMAW) and Submerged Arc Welding (SAW), traditional 37.5° V-bevels are being phased out on thick-wall pipes (>20 mm). V-grooves demand excessive filler metal deposition, increasing consumable costs and arc-on times.
The J-Prep Efficiency Gain: A 10° to 15° compound J-bevel with a 6 mm to 8 mm radius reduces total weld metal volume by up to 45% to 60% compared to a standard V-bevel. China portable beveling machine factories are now equipping machines with Form Carbide Cutters that produce flawless J-prep profiles and root lands in a single machining pass.
Procurement directors are shifting focus from simple hardware purchase price to Total Cost of Ownership (TCO) and digital traceability. Next-generation portable bevelers manufactured in our China OEM facilities feature integrated load sensors and variable-frequency digital drives (VFD):
To evaluate true procurement economics, consider a project requiring 10,000 meters of weld prep on 20 mm S355 structural steel plate:
| Cost Component (10,000m Project) | Manual Angle Grinding Discs | China Wholesale Milling Beveler |
|---|---|---|
| Consumable Cost | ~2,500 Grinding Discs ($10,000 USD) | ~20 Sets Indexable Carbide Inserts ($1,800 USD) |
| Direct Labor Hours | ~1,250 Man-Hours (Slow 0.3m/min) | ~110 Man-Hours (Fast 1.5m/min Auto-Feed) |
| Weld Rework / Defect Penalty | High (Irregular bevel angle causes lack of penetration) | Zero (Precision root face prevents blow-through) |
| Net Cost Savings | Baseline Baseline | 74% Total Cost Reduction |
We are not mere trading intermediaries; we are an established engineering enterprise with 20+ years of dedicated cold-cutting research, CNC machining centers, and strict quality assurance.
Every gear housing, expansion mandrel, tool post, and spindle drive is milled inside our 25,000 m² ISO-certified plant using Japanese Okuma CNC centers and continuous vacuum heat treatment.
Before export dispatch, every electric, pneumatic, or hydraulic machine undergoes a continuous 4-hour full-load milling trial on Hardox 500 and 316L stainless steel plates to verify torque stability and heat dissipation.
We provide complete private labeling, custom voltage/frequency adaptation (110V/220V/380V/440V at 50Hz/60Hz), custom milling tool heads, and worldwide door-to-door DDP logistics support.
Essential technical, financial, and operational insights for overseas procurement officers and engineering directors.
Cold milling mechanically shears the metal without applying thermal heat, leaving a 0.00 mm Heat-Affected Zone (HAZ), zero metallurgical micro-cracks, and no toxic fumes. It delivers a smooth surface finish (Ra 1.6–3.2 µm) ready for immediate welding without post-processing grinding, satisfying strict ASME, AWS, and EN 1090 structural codes.
Our ID-mounted and OD split-frame pipe beveling machines process pipe wall thicknesses up to 75 mm (Schedule 40, 80, 160, XXS). For plate beveling, our heavy auto-feed walking machines easily handle plate thicknesses from 6 mm up to 100 mm, producing single-pass bevel widths up to 45 mm and multi-pass widths up to 110 mm.
Yes. Our machines are engineered with heavy-duty gearboxes and high-torque electric/pneumatic drives specifically tuned for tough materials. When equipped with our custom TiAlN or TiCN coated tungsten carbide inserts, our bevelers clean-cut 304/316L stainless steel, Super Duplex, Inconel 625, P91 alloy steel, and wear-resistant Hardox 400/500 plates.
We supply electric machines compatible with global industrial power standards: Single-phase 110V/220V (50/60Hz) for site maintenance, and 3-phase 380V/415V/440V/480V (50/60Hz) for workshop production lines. For hazardous explosion-proof environments (oil & gas refineries, chemical plants), we offer 100% pneumatic motor drives operating on standard 0.6–0.8 MPa compressed air.
On standard Q235/S275 carbon steel plate, one set of 4-edge indexable carbide inserts typically lasts for 150 to 250 meters of continuous beveling per edge side (totaling up to 1000 meters per set of inserts). Because inserts are 4-way indexable, simply rotate the blade 90° when one edge wears out to instantly restore a sharp cutting face.
Yes. As a direct wholesale manufacturer, our in-house engineering team designs and manufactures custom cutter heads for compound J-preps, double-V (X-bevels), transition counter-boring, and clad plate stripping. Custom CAD drawings are supplied for customer approval prior to CNC tool production.
Standard electric and pneumatic pipe/plate bevelers are maintained in stock for rapid dispatch within 3 to 5 business days. Custom voltage adaptations or heavy-duty split-frame clamshell machines require 10 to 15 days. We guarantee 10-year spare parts availability (bearings, gears, motor carbon brushes, carbide inserts) dispatched globally via DHL/FedEx within 24 hours.
Direct factory pricing, comprehensive technical warranty, and engineering support for global B2B distributors and engineering contractors.