
Explore high-precision longitudinal seam welders, fiber laser cutters, PTA plasma cladding units, and heavy-duty gouging torches direct from certified Chinese OEM factories.
An in-depth technical analysis on optimizing weld integrity, thermal heat input, and deposition rates for cylindrical, conical, and rectangular sheet metal fabrications.
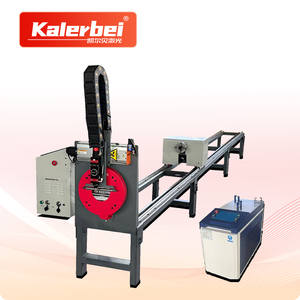
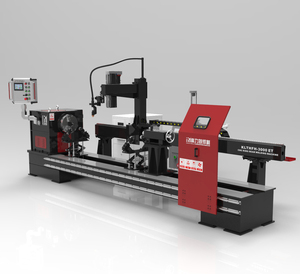
In modern industrial manufacturing, the fabrication of pressure vessels, process piping, water storage tanks, transformer housings, and aerospace cylinders demands absolute precision in linear seam joining. Longitudinal seam welding machines serve as the backbone of automated tank and pipe production lines, replacing error-prone manual welding with continuous, high-efficiency mechanized processes.
Chinese wholesale factories have emerged as global leaders in this sector, evolving from basic mechanical fixture builders to advanced integration hubs utilizing IGBT inverter digital power sources, closed-loop arc length control (AVC), water-cooled copper backing mandrels, and pneumatic finger clamping systems. Selecting the optimal China OEM manufacturer requires a profound understanding of metallurgical heat dissipation, workpiece clamping geometry, and process integration (TIG, PAW, GMAW, and SAW).
Integrating decades of power electronics engineering with specialized structural automation, Chinese tier-1 factories deliver turnkey production efficiency.
Our partner manufacturing lines integrate proprietary IGBT inverter power sources operating at high switching frequencies (up to 100 kHz). This ensures instantaneous arc stabilization, minimal spatter, precise dynamic response during keyhole seam welding, and up to 30% reduction in workshop energy consumption compared to legacy transformer-based systems.
Equipped with independent piano-key pneumatic fingers, our seam welders apply uniform clamping pressure along the entire linear joint. Integrated water-cooled copper backing bars with continuous gas purging prevent thermal burn-through, eliminate oxidative scaling on the root side, and maintain tight alignment tolerances on thin-gauge materials down to 0.4mm.
China OEM seam welding beds feature modular torch carriages that accept GTAW (TIG) with cold wire feeding, Plasma Arc Welding (PAW) for deep penetration without beveling, Submerged Arc Welding (SAW) for thick wall cylinders, and GMAW (MIG/MAG) for rapid structural deposition.
Every industrial machine undergoes continuous duty cycle load testing, insulation testing, and laser alignment verification under strict ISO 9001:2015 management systems. Factory acceptance testing (FAT) ensures zero-defect delivery before international shipping.
Smart factories integrate real-time telemetry modules (WeldVisor IoT) to record arc-on duration, peak current, voltage drift, travel speed, and shield gas flow rate. This data visualization supports complete quality auditing for ASME code compliance.
From automatic sheet loading arms to motorized alignment rotators and hydraulic positioners, Chinese suppliers deliver fully integrated longitudinal seam welding bays tailored to your factory layout.
Select the appropriate process technology based on material thickness, target cycle speed, metallurgical requirements, and quality standards.
| Welding Process | Wall Thickness | Travel Speed | Key Hole Penetration | Backing Gas Requirement | Primary Industrial Applications |
|---|---|---|---|---|---|
| TIG (GTAW) + Cold Wire | 0.4 mm – 4.0 mm | 150 – 450 mm/min | Conduction Mode | Mandatory (Argon / Mix) | Stainless steel sanitary pipe, solar water heaters, food tanks |
| Plasma Arc Welding (PAW) | 1.0 mm – 10.0 mm | 300 – 800 mm/min | Full Keyhole (Single Pass) | Mandatory (High Purity Ar) | Titanium aerospace cylinders, chemical pressure vessels, cryo-tanks |
| MIG/MAG (GMAW / Pulse) | 2.0 mm – 8.0 mm | 400 – 1200 mm/min | Partial / Bevel Required | Optional depending on alloy | Carbon steel drums, transformer tanks, automotive air receivers |
| Submerged Arc (SAW) | 6.0 mm – 25.0 mm+ | 350 – 900 mm/min | Deep Penetration (Heavy Duty) | Granular Flux Shielding | Wind turbine towers, LPG storage bullets, structural steel columns |
| Fiber Laser - Arc Hybrid | 0.5 mm – 12.0 mm | 1000 – 3500 mm/min | Keyhole High Speed | Top & Root Purge | High-volume automotive mufflers, precision alloy tubes, HVAC shells |
How Chinese factories are innovating next-generation linear seam equipment to meet strict international standards.
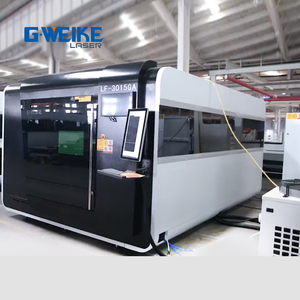
Legacy linear seam welders relied on rigid mechanical guide wheels that failed when sheet metal exhibited thermal warpage or pre-weld gaps. Next-generation Chinese longitudinal seam welders incorporate laser line vision sensors and neural network controllers. These systems dynamically adjust torch alignment (X/Y axes), arc voltage height (Z axis), wire feed rate, and travel speed in real-time, tolerating joint fit-up variations up to 1.5mm without burn-through.
In heavy pressure vessel fabrication, cutting deep V-bevels wastes immense filler material and increases thermal deformation. Advanced PAW longitudinal seam welders achieve single-pass square butt welding up to 10mm wall thickness without beveling. By compressing the plasma arc using focused orifice gas and precise pilot current circuitry, factories drastically reduce gas consumption and achieve 100% X-ray quality welds (ASME Section VIII compliant) in half the time.
Energy cost reduction is a major priority for global buyers. Modern Chinese seam welder power sources utilize power factor correction (PFC > 0.98) and closed-loop inverter power modules. Coupled with localized micro-channel water-cooled copper backing bars, thermal radiation into the surrounding shop floor is reduced by 40%, safeguarding operator safety and extending component lifespan.
Navigating supplier selection, factory audits, Total Cost of Ownership (TCO), and overseas after-sales support.
International procurement heads are bypassing trading intermediaries to work directly with China original equipment manufacturers. Direct technical communication enables customized bed lengths (from 500mm up to 6000mm), specialized mandrel expansion mechanisms, custom backing bar grooves for exotic alloys (Hastelloy, Duplex SS, Titanium), and integrated PLC interfaces (Siemens, Omron, Mitsubishi).
While initial capital expenditure (CapEx) for a Chinese automated longitudinal seam welder is roughly 40-60% lower than European or North American counterparts, global buyers evaluate TCO over a 10-year horizon. High reliability of IGBT modules, standard non-proprietary wear parts, and remote diagnostic ethernet modules ensure rapid troubleshooting and lower operational expenditure (OpEx).
Leading Chinese exporters offer comprehensive remote FAT protocols. Buyers submit sample metal sheets (stainless, mild steel, aluminum) to the factory in China. Technical teams execute test welds, perform radiographical (NDT) testing, macro-etching, and tensile testing on-camera, verifying procedural compliance before export packing.
Key insights to help engineering and purchasing teams make informed machinery procurement decisions.
Longitudinal seam welding machines can process sheet metal thicknesses ranging from 0.3mm to 25mm+, depending on the chosen process configuration. Thin-gauge materials (0.3mm to 3.0mm) typically utilize Micro-TIG or Fiber Laser welding with finger-key clamping and water-cooled copper mandrels. Medium to heavy wall thicknesses (4.0mm to 10mm) use Keyhole Plasma (PAW) or Tandem MIG. Extremely thick cylinders (10mm to 25mm+) utilize Submerged Arc Welding (SAW) with pre-beveled joint preparations.
The copper backing bar serves three vital functions during automated seam welding: 1) Heat Sink Effect: Copper's high thermal conductivity draws excess heat away from the weld zone, preventing burn-through, warping, and grain growth in the Heat-Affected Zone (HAZ). 2) Weld Root Shaping: A precision-machined groove in the copper bar supports the molten weld pool, forming a uniform, smooth root bead. 3) Shielding Gas Channel: Integrated gas ports deliver inert shielding gas (Argon or Nitrogen mix) directly to the molten root underside, preventing oxidation on reactive metals like stainless steel and titanium.
High-end China factories build rigid heavy-duty stress-relieved steel gantry frames. Pneumatic piano-key clamping fingers apply independent vertical pressure on both sides of the seam. Furthermore, alignment accessories such as pneumatic edge alignment pins, centralizing laser lines, and hydraulic mandrel expanders eliminate workpiece tacking misalignment and mismatch prior to torch travel.
Yes. A single longitudinal seam welder bed can accommodate a broad range of diameters. The key parameter is the mandrel diameter and the open height under the clamping fingers. Standard models handle diameters from 100mm up to 1000mm or more. For smaller diameter tubes (e.g., 50mm - 150mm), interchangeable drop-in copper mandrels are used. Machine bed lengths are fixed (e.g., 1000mm, 1500mm, 2000mm, 3000mm), but shorter parts can be clamped and welded anywhere along the bed length.
Export-oriented Chinese manufacturers build equipment in compliance with CE Mark Directive 2006/42/EC (Machinery), Low Voltage Directive 2014/35/EU, and Electromagnetic Compatibility (EMC) Directive 2014/30/EU. Power sources meet IEC 60974-1 standards. For North American buyers, machinery can be optioned with CSA-compliant wiring and UL-listed electrical panels (Schneider or Siemens control gear).
Leading suppliers provide comprehensive support including remote PLC diagnostic connection via VPN, online video-assisted commissioning, detailed English technical documentation, and spare part packages (copper fingers, ceramic nozzles, gas diffusers, drive rollers). On-site technician deployment for installation, parameter tuning, and operator training is available globally upon request.
Consult with our senior welding automation engineers. Receive custom seam welder layout drawings, process recommendations, and factory-direct wholesale pricing within 24 hours.