Explore top-rated industrial positioning rotators, plasma processing platforms, and high-efficiency carbon arc gouging equipment built for continuous heavy fabrication environments.
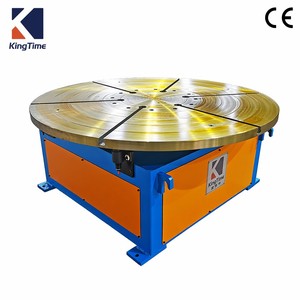
In heavy industrial manufacturing—spanning pressure vessel construction, oil & gas storage tank fabrication, wind turbine tower production, and nuclear pipe spooling—the efficiency and structural integrity of circumferential arc welding depend heavily on precision workpiece positioning. As a leading manufacturer and global exporter of industrial welding power sources and automation turnkey setups, our engineering division delivers state-of-the-art tank turning rolls (welding rotators) engineered to minimize operator intervention, eliminate longitudinal vessel drift, and guarantee stable linear circumferential speeds under harsh workshop conditions.
Tank turning rolls, also designated as vessel turning rotators or pipe alignment beds, utilize motorized drive units coupled with idler roller assemblies to rotate cylindrical workpieces smoothly beneath stationary submerged arc welding (SAW), gas metal arc welding (GMAW), or gas tungsten arc welding (GTAW) heads. Selecting the correct turning roll configuration requires an in-depth mechanical audit of workpiece load distribution, dynamic friction factors, shell deflection limits, and rotational torque demands.
Engineered with stress-relieved welded steel chassis and double-ended planetary gearboxes, our turning rolls prevent frame distortion even when loaded with non-uniform heavy wall pressure vessels weighing up to 1,000 metric tons.
Equipped with digital variable frequency drives (VFD) and high-resolution encoder feedback, offering seamless speed control from 100 mm/min to 1200 mm/min for precise heat input management during multi-pass welding.
With over two decades of dedicated manufacturing experience, our ISO 9001:2015 certified production base integrates complete in-house R&D, heavy CNC machining centers, dynamic wheel balancing setups, and real-time load testing bays. Unlike trading entities that rebrand standardized components, we engineer every critical sub-assembly in-house—from electronic control boards to polyurethane wheel formulations.
Our control systems feature proprietary digital microprocessor architecture, ensuring noise-immune RS485/Modbus integration with column & boom manipulators and automatic SAW power units.
We synthesize high-wear, tear-resistant polyurethane (PU) linings directly bonded to heavy steel cores, protecting thin-walled stainless steel or titanium tanks from surface contamination and crushing.
Every drive unit undergoes a continuous 48-hour full-load thermal endurance test and ultrasonic gear weld check before export, guaranteeing zero downtime upon jobsite delivery.
Choosing the optimal turning roll setup requires evaluating tank diameter variations, vessel material composition, wall thickness, and whether jobsite operations require frequent size adjustments.
Ideal for production runs of uniform vessel diameters. Roller center distances are adjusted manually via pre-drilled bolt slots or lead screws. Built with twin heavy-duty AC motors and synchronized worm gearboxes for maximum mechanical lock.
Designed for fabricators working with varying tank diameters. Four roller assemblies automatically adjust their angle of contact when a tank is loaded, automatically maintaining four-point load distribution without manual mechanical adjustments.
Advanced hydraulic alignment beds equipped with independent vertical, horizontal, and axial displacement cylinders. Allows operators to align separate shell segments precisely for tacking and circumferential seam welding.
Incorporates closed-loop photoelectric axial sensors and motor-driven lead screw tilting mechanisms on the idler rotators to correct axial vessel walking, keeping narrow bevel seams aligned under high-speed SAW welding.
| Model Series | Rated Capacity | Diameter Range | Wheel Options | Drive Synchronisation | Primary Industrial Field |
|---|---|---|---|---|---|
| CR-10 | 10 Metric Tons | Ø 300 – 3,000 mm | High-Grade Polyurethane | Dual AC VFD Vector Drive | Light LPG Tanks, Piping Spools |
| CR-60 | 60 Metric Tons | Ø 600 – 5,000 mm | PU / Forged Alloy Steel | Digital Microprocessor Bus | Petrochemical Heavy Storage Vessels |
| HGK-20 | 20 Metric Tons | Ø 500 – 3,500 mm | Self-Aligning PU Quad-Wheels | Integrated Control Cabinet | General Tank Fabrication Shops |
| HGK-100 | 100 Metric Tons | Ø 1,000 – 6,000 mm | Heavy Steel Cores / PU | Dual Planetary Gearbox Sync | Pressure Vessel Shell Fit-Up |
| ADR-150 | 150 Metric Tons | Ø 800 – 6,500 mm | Hardened Tool Steel | Closed-Loop Servo Tilting Anti-Drift | Nuclear Power & Offshore Monopiles |
Global B2B procurement patterns for welding automation equipment are undergoing a major shift. Industrial buyers, EPC contractors, and vessel fabricators no longer evaluate turning rolls solely on static mechanical weight ratings. Tomorrow’s smart factories demand connectivity, sensorized protection, and zero-defect drift tracking.
Modern procurement specifications increasingly mandate IoT-connected turning rolls capable of transmitting real-time rotational RPM, motor current draw, bearing temperature, and cumulative arc-on hours directly to centralized enterprise platforms (MES/ERP).
Rather than operating as standalone mechanical units, future turning rolls must interface directly with laser seam trackers and motorized welding column-and-booms, automatically dynamic-adjusting rotational linear speed to compensate for joint root gap variations.
With growing demand for LNG storage vessels, hydrogen tanks, and pharmaceutical stainless reactors, buyers require specialized non-marking, non-contaminating polyurethane formulations that resist delamination under heavy point loads.
To keep pace with extreme vessel fabrication demands—such as offshore monopiles exceeding 2,000 tons and ultra-thick nuclear heat exchangers—our engineering teams are driving key technological breakthroughs:
Legacy passive thrust rollers often cause severe localized flange deformation. Next-generation anti-drift turning rolls utilize high-precision linear displacement transducers (LVDT) combined with motorized vertical lead screws on the idler bed. When sensors detect vessel axial shift > 0.2 mm, the PLC gently tilts the roller axis, using controlled vector forces to guide the vessel back to center without damaging tank walls.
Continuous rotation of massive unbalanced vessels creates significant kinetic back-EMF during acceleration and deceleration. New drive systems integrate regenerative braking modules, feeding excess kinetic energy back into the shop grid while ensuring smooth stop/start sequences without weld crater flaws.
To prevent costly mechanical mismatches, structural failures, or premature drive burnouts, engineering procurement teams should verify the following five parameters prior to issuing a purchase contract:
Calculate vessel weight plus internal attachments (stiffeners, nozzles). Account for out-of-roundness eccentricity to ensure drive motors provide adequate starting torque.
Verify that the wheel width and polyurethane hardness (Shore A 85–95) can handle peak point loads without permanent deformation or surface debonding.
Ensure stepless speed regulation covers both slow SAW root pass requirements (6–15 m/hr) and fast positioning speeds (60–100 m/hr).
Confirm heavy-duty copper welding ground brushes (capable of carrying 1000A–1500A continuous current) are integrated directly into the turning roll spindle to prevent bearing arcing damage.
Key answers to common technical queries raised by global procurement specialists, welding engineers, and plant managers.
Whether you require standard 10-ton vessel rotators, heavy 500-ton anti-drift fit-up beds, or customized turnkey pipe profile cutting lines, our application engineering team is ready to deliver tailored CAD drawings, load calculations, and competitive factory-direct quotations.