Engineered for Continuous Heavy-Duty Duty Cycles, Superior Arc Constriction, and Maximum Cut Quality
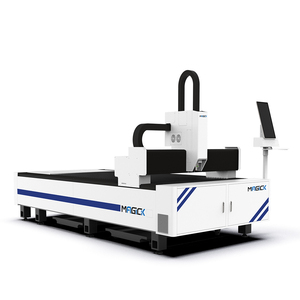
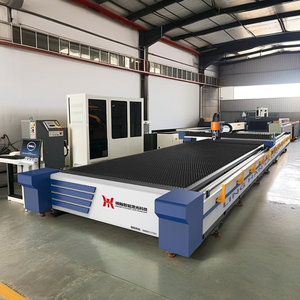
Thermal cutting technology remains the cornerstone of modern heavy structural steel fabrication, pressure vessel engineering, shipbuilding, and industrial pipe manufacturing. Among all non-contact and contact thermal cutting methodologies, High-Definition Plasma Cutting (HD Plasma) and High-Amperage Mechanized Plasma Torch systems represent the optimal convergence of metallurgical cutting velocity, operational cost-per-meter, and bevel edge precision. As global manufacturing hubs seek elevated production efficiency and reduced post-cut grinding overhead, China's premier plasma cutting torch factories have evolved from low-cost component fabricators into advanced original equipment manufacturers (OEM) and technology exporters capable of engineering high-end plasma power sources, torch geometry dynamics, and automated CNC gantry integration.
Information Gain Key Insight: Modern high-definition plasma cutting torches operating at currents above 200A require dual-gas vortex stabilization and liquid-cooled swirl baffles to achieve ISO 9013 Class 3 bevel angles (<2.5° angular deviation). Top-tier Chinese plasma torch manufacturers utilize oxygen-free high-conductivity (OFHC) copper embedded with tellurium-copper alloys and Hafnium inserts to extend consumable life cycles by over 300% under continuous 100% duty cycle operations.
The cutting capability of a plasma torch is governed by the laws of magnetohydrodynamics and gas thermal ionization. When pressurized shielding gas (such as Compressed Air, Oxygen, Nitrogen, or H35 Argon-Hydrogen mixtures) passes through the constricted orifice of the torch nozzle, an electric arc generated between the tungsten/hafnium cathode and the workpiece ionizes the gas into a high-temperature plasma jet exceeding 20,000°C. China's top plasma torch factories focus heavily on optimizing three critical internal torch components:
Why International Procurement Directors Partner with China's Premier Torch & Power Source Factories
Unlike trading entities that aggregate white-label components, elite Chinese manufacturers design high-frequency IGBT inverter power boards, digital arc-control firmware, and torch body molds entirely in-house for complete engineering control.
Every industrial plasma cutting power source and plasma torch assembly undergoes continuous 100% duty cycle load testing under severe 40°C ambient temperatures, verifying thermal cut-off margins prior to global export shipping.
Standardized CNC interface protocols, voltage divider outputs, and ohmic height-sensing compatibility allow effortless plug-and-play installation onto CNC gantry tables, robotic arm cells, and pipe profiling systems.
Industry 4.0 enabled plasma cutting systems featuring remote operational monitoring, tracking real-time arc-on hours, consumable wear indices, line voltage drops, and operational gas pressure stability.
As the international metal fabrication market transitions toward automated, low-emission, and smart factory standards, global buyers face shifting procurement dynamics when selecting China-based plasma torch suppliers. Key sourcing trends include:
To assist industrial engineers and procurement specialists in selecting the optimal cutting technology for their factory floor, the following empirical comparison evaluates key operational metrics across carbon steel, stainless steel, and aluminum plate processing:
| Evaluation Parameter | High-Definition Plasma Torch | Fiber Laser Cutting Machine | Oxy-Fuel Heavy Cutting Torch | Abrasive Waterjet Cutting |
|---|---|---|---|---|
| Optimal Plate Thickness | 6 mm to 50 mm | 0.5 mm to 25 mm | 25 mm to 300+ mm | 1 mm to 100+ mm |
| Cutting Velocity (20mm Mild Steel) | Very High (~1,800 mm/min) | High (~2,200 mm/min) | Low (~400 mm/min) | Very Low (~120 mm/min) |
| Initial Capital Expenditure (CAPEX) | Moderate / Balanced | High to Very High | Low | High |
| Consumable Operating Cost (OPEX) | Low (Nozzles, Electrodes, Gas) | Low (Assist Gas, Lenses) | Low (Gases, Tips) | High (Garnet Abrasive) |
| Bevel Angle Quality (ISO 9013) | Class 2 – Class 3 (<3°) | Class 1 – Class 2 (<1.5°) | Class 3 – Class 4 (<5°) | Class 1 (<1°) |
| Heat Affected Zone (HAZ) | Narrow (Fast Speed Dissipation) | Extremely Narrow | Wide (High Heat Soaking) | Zero Thermal Distortion |
| Automation Compatibility | Excellent (CNC, Robot, Pipe) | Excellent (Gantry Sheet Enclosure) | Moderate (Gantry Motorized) | Moderate (Gantry CNC) |
The plasma cutting industry is undergoing a technological revolution powered by digital power electronics, gas dynamic simulations, and advanced surface coating chemistry. China's top plasma cutting torch factories are pioneering several critical advancements:
Torch height control (THC) accuracy directly affects nozzle lifespan. Modern mechanized torches incorporate integrated capacitive voltage division and ohmic contact feedback circuits right inside the torch body. This prevents the torch tip from plunging into molten metal during the initial piercing phase—the single largest cause of premature nozzle destruction.
By employing computational fluid dynamics (CFD) to model supersonic plasma gas expansion, Chinese engineers have created constricted nozzle interiors that maintain arc column stiffness at reduced gas flow rates. This innovation cuts shield gas consumption by up to 25% without sacrificing piercing speed or edge smoothness.
Environmental standards in European and North American markets mandate strict workplace air quality control. Hand-held and semi-automated plasma torches now offer integrated vacuum shroud attachments that capture up to 90% of sub-micron metallic oxide fumes directly at the arc source before they disperse into the workshop atmosphere.
Technical Clarifications for Global Importers, Distributors, and Engineering Buyers
The choice depends on plate thickness, daily production volume, and edge precision requirements. Air plasma torches (typically 40A to 120A) rely on ambient compressed air for both arc plasma creation and cooling; they are ideal for manual cutting, light structural steel, and maintenance workshops where cut angle tolerances are non-critical. Conversely, Liquid-Cooled High-Definition (HD) Plasma Torches (200A to 400A+) circulate liquid coolant around the nozzle and electrode and utilize specialized gases (O2, N2, H35). They are essential for continuous CNC gantry operations cutting plate above 12mm where square edges (<2° bevel), zero dross, and 100% duty cycle reliability are mandatory.
The four primary culprits of rapid consumable degradation are: (1) Incorrect Piercing Height: Piercing too close to the workpiece causes molten slag to splash back onto the nozzle orifice, causing double-arcing. (2) Moisture or Oil in Compressed Air: Contaminated air disrupts arc ionization and rapidly oxidizes the hafnium electrode core. Compressed air lines must utilize refrigerated dryers and multi-stage oil coalescing filters. (3) Inadequate Gas Flow Rates: Low gas pressure fails to constrict the arc, causing the arc to root directly onto the copper nozzle wall. (4) Coolant Flow Interruption: On liquid-cooled torches, scale buildup or low coolant flow leads to instantaneous copper thermal meltdown.
Reputable China plasma torch and power source factories rate their equipment in compliance with international standard IEC 60974-1. Duty cycle tests are conducted in a controlled environmental chamber at 40°C ambient temperature over a 10-minute cycle period. A 60% duty cycle rating at 200A means the machine can cut continuously for 6 minutes at 200 Amperes before requiring a 4-minute cooling period. Heavy industrial models intended for export are rated at 100% continuous duty cycle at maximum rated amperage.
Yes. Leading Chinese plasma torch exporters design their mechanized torches with standardized mounting barrel diameters (e.g., 35mm or 50mm smooth body), industry-standard thread connections, and universal arc-ignition wiring. Whether your CNC table utilizes Hypertherm, Thermal Dynamics, ESAB, or generic stepper/servo controllers, Chinese torch manufacturers supply adapter cables, voltage divider modules, and custom pin-out plugs to enable seamless retrofit integration.
When evaluating China plasma cutting torch factories, ensure they hold an active ISO 9001:2015 Quality Management System certification covering both design and manufacturing phases. For European export markets, equipment must carry CE certification covering the Low Voltage Directive (LVD 2014/35/EU) and Electromagnetic Compatibility (EMC Directive 2014/30/EU). For North American markets, compliance with CSA or UL standards for industrial electrical safety is highly recommended.
Standard consumable packages (nozzles, electrodes, shield caps, swirl rings) are typically stocked in volume and ship within 3 to 7 working days via DHL/FedEx/UPS express air freight. Complete mechanized torch assemblies and inverter power source machines carry a 15 to 25 calendar day production lead time. Export goods are vacuum-sealed in anti-corrosion VCI moisture-barrier bags and packaged inside IPPC-certified ISPM-15 compliant fumigation-free plywood crates for safe ocean or air transportation.
Overseas distributors can submit 3D CAD files (STEP/IGES format) or physical samples to the factory's engineering team. The OEM team will perform fluid dynamic modeling, produce rapid-prototype 3D printed handle/body shells, and execute trial arc-striking tests. Private label laser marking on torch bodies and custom color-coded retail packaging are routinely provided for contract orders meeting minimum order quantities (MOQ).
Get in touch with our senior application engineers to discuss your thermal cutting specifications, request OEM/ODM technical catalogs, or obtain competitive factory-direct export quotations.
Contact Us