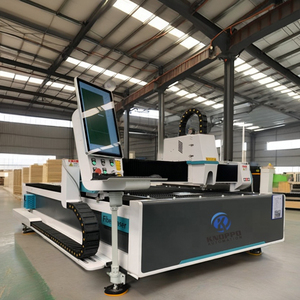
High-performance power sources, laser cutters, pressure vessel winders, and consumables engineered for rigorous industrial manufacturing.
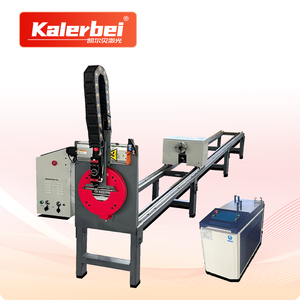
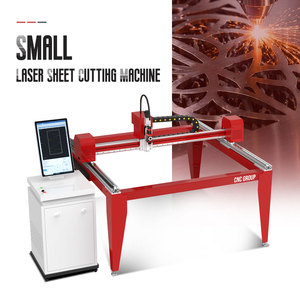
Equipped with narrow-band blue/red laser triangulation and dual-channel optical filters to completely eliminate intense arc glare and spatter reflections during MIG, TIG, and SAW operations.
Native EtherCAT, PROFINET, and Modbus-TCP protocol support, offering plug-and-play real-time path correction for FANUC, KUKA, ABB, Yaskawa, and custom CNC gantries.
AI-driven image processing algorithms automatically detect V-groove, lap joints, fillet welds, and narrow gap configurations without manual teach-pendant programming.
In modern heavy industrial manufacturing—spanning pressure vessel production, shipbuilding, wind tower construction, automotive chassis assembly, and cross-country pipeline engineering—achieving zero-defect weld seams is no longer optional. Traditional fixed-path automated welding systems relying purely on programmed trajectories frequently fail due to workpiece thermal distortion, joint gap variations, sheet metal spring-back, and assembly fitting tolerances. As China's leading welding seam tracker manufacturer and global engineering exporter, Advanced Power Sources Limited (APS) provides a comprehensive technical overview of laser vision seam tracking technologies, strategic procurement frameworks, and industry trends shaping automated welding through 2030.
At the core of an advanced laser seam tracking system lies the principle of optical triangulation. A structured laser line (typically operating at 450nm blue or 650nm red wavelengths) is projected onto the workpiece surface across the weld seam groove. The reflected laser light passes through an optical lens assembly and is captured by a high-speed CMOS matrix sensor positioned at a precise offset angle.
The sensor's internal Digital Signal Processor (DSP) or Field Programmable Gate Array (FPGA) analyzes the geometric distortion of the laser line in real time. By computing spatial height changes ($Z$) and lateral displacement ($X$), the vision processing unit identifies the exact seam center, root gap width, groove cross-sectional area, and joint alignment. This data is transmitted at frequencies exceeding 100 Hz to the motion controller, driving servo actuators to realign the welding torch continuously ahead of the arc.
Selecting the optimal seam tracking architecture requires evaluating process constraints, joint geometry, material reflective properties, and thermal exposure. The comparison table below highlights key performance parameters across modern industrial tracking methods:
| Parameter / Feature | Laser Vision Tracking (LVS) | Arc Voltage Control (AVC / Thru-Arc) | Tactile Mechanical Probing | Inductive / Capacitive Probing |
|---|---|---|---|---|
| Primary Tracking Axis | 3D Real-Time ($X, Y, Z$ + Torch Angle) | 1D or 2D ($Z$-height / Weave Center) | 2D Mechanical ($X, Z$) | 1D Height Sensing ($Z$-axis only) |
| Tracking Accuracy | High Precision (±0.02 mm to ±0.05 mm) | Moderate (±0.5 mm to ±1.0 mm) | Low-Medium (±0.5 mm) | Medium (±0.2 mm) |
| Response Speed | Ultra-Fast (< 10 ms closed-loop) | Slow (Dependent on arc weave rate) | Physical friction lag | Moderate (50 ms) |
| Surface & Material Adaptability | Universal (Carbon steel, SS, Aluminum, Copper) | Ferrous materials with stable arcs | Rigid plates (Scratches thin sheet) | Conductive metals only |
| Arc Glare & Dust Resistance | High (Optical narrowband filtering + Air knife) | Unaffected by optical glare | Unaffected by light | Sensitive to magnetic slag |
| Groove Profiling Capability | Full 3D profile, gap width & volume calculation | No groove measurement capability | None | None |
Industrial welding environments represent some of the most hostile operating conditions for optical sensors. High-frequency electromagnetic interference (EMI), intense ultraviolet and infrared arc radiation, molten spatter ejection, ambient smoke, and severe thermal radiation pose major operational risks. China's top-tier seam tracker manufacturers utilize several proprietary engineering solutions to guarantee high reliability:
Procurement directors and plant managers in international engineering companies are shifting their capital expenditure criteria when sourcing welding automation from China. The decision-making process has evolved from simple hardware price comparisons to evaluating holistic lifecycle value, IoT integration capabilities, software ecosystem compatibility, and vendor application engineering expertise.
In thick-plate applications such as pressure vessel dish heads, offshore wind turbine monopiles, and heavy bridge girders, single-pass welding is impossible. Modern buyers require laser seam trackers capable of performing multi-pass adaptive filling. The vision system scans the root joint profile during the first pass, calculates the exact volume of the bevel, and automatically adjusts wire feed speed, travel speed, torch weave amplitude, and dwell times for subsequent fill and cap passes without human intervention.
Smart factories operating under Industry 4.0 frameworks demand full traceability. Advanced seam tracking controllers now integrate embedded OPC-UA, MQTT, and WeldVisor IoT telemetry modules. Quality management teams can monitor real-time spatial path deviation logs, thermal profiles, arc-on efficiency, and sensor optical health from centralized dashboards. If a thermal distortion exceeds engineering tolerance limits, automated alerts notify operators or trigger automated machine pauses before non-conforming welds are completed.
Rather than replacing multi-million dollar gantry welding beds or column-and-boom SAW manipulators, industrial fabricators are increasingly procuring modular seam tracker retrofit packages. These turnkey kits include compact 2-axis ($X-Z$) motorized cross-slides, a laser vision sensor head, a touchscreen industrial HMI, and universal mounting brackets. This retrofit strategy reduces capital outlay by over 60% while elevating legacy machines to modern precision standards within days.
As an ISO 9001:2015 certified manufacturer and exporter with over 21 years of deep industrial experience, Advanced Power Sources Limited (APS) operates a state-of-the-art production facility in Old GIDC Gundlav, Valsad, Gujarat, supplying high-performance welding power sources, seam trackers, cutting machines, and automated positioning systems worldwide.
Our engineering team collaborates directly with global EPC contractors, shipyard automation supervisors, and tank fabricators. We offer comprehensive application feasibility studies, joint drawing reviews, and custom software protocol development to ensure seamless integration with existing robotic arms and CNC gantries.
Our standard industrial laser vision seam trackers offer configurable standoff distances (working distances) ranging from 80 mm to 250 mm, with field-of-view (FOV) measurement widths between 10 mm and 120 mm. Custom long-standoff models are available for heavy submerged arc welding (SAW) where high heat radiation and bulky flux hoppers require greater sensor clearance.
Blue lasers (450nm wavelength) feature significantly lower light penetration and less specular scattering on reflective metal surfaces such as stainless steel, aluminum alloys, copper, and galvanized sheets compared to red lasers (650nm). Additionally, high-current welding arcs emit less ambient radiation in the blue spectrum, allowing our dual-filter optical sensors to maintain crisp, distortion-free groove profile images even during high-amperage MIG/TIG processes.
Yes. Our tracking controllers support native industrial Ethernet protocols including EtherCAT, PROFINET, Ethernet/IP, and Modbus-TCP, as well as digital/analog I/O interfaces. We provide pre-built software driver packages and communication control blocks for major robot OEMs (KUKA, ABB, FANUC, Yaskawa, Motoman, Kawada) as well as custom PLC-based CNC gantries.
Every sensor head is built inside an IP67-rated sealed aluminum enclosure equipped with a heavy-duty splash shield, a replaceable optical quartz glass window, an integrated pneumatic air knife (which blows high-velocity compressed air across the window to repel dust and spatter), and optional internal liquid-cooling chambers for high-temperature applications.
For high-throughput manufacturers operating automated tank production, pipe spool fabrication, or structural beam lines, the ROI payback period typically ranges from 4 to 8 months. Payback is driven by a 40–70% reduction in joint preparation/teaching time, virtual elimination of weld seam rework and grinding scrap, increased travel speeds, and continuous multi-shift arc-on utilization.
To ensure our application engineers recommend the correct sensor model, cross-slide travel strokes, and control interfaces, please specify: (1) Welding process (MIG/MAG, TIG, SAW, Plasma), (2) Workpiece material, joint types (V-bevel, butt, lap, fillet), and sheet thickness, (3) Required tracking speed range, (4) Host motion system (Robot brand, CNC gantry, or column & boom manipulator), and (5) Operating environment conditions (ambient temp, preheat requirement).
Consult with our senior application engineers to receive custom seam tracking system drawings, joint sample testing, and direct factory quotation packages.
Send an Inquiry