
[email protected] Sales: +91 96014 44111 Service: +91 96013 33888

CE Certified TIG Welding Torch Factories & Exporters

Engineering Whitepaper & Global Sourcing Manual for High-Duty GTAW Torches, Gouging Equipment, and Automated Industrial Arc Systems

Heavy-Duty Welding & Cutting Products

Explore our certified lineup of TIG welding torches, air carbon arc gouging guns, orbital welding heads, fiber laser cutters, and heavy industrial automation solutions.
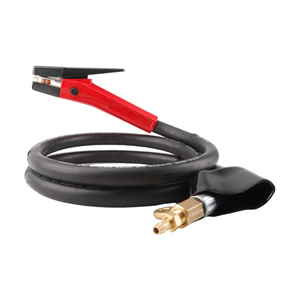
CNAWELD K4000 Air Carbon Arc Gouging Torch

CNAWELD K4000 Air Carbon Arc Gouging Torch

Heavy-duty carbon arc gouging gun designed for precise weld root cleaning, alloy defect removal, and bevel preparation up to 1000A capacity.
Contact Us
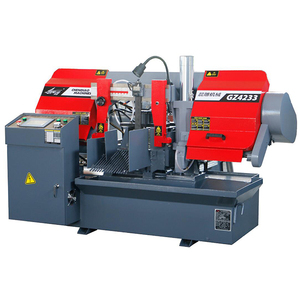
CNC Fully Automatic Metal Band Saw Blade Welding Machine

CNC Automatic Band Saw Blade Welding Machine

Precision horizontal resistance butt-welding unit for high-repeatability joining of bi-metal and carbide band saw blades.
Contact Us
PTA Plasma Transferred Arc Inverter Welding Machine

PTA Plasma Transferred Arc Inverter Cladding Machine

Advanced plasma transferred arc system engineered for wear-resistant hardfacing, PTA metal cladding, and precision surface alloy enhancement.
Contact Us
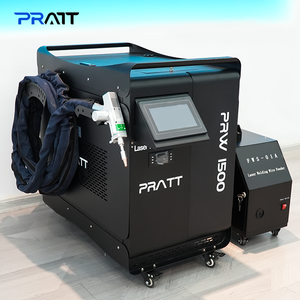
Fiber Laser Welding Machine For Metal

High-Power Industrial Fiber Laser Welding Machine

Factory-direct 1500W to 6000W fiber laser welding platform delivering deep penetration, minimal thermal distortion, and high-speed metal joinery.
Contact Us
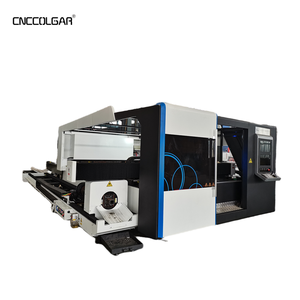
6KW Enclosed Fiber Laser Cutting Machine

6KW Full Enclosure Fiber Laser Cutting Machine

CNC automated fiber laser cutting station with dual exchange shuttle tables and integrated 6m pipe profile cutter module.
Contact Us
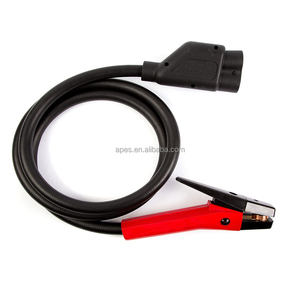
Arc Air Gouging Torch 600A 800A 1000A

Extreme Heavy Duty Arc Air Gouging Torch (600A-1000A)

K3/K4 series high-amp air carbon arc torch featuring 360-degree swiveling cable assemblies and ergonomic heavy-impact insulation.
Contact Us
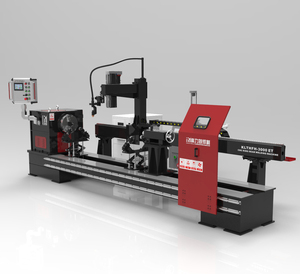
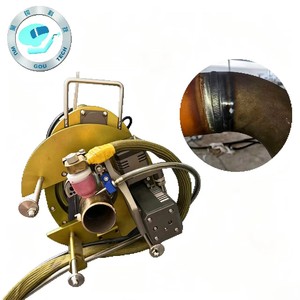
Wugou Automatic Pipe Orbital TIG Welding Machine

Automatic Orbital TIG Pipe Welding Equipment

Precision circular seam orbital GTAW system designed for pipeline fabrication, sanitary stainless tube joining, and hardfacing repair.
Contact Us
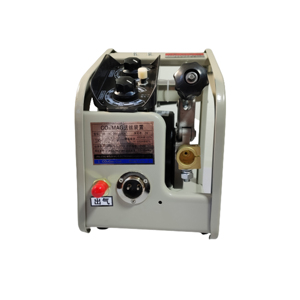
TIG Welding Wire Feeder Wire Liner Argon Arc Welding

Cold Wire Feeder System for Automatic TIG Welding

Microprocessor-controlled pulse cold wire feeder with Teflon/steel wire liners for high-consistency automated TIG wire delivery.
Contact Us
22,600+
Global Systems Installed
ISO 9001
Quality System Certified
CE & IEC
Full European Compliance
20+ Years
In-House Manufacturing

Engineering Excellence in CE Certified TIG Welding Torch Manufacturing

Understanding thermal conductivity, shielding gas dynamics, and high-frequency arc stabilization for critical industrial joinery.

Advanced Gas Lens Dynamics

Standard GTAW nozzles often suffer from turbulent shielding gas dispersion, leading to atmospheric oxygen contamination and weld porosity. Premium CE-certified TIG torches incorporate multi-layered stainless steel mesh gas lenses. This creates a smooth, laminar gas flow column, allowing tungsten stick-out lengths up to 1 inch while providing superior protection over titanium, Inconel, and stainless steel joints.

Thermal Dissipation & Duty Cycle

Under EN 60974-7 standard testing protocols, duty cycles are rigorously evaluated over a 10-minute period at 40°C ambient room temperature. Water-cooled TIG torches utilize dual-pass internal copper cooling channels directly surrounding the tungsten collet body. This enables continuous 100% duty cycle operation at 350A to 500A currents without handle thermal degradation or high-frequency dielectric breakdown.

Ergonomics & Cable Flexibility

Repetitive Strain Injury (RSI) is a major contributor to operator fatigue in high-volume boiler and aerospace production lines. Factory-engineered CE torches feature high-flex silicon rubber power cables wrapped in cut-resistant zippered leather covers. Integrated ball-and-socket handle joints reduce wrist tension, empowering welders to execute flawless root passes in tight quarters.

TIG Torch Class Comparison: Air-Cooled vs. Water-Cooled Systems

Selecting the optimal torch geometry and cooling infrastructure based on material thickness, current density, and production environment.
Performance Metrics Air-Cooled (WP-9 / WP-17 / WP-26) Water-Cooled (WP-18 / WP-20 / Heavy Automation) Orbital TIG Heads (Pipelining / Tube Sheets)
Current Handling Range 125A – 250A DC / 160A AC 250A – 500A+ DC Continuous 150A – 400A Pulsed Current
Duty Cycle Rating (IEC 60974-7) 60% at rated current (air conductive) 100% continuous duty cycle 100% continuous automated duty
Cooling Medium Ambient air flow & shielding gas flow Closed-loop water recirculation cooler Integrated liquid cooling jacket
Primary Industrial Applications Light sheet metal, structural steel repair, field maintenance Heavy plate fabrication, pressure vessel seams, nuclear equipment Sanitary stainless tubing, aerospace ducts, tube-to-tubesheet
Cable Weight & Flexibility Ultra-lightweight, single mono-cable design Tri-cable assembly (Gas, Water In, Power/Water Out) Bundled robotic umbilical with feedback sensors
CE Compliance Standard EN 60974-7 / Low Voltage Directive 2014/35/EU EN 60974-7 / RoHS / IP3X Enclosure Rating EN 60974-7 / EN 60974-10 EMC Class A

Key Procurement & Automation Trends Shaping 2025–2030

Strategic insights for OEM buyers, engineering procurement managers, and international welding equipment distributors.

1. Integration of Smart IoT Data Sensors in Torch Handles

Modern manufacturing plants are transitioning to Industry 4.0 standards. Advanced TIG torches now integrate real-time sensor modules within the handle housing to track arc-on time, gas flow rate, and handle temperature. Connecting these metrics to central monitoring systems (such as the WeldVisor IoT platform) allows plant managers to optimize gas consumption, audit operator efficiency, and schedule predictive maintenance before dielectric breakdown occurs.

2. Transition to Modular Swappable Torch Neck Architectures

Factory downtime caused by damaged torch necks or restricted angle access is a significant cost driver in complex weldments. Flexible (FL) and quick-change modular torch heads allow welders to swap from a straight 180° head to a 90° or 70° angle neck in under 30 seconds. Importers and procurement heads are increasingly specifying modular torch systems to consolidate inventory spare parts while maximizing shop-floor adaptability.

3. High-Frequency (HF) Interference Mitigation & Digital Shielding

With digital inverter power sources and robotic CNC controllers sharing the shop floor space, high-frequency arc-starting noise can disrupt sensitive microcontrollers and PLC communication lines. Modern CE-certified TIG torches incorporate enhanced coaxial shielding and digital logic signal wiring to isolate HF pulse ignition, guaranteeing flawless arc starting without tripping neighboring automated machinery.

4. Environmental RoHS & Non-Thoriated Electrode Compliance

Environmental regulations in the European Union and North America are pushing industrial fabricators away from low-level radioactive Thoriated Tungsten (EWTh-2) electrodes. Export-oriented torch factories now optimize collet body gas dynamics specifically for Lanthanated (EWLa-1.5/2.0), Ceriated (EWCe-2), and rare-earth E3 tungsten electrodes. This delivers equal arc stability and ignition characteristics without health or environmental compliance liabilities.

Factory Direct Manufacturing & Engineering Capabilities

Building over two decades of precision welding power source, torch, and automation manufacturing excellence.

In-House R&D & Inverter Design

Unlike trading companies, every machine circuit board, torch handle mold, and control firmware is developed in-house at our dedicated manufacturing facility in Gujarat, India. This guarantees direct technical support and immediate resolution of complex field application challenges.

ISO 9001:2015 & CE Quality Standards

Our rigorous Quality Assurance system controls every stage of production—from incoming raw copper purity checks and high-voltage dielectric isolation testing to 100% full-load thermal chamber testing prior to global export shipping.

Global OEM/ODM Export Solutions

With over 22,600 machines deployed across international markets, we support global distributors and heavy industrial clients with customized branding, tailored cable lengths, specialized plug configurations, and full technical documentation.

Frequently Asked Sourcing & Technical Questions

Direct expert answers to essential technical queries regarding TIG torches, air carbon arc gouging, and international procurement standards.
1. What certifications are required for exporting TIG welding torches to European markets?
To export TIG welding torches to European Union member states, equipment must comply with the Low Voltage Directive (LVD) 2014/35/EU and be manufactured in compliance with harmonized standard EN 60974-7 (Arc welding equipment - Part 7: Torches). This certification verifies electrical safety, insulation resistance, thermal rating compliance, and IP protection levels. All our export torches carry verified CE marks and come with official compliance declarations.
2. How do I determine whether my shop needs an air-cooled or water-cooled TIG torch?
The decision depends on three primary variables: operating current (amperage), duty cycle requirement, and joint thickness. If your shop routinely welds stainless steel or aluminum at currents exceeding 200 Amps for extended durations, a water-cooled TIG torch (such as a WP-18 or WP-20 series) is mandatory to prevent torch handle overheating and gas lens degradation. For field installation, light sheet fabrication, or repair work under 180A, air-cooled torches offer greater portability without needing a water recirculating cooler.
3. What is the operational difference between TIG welding torches and Air Carbon Arc Gouging torches?
While TIG (GTAW) torches use a non-consumable tungsten electrode under an inert argon gas shield to produce clean, high-precision welds, an Air Carbon Arc Gouging torch (like the K4000 series) uses a consumable carbon/graphite rod combined with compressed air blasts (80-100 PSI). The gouging torch melts metal via a heavy current arc (up to 1000A) and instantly blows away molten slag. It is specifically used for weld root cleaning, back-gouging heavy plates, and removing defective weld seams prior to re-welding.
4. How does gas lens technology improve TIG weld quality on stainless steel and reactive metals?
A standard TIG collet body releases argon gas in a swirling, turbulent vortex that mixes with surrounding room air at greater distances. A gas lens replaces the standard collet body with a specialized housing containing multiple microscopic stainless steel screen mesh layers. This transforms the turbulent gas into a smooth, laminar flow column. Laminar flow eliminates air entrapment, reduces tungsten oxidation, and allows the welder to extend the tungsten electrode up to 25mm out of the nozzle for enhanced visibility in tight fillet welds and root joints.
5. What spare parts should be included in a wholesale TIG torch procurement order?
For smooth production line operations, overseas buyers should always stock a balanced ratio of high-wear consumables. Essential spares include: Collets and Collet Bodies (sized for 1.6mm, 2.4mm, and 3.2mm electrodes), Alumina Ceramic Cups (#5, #6, #7, and #8 orifice sizes), Gas Lens Assemblies, Long/Medium/Short Back Caps with high-temperature O-rings, and replacement silicone rubber handle shells.
6. Can your TIG torches and cold wire feeders be integrated with robotic arms and orbital tractors?
Yes. We supply specialized automatic machine TIG torches equipped with rigid cylindrical barrels, rack-and-pinion positioning mounts, and heavy-duty signal connectors. When paired with our automatic TIG cold wire feeder system, these torches integrate seamlessly with orbital pipe welding carriages, column-and-boom manipulators, and multi-axis CNC/robotic welding cells.

Request Factory Direct Quotations & Engineering Support

Need customized cable lengths, specialized torch head configurations, or bulk distributor pricing? Connect directly with our application engineering team today.