CE and ISO 9001:2015 compliant industrial machinery tailored for heavy structural engineering, pipe profiling, and high-deposition welding lines.
From component-level IGBT inverter power source design to heavy structural steel beam profiling, we control the total manufacturing lifecycle to guarantee compliance with European Machinery and Pressure Equipment Directives.
Our complete structural and machinery manufacturing process operates under strict ISO 9001:2015 quality management systems. Every heavy plate assembly undergoes certified non-destructive testing (NDT), including Ultrasonic (UT), Magnetic Particle (MT), and Radiographic (RT) inspections in compliance with EN 1090-2 (Execution Class EXC3/EXC4) and ASME Section VIII standards.
Unlike asset-light traders, our internal engineering team develops proprietary IGBT inverter topologies, high-frequency control electronics, and automated CNC drive firmware. This allows tailored arc dynamic customization, reduced thermal stress during 100% duty cycle heavy plate welding, and seamless integration with industrial IoT monitoring software.
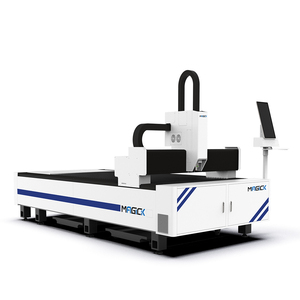
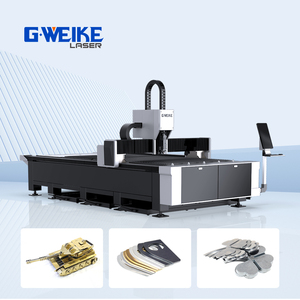
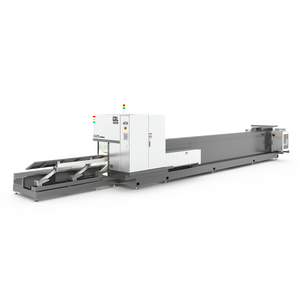
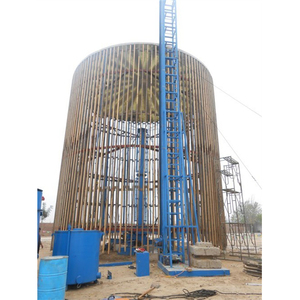
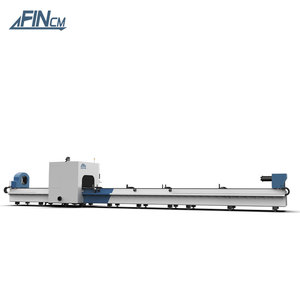
We supply unified engineering packages combining high-power fiber laser gantry systems, 45° beveling pipe cutters, self-aligning welding rotators, and heavy-duty Submerged Arc Welding (SAW) column & booms. One unified vendor guarantees zero signal latency between positioner controllers and digital power sources.
Heavy plate fabrication—encompassing thick carbon steel (S275, S355, S690QL), stainless steel (316L, Duplex 2205), and abrasion-resistant alloys (Hardox)—requires specialized thermal management, edge preparation, and structural weld integrity. Under European standard EN 1090-2 and the Machinery Directive 2006/42/EC, certified manufacturers must ensure full material traceability (EN 10204 3.1/3.2 MTC) and validated Welding Procedure Specifications (WPS/WPQR according to ISO 15614-1).
Request Technical Specification SheetComparative parameter guide for heavy structural steelwork, pressure vessels, and thick-walled tube beveling.
| Material Grade | Thickness Range | Primary Cutting Process | Edge Preparation / Bevel | Optimal Welding Process | Key Compliance Standard |
|---|---|---|---|---|---|
| S355JR / S355J2 Structural Steel | 10 mm – 120 mm | Fiber Laser (High Power 12kW-30kW) / Plasma Gantry | 45° CNC V/K/X-Bevel (3D Head) | Submerged Arc Welding (SAW) / FCAW | EN 1090-2 EXC3, CE Marked |
| S690QL High-Yield Quenched Steel | 12 mm – 80 mm | High-Precision Fiber Laser with Nitrogen/O2 Assist | Precision Mechanical Milling / Laser Beveling | Low-Hydrogen GMAW / Multi-Pass SAW | ISO 3834-2, EN 1090-2 EXC4 |
| Austenitic & Duplex Stainless (316L / 2205) | 6 mm – 60 mm | High-Power Fiber Laser (N2 Shielding) | 45° Clean Cold Beveling | Pulse GTAW Root + SAW Tandem Fill | ASME VIII Div 1 & 2, PED 2014/68/EU |
| Hardox 450 / 500 Wear-Resistant Plate | 8 mm – 50 mm | Ultra-High Power Fiber Laser Cut | Controlled Heat Input Beveling | Low-Heat Input GMAW (Strenx/Hardox Spec) | ISO 9001:2015 Internal QC |
How ultra-high power fiber lasers, AI-driven digital control, and hybrid process automation are redefining industrial steel component manufacturing.
The global shift toward 12kW–30kW fiber laser sources allows fabricators to cleanly slice through carbon steel up to 50mm and stainless steel up to 80mm with minimal heat-affected zones (HAZ). Fiber laser processing eliminates secondary grinding, dramatically reducing cycle times compared to legacy oxy-fuel profile cutting.
Modern structural steel production demands direct 45-degree weld preparation during the primary cutting pass. Automated 5-axis 3D laser heads execute complex tube saddle cuts, pipe profile intersections, and heavy plate edge bevels without manual layout or robotic secondary beveling stations.
Industrial IoT platforms, such as WeldVisor telemetry systems, log real-time voltage, wire feed rate, arc-on time, and heat input per seam. This digital traceability is vital for EPC contractors verifying compliance with strict European EN ISO 5817 weld quality level B specifications.
Key strategic considerations for EPC contractors, vessel fabricators, and structural steel buyers managing global supply chains.
Global buyers are moving away from sourcing cutting tables, positioners, and power sources from separate vendors. Single-source supply guarantees hardware-software synchronicity and simplifies international warranty claims.
With rising energy tariffs globally, switching from traditional transformer power sources to high-frequency IGBT inverter units slashes plant power consumption by up to 35%, supporting corporate Scope 2 carbon reduction goals.
Procurement specifications now frequently mandate direct compatibility with TEKLA, Autodesk Inventor, and DXF/DWG formats. Modern CNC systems allow instant nesting and automated toolpath generation directly from structural BIM models.
Overseas buyers require pre-shipment Inspection Certificates (SGS, TÜV, Bureau Veritas) demonstrating strict compliance with the Machinery Directive 2006/42/EC and Electromagnetic Compatibility (EMC) Directive 2014/30/EU.
Answers to common technical, certification, and shipping inquiries regarding heavy plate fabrication machinery and custom exported structures.
CE certification confirms that heavy plate fabrication equipment and structural components meet essential health, safety, and environmental protection requirements established by European Directives—specifically the Machinery Directive (2006/42/EC), Low Voltage Directive (2014/35/EU), and EMC Directive (2014/30/EU). For structural fabrications exported to Europe, EN 1090-2 CE marking proves full structural stability, material traceability, and audited welding quality assurance.
High-power CNC fiber laser cutting systems (up to 30kW) routinely handle carbon steel up to 50mm and stainless steel up to 80mm with smooth edge squareness. For heavy joint welding, Submerged Arc Welding (SAW) is the industry standard for plate thicknesses ranging from 12mm to well over 100mm, delivering extremely high deposition rates (over 15 kg/hr per arc wire) with deep weld root penetration.
We strictly adhere to ISO 13920 (Welded structures — General tolerances for linear and angular dimensions) and ISO 2768-m standards. Dimensional consistency is maintained by utilizing CNC 5-axis pipe profile cutters, automated welding positioners to eliminate distortion, and pre-heat / stress-relieving heat treatments where required by design codes.
Every heavy plate component or pressure vessel export package includes EN 10204 3.1 or 3.2 Material Test Certificates, Ultrasonic Testing (UT) reports for full-penetration butt welds, Magnetic Particle Inspection (MPI) reports for fillet joints, and dimensional inspection protocols stamped by certified ASNT Level II / III inspectors.
Yes. All of our industrial 3-axis and 5-axis CNC laser cutters natively support DXF, DWG, PLT, STEP, and IGES file formats. They interface smoothly with industry-standard nesting software (such as CypCut, SigmaNEST, or Radan), enabling automated structural steel layout, micro-joint placement, and remnant plate management.
Standard CNC machinery or welding automation units ship within 30 to 45 days upon technical drawing sign-off. Custom heavy structural lines or pressure equipment take 60 to 90 days. All export units are wrapped in anti-corrosion VCI barrier bags, mounted on heavy structural steel skids, and secured inside Open-Top or Flat-Rack sea containers for safe ocean transport.
We offer comprehensive global technical support via remote digital diagnostic gateways, online software assistance, and on-site engineering dispatch. Essential mechanical consumables, optical lenses, laser nozzles, and IGBT inverter board kits are stocked for fast international air dispatch within 48 hours.
Whether you require high-power CNC fiber laser cutting systems, automatic beveling pipe cutters, heavy SAW welding automation, or custom CE-marked structural fabrications, our application engineering team is ready to evaluate your CAD models and production goals.